A preflight should answer three different questions: does the file represent the intended geometry, does the selected printer and process have a plausible path to make it, and does the slice contain the features you expect? A successful import, a green repair warning, or a generated G-code file answers none of those questions by itself. Preserve the original model or project and record every transformation that changes what will be sliced.
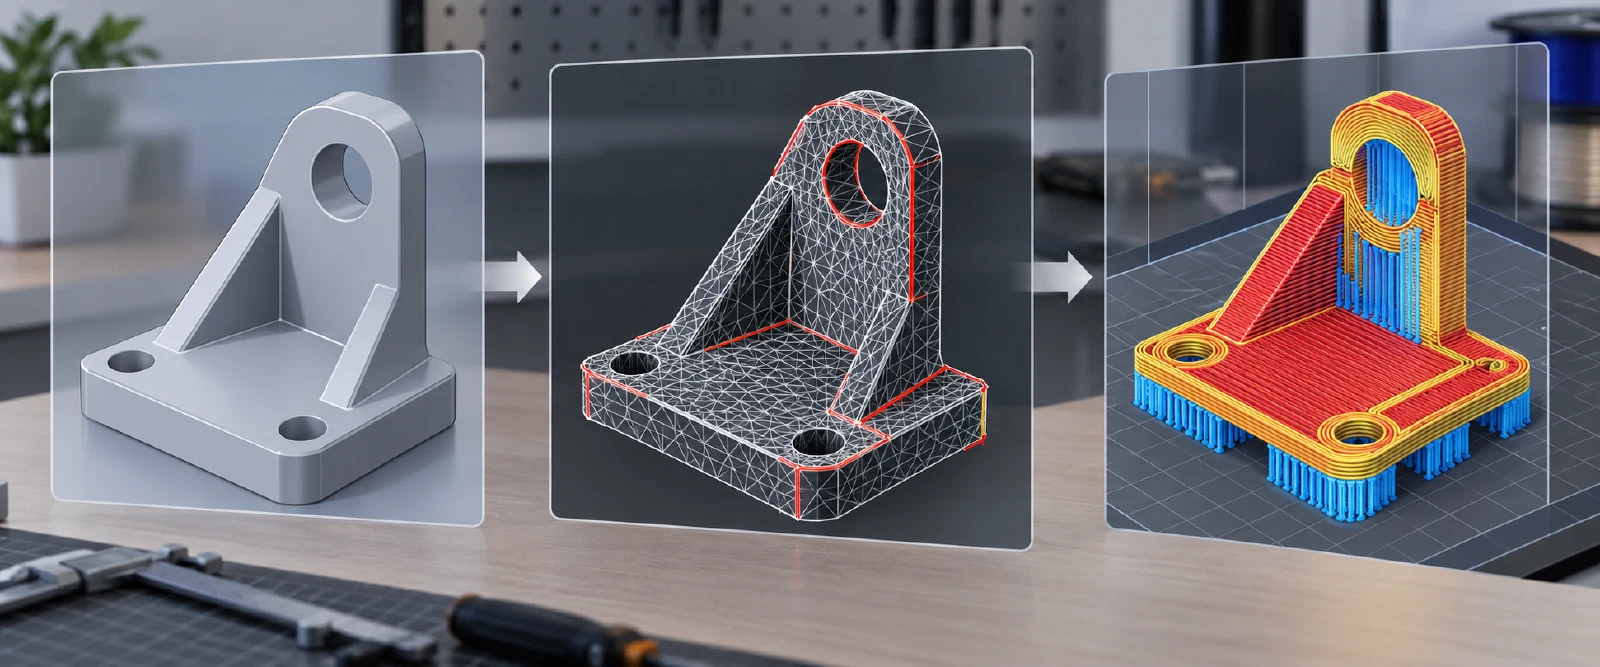
For OrcaSlicer’s belt workflow, add a separate check for the belt feature gate, coordinate transforms, and raw-G-code preview. The ordinary model view and the machine-coordinate output are different views of the job; see belt-printer model preparation and preflight .
1. Preserve identity and process context
Before editing, record the model revision or project file, source application, configuration or body/part identity, export format, units, axis convention, scale, and the receiving slicer and release. For a 3MF handoff, remember that core geometry, transforms, units, and coordinate systems are separate from extension features; compatibility is feature-specific and vendor-reported. For STL, explicitly check scale, scene units, forward/up axes, modifiers, and mesh validation after import.
Bind the model to the exact printer variant, firmware context, nozzle diameter and material, plate, slicer printer/material/process presets, and layer-height and line-width choices. Check the object tree or scene identity after import. An object, part, instance, or mesh group may have different settings and placement semantics, so select the intended scope before changing a modifier, support assignment, or process override.
For a project with multiple beds or open project contexts, record which model, printer, and configuration belong to each bed before slicing. These workflows are version-specific; verify the active project and each bed’s resolved settings in the target build rather than assuming an import preserved them.
2. Check geometry before asking the slicer to fix it
Run a mesh check for watertight or closed geometry, non-manifold edges, holes, intersections, distorted faces, very thin faces, and sharp or overhanging regions. A model intended for printing should represent a solid that can exist as a three-dimensional object. A slicer can repair some corruption, but not all of it; a repair operation may add or remove faces, change resolution, or behave platform- and version-specifically. Simplification is a different operation: it can reduce polygon and toolpath burden while losing visible detail.
Use this escalation sequence:
- Keep an untouched source and note the warning or failing check.
- Try the documented, setup-appropriate repair only when its scope is known.
- Compare dimensions, holes, thin features, normals, boundaries, and critical surfaces with the source.
- If the repair changes design intent or remains incomplete, return to the CAD or mesh source rather than stacking unrecorded automatic edits.
- Reopen the repaired model in the target slicer and inspect the new preview.
A repair warning is a reason to investigate, not proof that a model is unusable. A successful automatic repair is also not proof that the result matches the source or will print. Automated model checks, AI repair suggestions, and post-slice risk flags are additional signals, not a statement that every defect was detected. Creality Print 7.2.0 AI Edition beta, for example, describes checks and risk suggestions without reporting detection sensitivity. Check the tool’s stated coverage, compare edits with the source, and inspect any generated support in the layer preview.
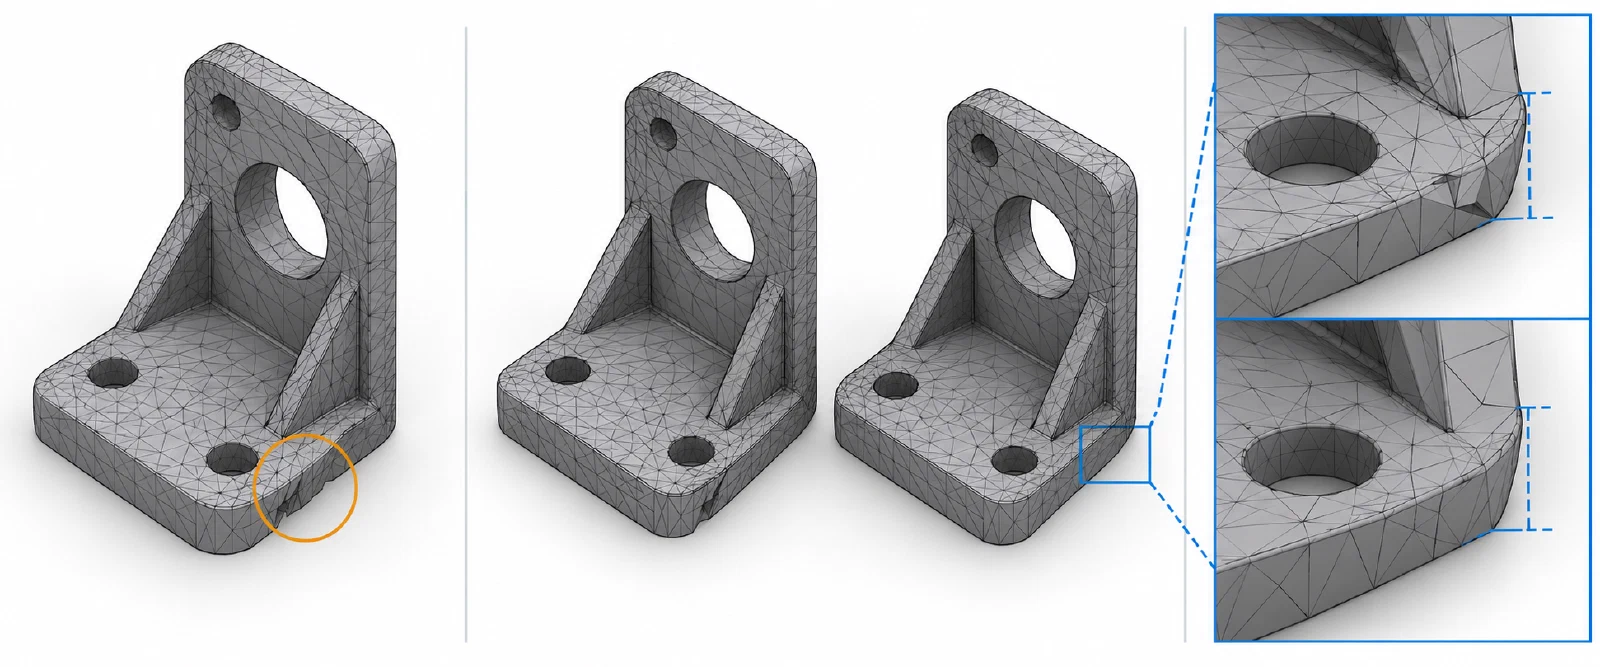
A generated assembly guide is a communication aid, not a fit check. Bambu Studio 2.8.0 Public Beta describes creating assembly steps from a STEP file; compare those steps and part identities with the source design, then verify the intended order and fit separately.
3. Check placement, machine envelope, and first layer
Confirm the model’s dimensions, orientation, bed shape, excluded regions, maximum height, Z offset, plate profile, and actual installed hardware. Auto Arrange can space and rotate objects, but it does not establish support access, purge-space, adhesion, tool-change, or physical stability. For by-object or sequential jobs, check the complete extruder envelope, including the profile’s radius and vertical clearances to rods or a lid. A warning-free export is not a collision guarantee.
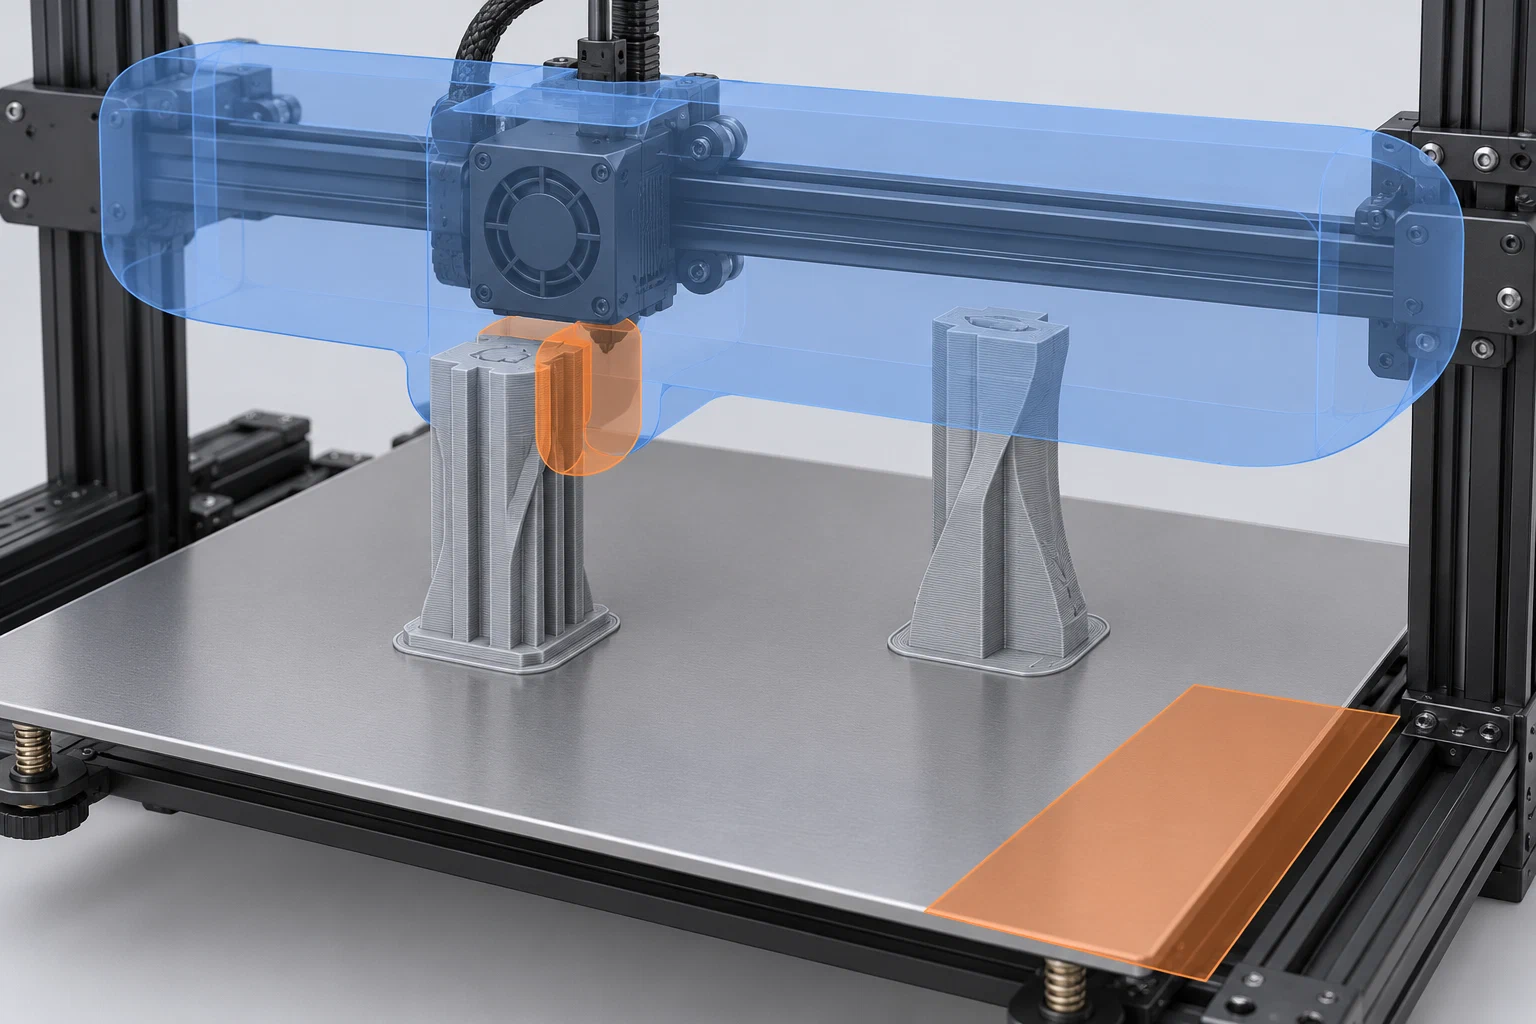
Inspect the first-layer footprint and choose a skirt, brim, or draft shield only for the problem it addresses. A skirt can reveal flow or adhesion problems; a brim increases contact area; a draft shield addresses a draft-sensitive process. Check that the aid fits the plate and can be removed. These are preparation aids, not universal adhesion or warping guarantees.
4. Audit the slice, not just the model
Use the layer-by-layer preview and check, in order:
- first-layer coverage, object placement, islands, holes, and missing geometry;
- perimeter count, thin-wall paths, gaps, bridges, overhangs, and infill;
- support origin, painted enforcers/blockers, interface layers, Z/XY separation, removal access, and support collisions;
- seam locations, modifiers, variable layer-height regions, negative volumes, and text or other generated geometry;
- material or extruder assignment, purge or wipe structures, travel, and multi-object order;
- estimated time and material against the intended trade-off and the actual printer profile; these values are estimates, not measured elapsed time.
If the model was edited, repaired, split, simplified, or reloaded, compare the preview before and after. If project files are exchanged, confirm which settings were preserved, replaced, or defaulted on import. A normal G-code file may carry toolpaths without the full printer, material, and process context; retain a project or separate handoff record when that context matters.
Distinguish a model-only 3MF, a full project, a selected-settings overlay, and a toolpath-bearing package. The 3MF Toolpath Extension document is marked Release Candidate and requires Core and Production extensions. If a package declares toolpath extensions, confirm that the exact producer and receiver support the required extensions and their versions; the specification or successful file open alone does not establish that the installed slicer and printer can use the toolpath.
5. Record the release decision
Keep a preflight record containing the source and modified file names, units and scale, mesh-check results, repair operation, selected object or part, printer and profile, nozzle, material and plate, support and first-layer choices, preview observations, estimated time/material, known unresolved risks, and the person or test that will verify the first layer. For a critical fit or load, add a measured coupon or representative validation print.
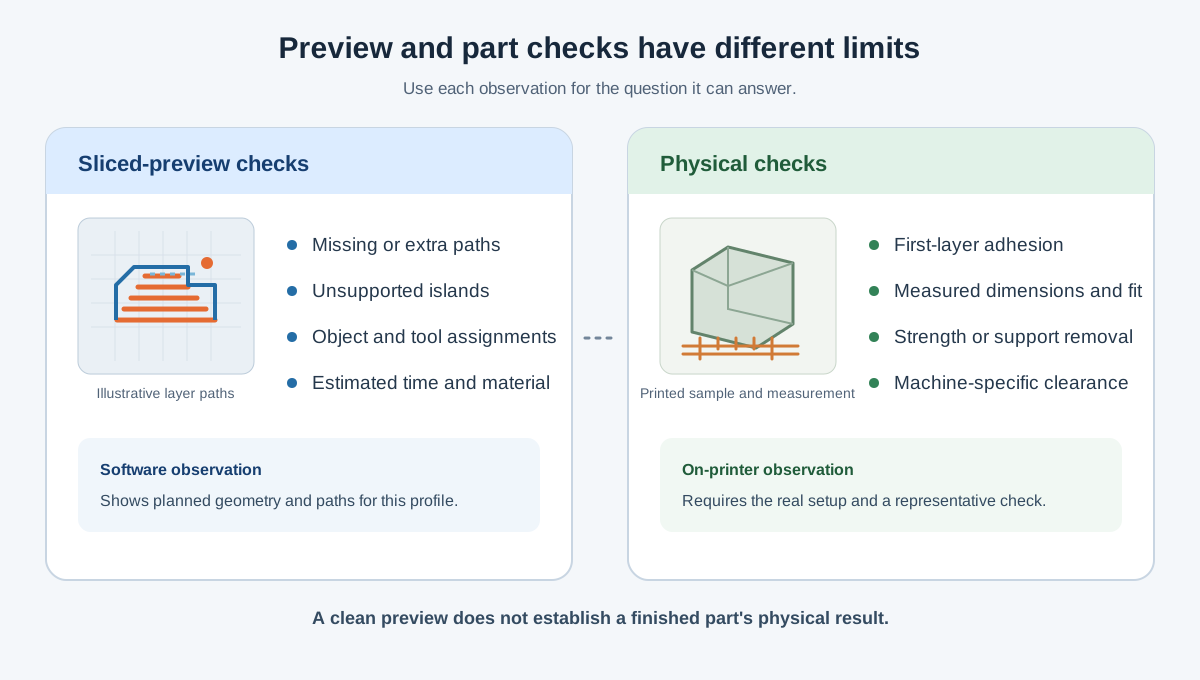
Do not treat a preview as physical validation. It can expose missing paths, unsupported islands, unexpected assignments, and many collision or fit risks, but it cannot prove adhesion, strength, support removal, dimensional accuracy, or machine safety. If an important check remains unknown, keep the job in a bounded test state or return to the source model instead of converting uncertainty into a confident export.
For orientation decisions, see choosing a 3D-print orientation for strength, surface, and reliability . For support and interface choices, use support strategy for overhangs and bridges . For critical dimensions, use thin walls, gaps, holes, and clearances .
Back to top ↑