This is a product-scoped starting point for Bambu TPU 95A HF on a Bambu Lab P1S. It is not a universal TPU profile and it is not a documented P1S print result. TPU hardness, formulation, moisture, feeder path, nozzle, plate, firmware, slicer release, and model geometry all matter.
Confirm the flexible-filament path
Bambu’s product page marks TPU 95A HF as incompatible with AMS and AMS lite. That statement belongs to this exact product. Bambu also sells a different TPU for AMS product, listed as Shore 68D with its own temperature and volumetric values; do not transfer those values or its feeder claim to TPU 95A HF, generic TPU, or another hardness.
Before loading the spool, record the P1S variant, firmware, Bambu Studio release, product and hardness, nozzle, plate, and the permitted feed path from the current printer and product instructions. Keep the path unobstructed and avoid excessive drive pressure. If the filament grinds, tangles, or cannot advance consistently, stop and correct the mechanical path before changing process values.
Product-scoped starting fields
| Field | Bambu TPU 95A HF starting point | Qualification |
|---|---|---|
| Nozzle | 220–240 °C product range; the captured P1S preset stores 230 °C | Product and preset values, not a P1S print result. |
| Bed | 30–35 °C with glue | Bambu TDS guidance; verify the installed plate and product instructions. |
| Maximum speed | Product guidance says below 200 mm/s | A ceiling or product instruction is not a quality target. Flexible parts usually need a slower, controlled test. |
| Maximum volumetric speed | The captured P1S preset stores 12 mm³/s | A preset field, not a measured P1S limit; inspect the resolved profile and preview. |
| Retraction | P1S preset: 0.8 mm; product TDS: 0.8–1.4 mm at 20–40 mm/s | Test with the actual path; excessive retraction can worsen feeding problems. |
| Flow | P1S preset stores flow ratio 1 | A stored default still needs product- and machine-specific verification. |
| Nozzle compatibility | Product TDS lists 0.4, 0.6, and 0.8 mm | Confirm the physical nozzle and selected machine/profile object. |
| Drying | Conflicting Bambu instructions: 55 °C for 8 hours in the Filament Guide and 70 °C for 8 hours in the TPU 95A HF TDS | The two source values are not reconciled; check current instructions for the exact spool and stay within spool and dryer limits. |
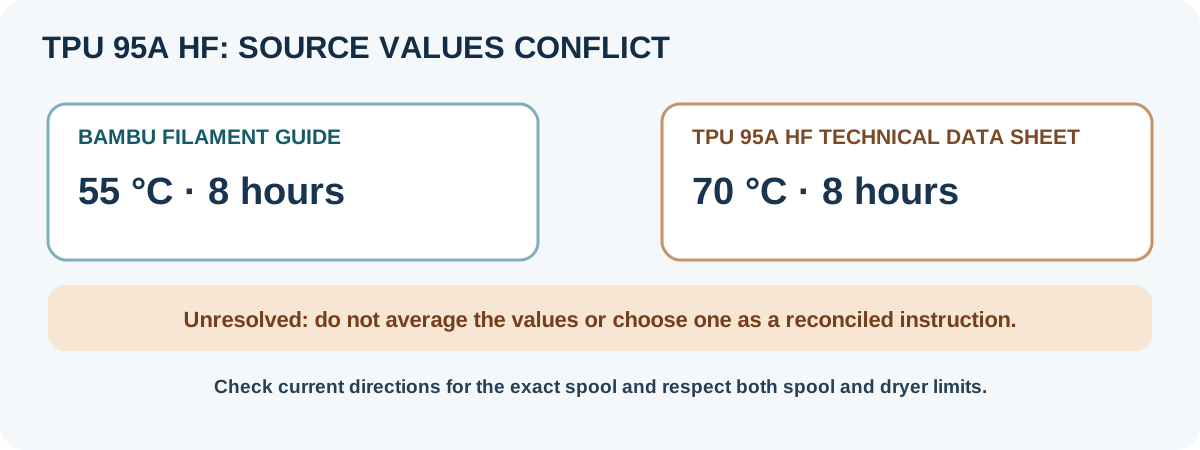
The Filament Guide and TPU 95A HF TDS give different blast-oven schedules for the same named product. Do not average the values or present either as a reconciled instruction. Check the current directions for the spool you have and confirm that both the spool and drying equipment are suitable for the applicable schedule. The TDS’s below-20% RH guidance describes sealed storage with desiccant; it does not settle which drying schedule applies.
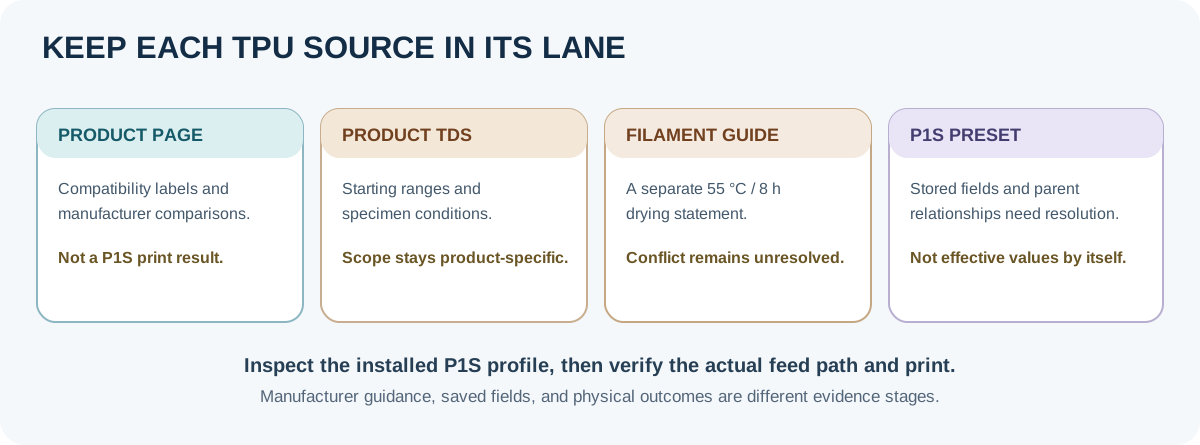
The TDS specimen conditions—230 °C nozzle, 35 °C bed, 140 mm/s, and 100% infill after drying and annealing—are standard sample conditions for comparison. They do not prove that the same result occurs on a P1S or on another model.
A short verification path
- Resolve the drying guidance for the exact product and equipment before starting a cycle. Confirm the spool and dryer limits, then record the schedule and date used; do not substitute a generic humidity threshold for a product instruction.
- Confirm the P1S machine profile, nozzle, plate, filament preset, and inherited values in the installed Bambu Studio release. The repository preset is on a mutable branch and does not resolve every inherited field.
- Run a short feeding test at a conservative process speed. Watch for grinding, tangling, skipped extrusion, and inconsistent flow. Stop if the path is damaging the filament.
- Print a small first-layer and flexible-feature test. Inspect adhesion, thin walls, corners, bridges, stringing, and recovery after travel moves before printing a large flexible part.
- Change one variable at a time. If stringing or under-extrusion remains, check moisture, nozzle condition, path friction, temperature, and retraction rather than assuming the preset is wrong.
Save the result with the product, hardness, dry state, path, nozzle, plate, slicer release, firmware, model, and observed outcome. A successful test for TPU 95A HF must not be presented as validation for another TPU product or for AMS use.
Back to top ↑