Thin lines, grinding, blobs, clicking, or stopped extrusion can come from a restricted feed path, but the symptom does not identify the cause by itself. A profile mismatch, spool drag, damp or damaged filament, a worn nozzle, cooling failure, drive-gear debris, or an installation problem can look similar. Capture the exact printer, nozzle, material, and recent changes before opening anything.
Triage the path before disassembly
Record the model and revision, firmware, nozzle diameter and material, filament product and dry state, plate, slicer and version, selected profile, layer height, speed, temperatures, cooling, and where the failure begins. Note whether the symptom appears on the first layer, after a long run, only with one spool, after abrasive or flexible filament, or immediately after a nozzle or hotend change.
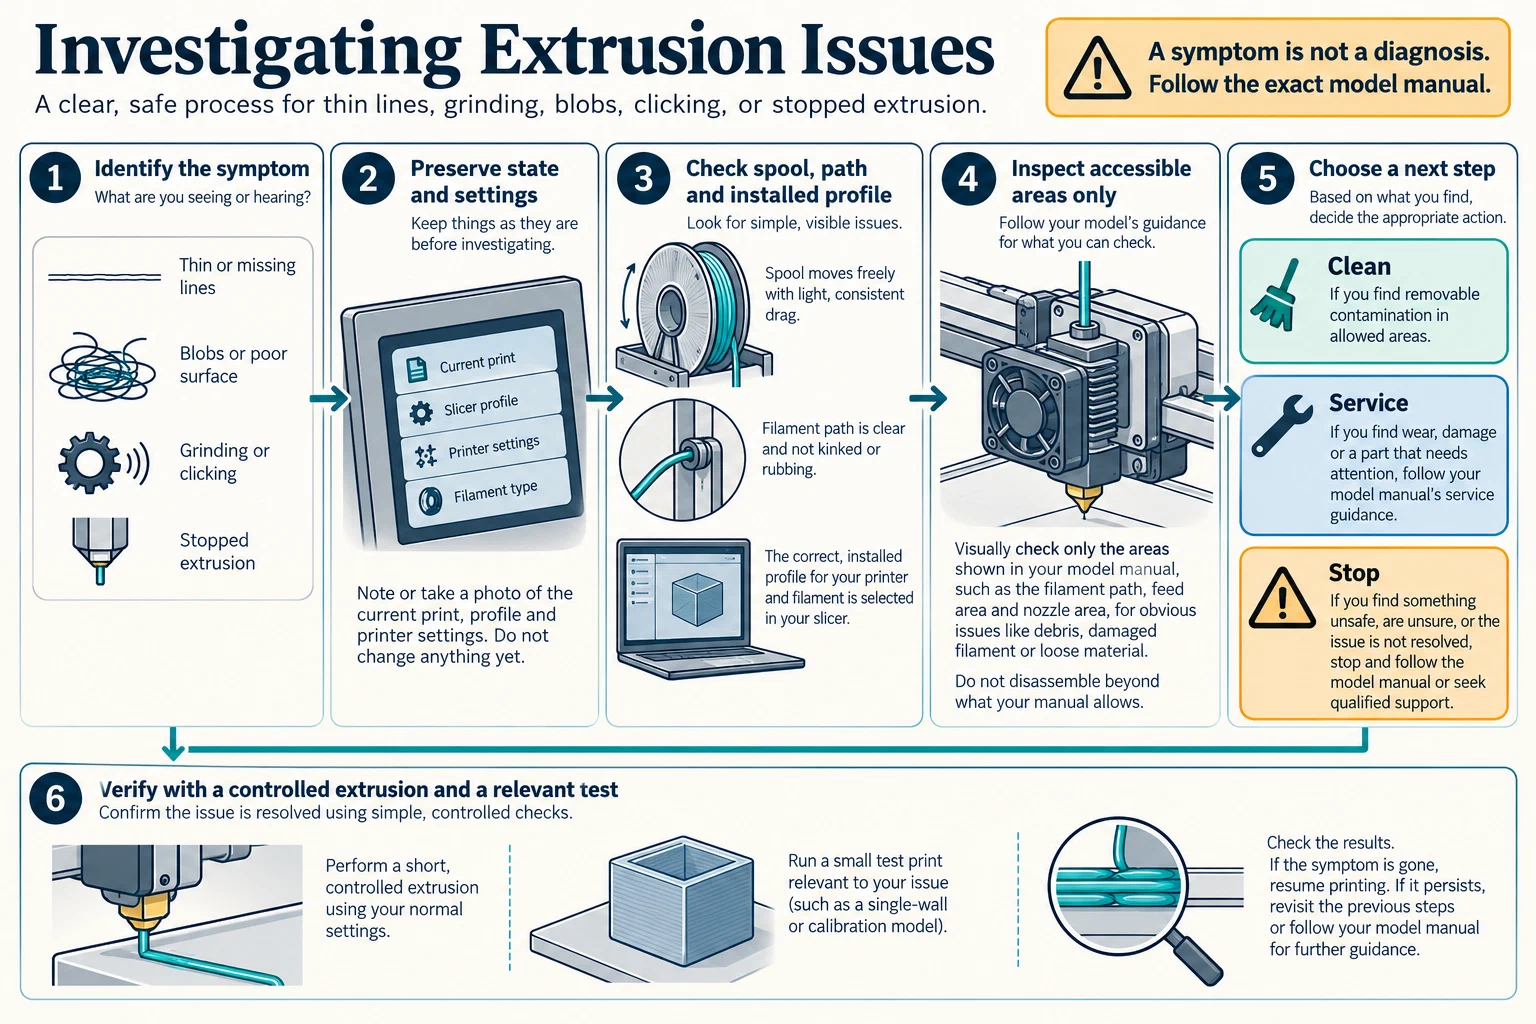
Use this low-risk sequence:
- Stop a print with failed extrusion and preserve the failed part and last known settings. Do not resume over missing material and call that recovery.
- Check that the spool turns freely and that the guide tube, PTFE path, filament sensor, and drive entrance are not kinked, pinched, contaminated, or rubbing. Inspect the filament for a ground section or unusual swelling.
- Confirm the selected material and nozzle profile match the installed hardware. Do not compensate for an unknown mismatch by raising temperature blindly.
- Inspect the nozzle exterior and the accessible extruder or feeder path using the exact model manual. A purge can show that material moves; it does not prove sustained flow during a print.
- If the symptom follows a long print, compare the hotend fan, heat-sink airflow, material throughput, and enclosure conditions with the model guidance before diagnosing heat creep.
The Ender-3 V3 SE support Wiki illustrates the correct boundary: it routes owners to separate model-specific tutorials for nozzle cleaning, extruder work, hotend replacement, belts, bearings, fans, and limit switches. Its captured support page does not provide a portable disassembly sequence, belt value, service interval, or print-quality acceptance threshold.
Apply the exact cleaning boundary
Manufacturer instructions take priority over a generic tool list. Prusa’s MK4/S and MK3.9/S maintenance guidance, for example, describes warming the nozzle for that printer family, protecting hotend cables, and waiting for ambient temperature before contact. It also describes cleaning accessible Nextruder gear debris while warning against opening the gearbox unless official support directs it. Do not copy that temperature, access order, or gearbox boundary to another printer.
For Prusa Nextruder nozzle families, the manufacturer distinguishes non-abrasive and abrasive filament use. Brass is described for non-abrasive materials, while abrasive composites can wear it quickly. For an ObXidian-coated nozzle, Prusa warns against an acupuncture needle, brass brush, and cold pull because the coating can be damaged. The source recommends a non-abrasive cloth for the exterior and cleaning filament for the internal path, but it does not establish one universal cleaning temperature or replacement interval.
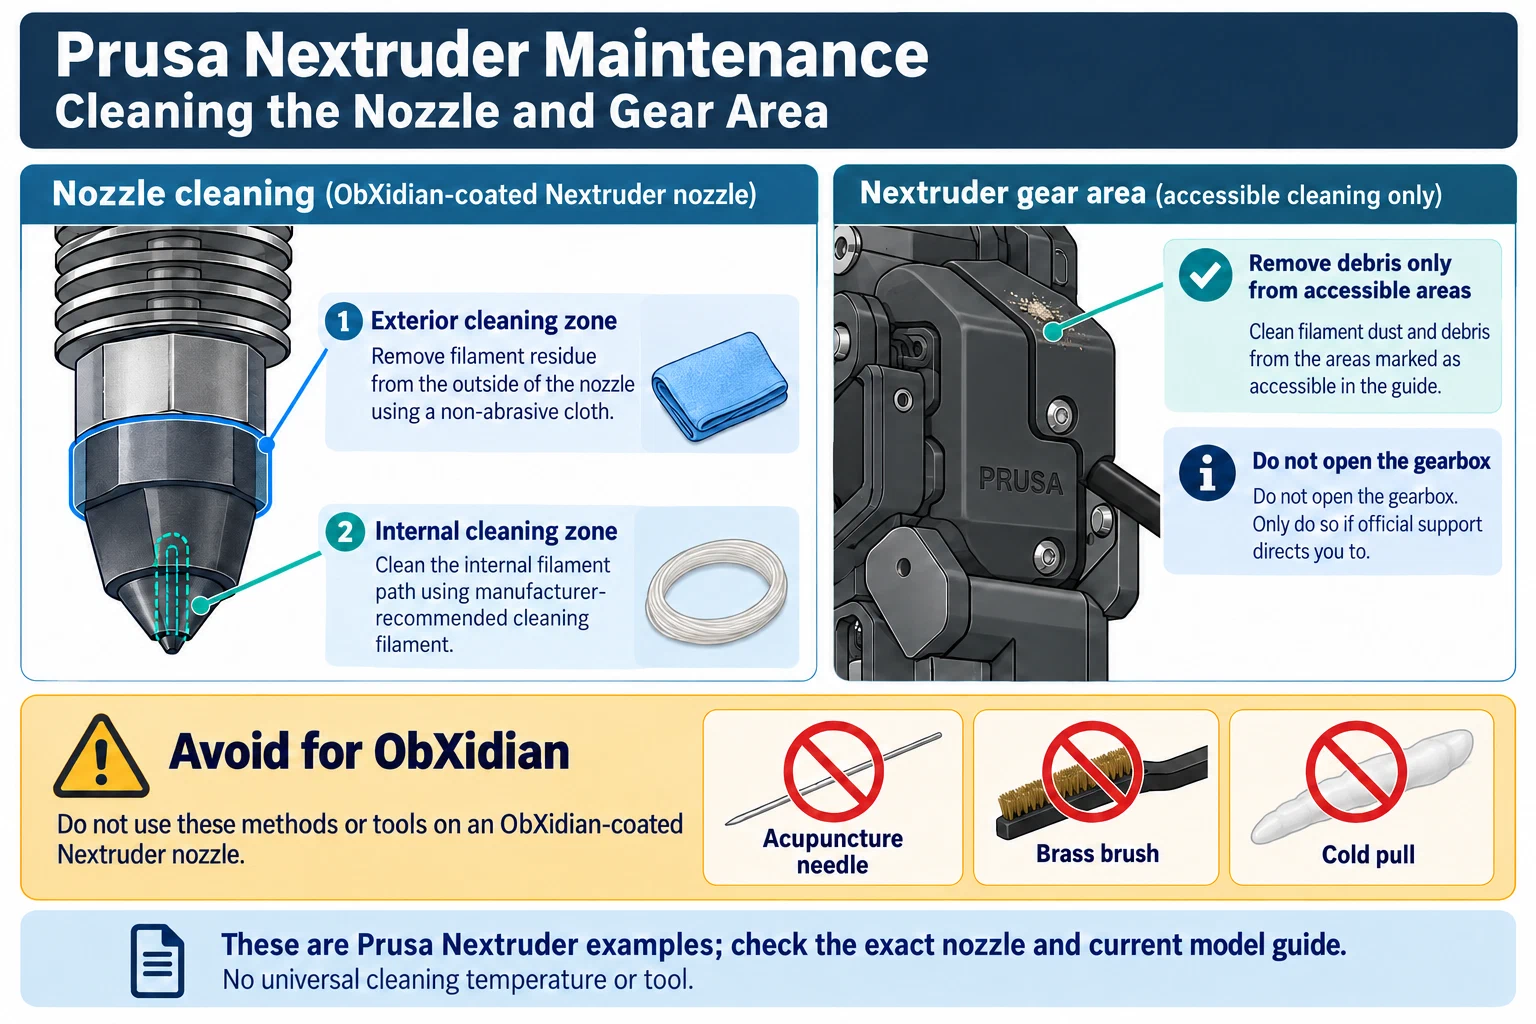
Treat hot surfaces, moving gears, stored energy, and electrical connections as part of the procedure. Use the source-defined cool-down, power-off, unplugging, guarding, and tool requirements. Stop and escalate when wiring is damaged, a fan or thermistor fault appears, the hotend cannot be identified safely, a coating or heater block is damaged, or the manual’s repair boundary is unclear. NIOSH’s workplace guidance supports recording the material, printer, task, and control context; it is not a printer service manual or universal exposure limit.
Prove what changed
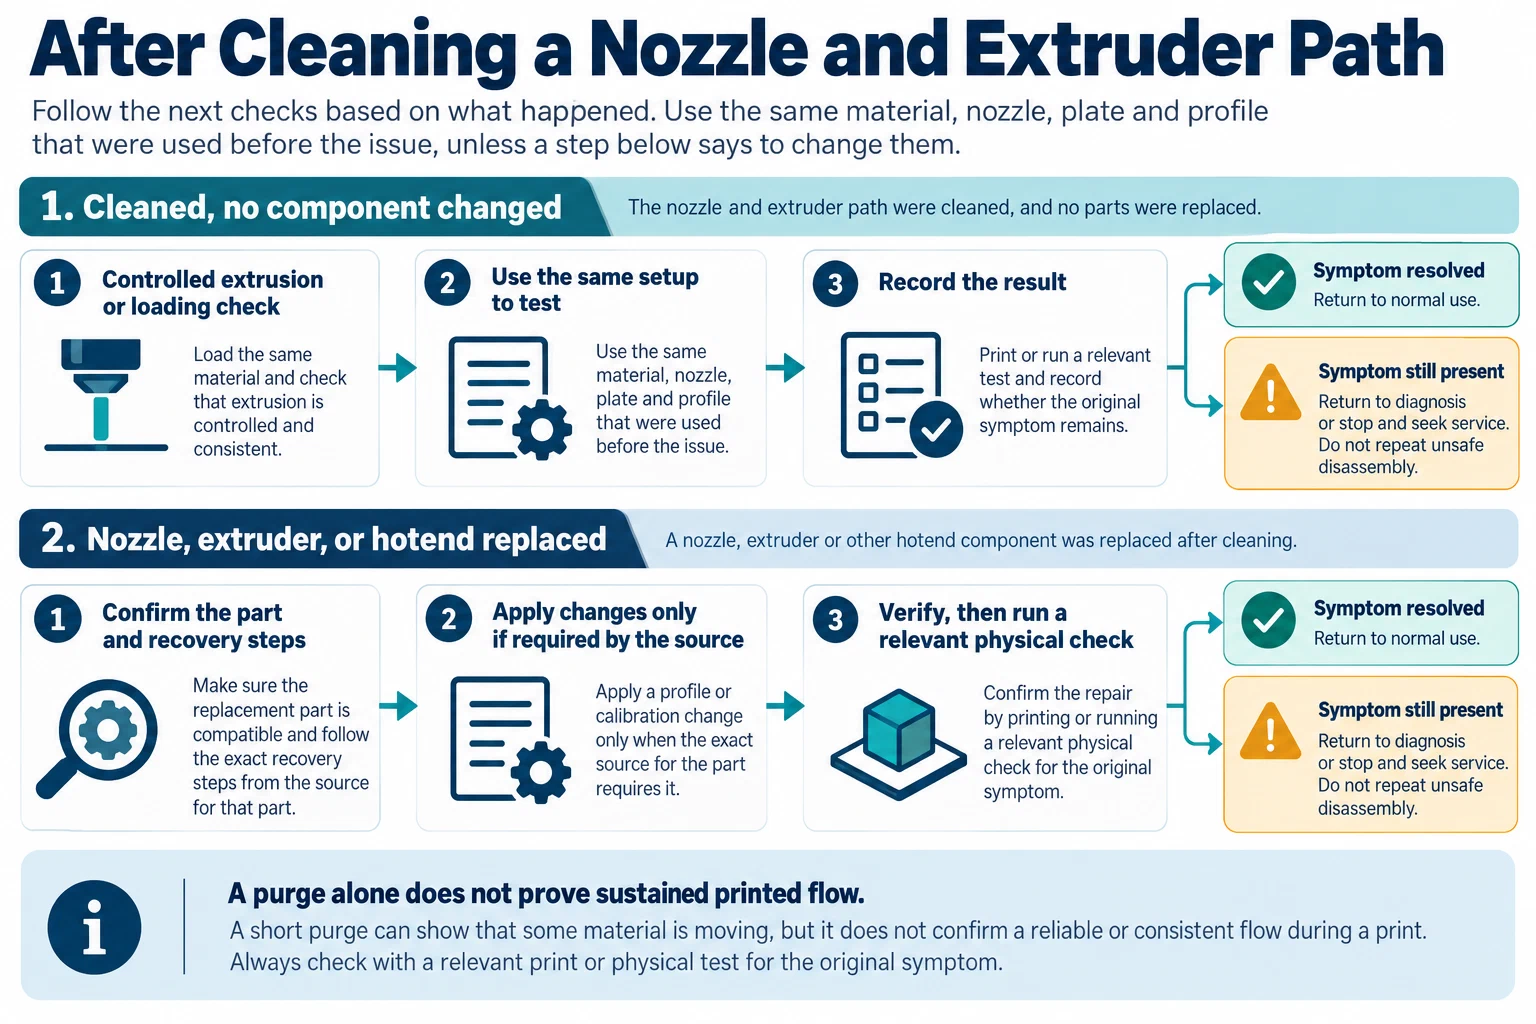
After cleaning, use the model’s controlled extrusion or loading check, then run the smallest relevant first-layer or functional test with the same material, nozzle, plate, and profile. Inspect line continuity, drive behavior, residue, and the original failure location. A clear purge does not prove a clean path under sustained demand. If a nozzle, extruder, or hotend was replaced, continue with verify a repair or replacement . If material flows but the pattern remains wrong, compare first-layer state and profile assumptions rather than repeatedly reopening the hotend. Keep the before/after result in the model-specific maintenance baseline .
Keep each Prusa nozzle path model-specific
The CORE One INDX maintenance instructions describe nozzle cleaning as needed or at the stated printing-hour check, while its cold-pull procedure gives a separate sequence for that machine. The procedure selects the filament tool for the material being removed, heats to the loaded material’s temperature or slightly above, switches the heater off, and makes the pull at the specified lower temperature. The source also warns against using an external heat source. Follow the complete current procedure, including its tool choice and stop conditions; these temperatures and steps are not a generic Prusa or cross-brand cold-pull recipe. The INDX uses a different toolhead arrangement from the MK4/S examples above, so use the CORE One INDX maintenance and cold-pull guide for its exact documented path.
Back to top ↑