Under-extrusion means that less material reached the part than the toolpath intended. It can appear as thin lines, gaps, weak walls, missing top surfaces, filament grinding, clicking, or no extrusion at all. It is an observation, not a diagnosis. A first layer that is too compressed, a mismatched profile, spool resistance, a partial clog, contaminated hardware, cooling failure, or excessive material demand can look alike.
Capture the failure pattern
Record the printer and exact variant, firmware, material product and dry history, nozzle diameter and wear, drive path, plate, slicer and version, selected printer/filament/process profiles, layer height, speed, temperature, cooling, flow, maximum volumetric speed, retraction, spool routing, and recent maintenance. Note whether the defect starts on the first layer, appears after a long print, follows one material, occurs only at high speed, or clears after a pause.
| Observation | Useful branch, not a confirmed cause |
|---|---|
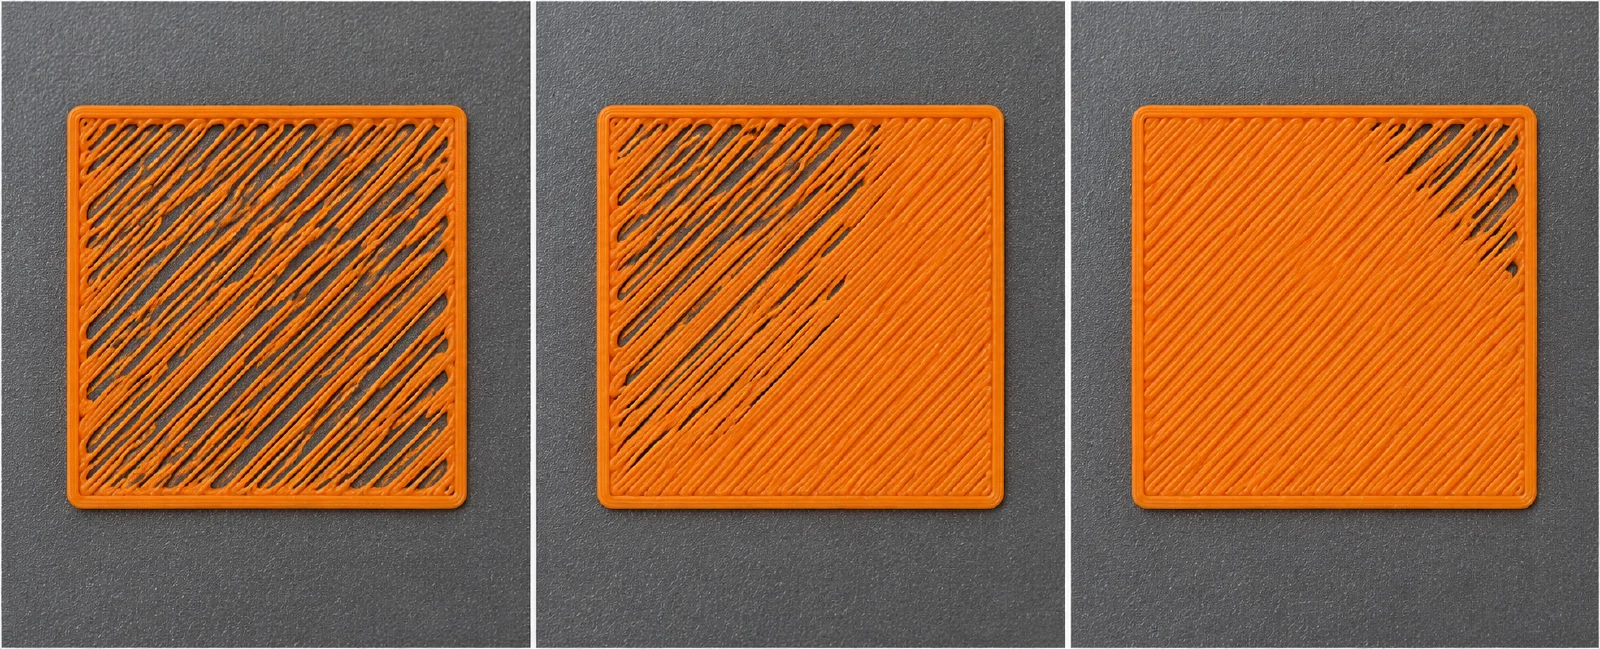
| Thin lines or regular gaps from the start | Check first-layer compression, profile/material match, flow path, and toolpath before opening the hotend. |
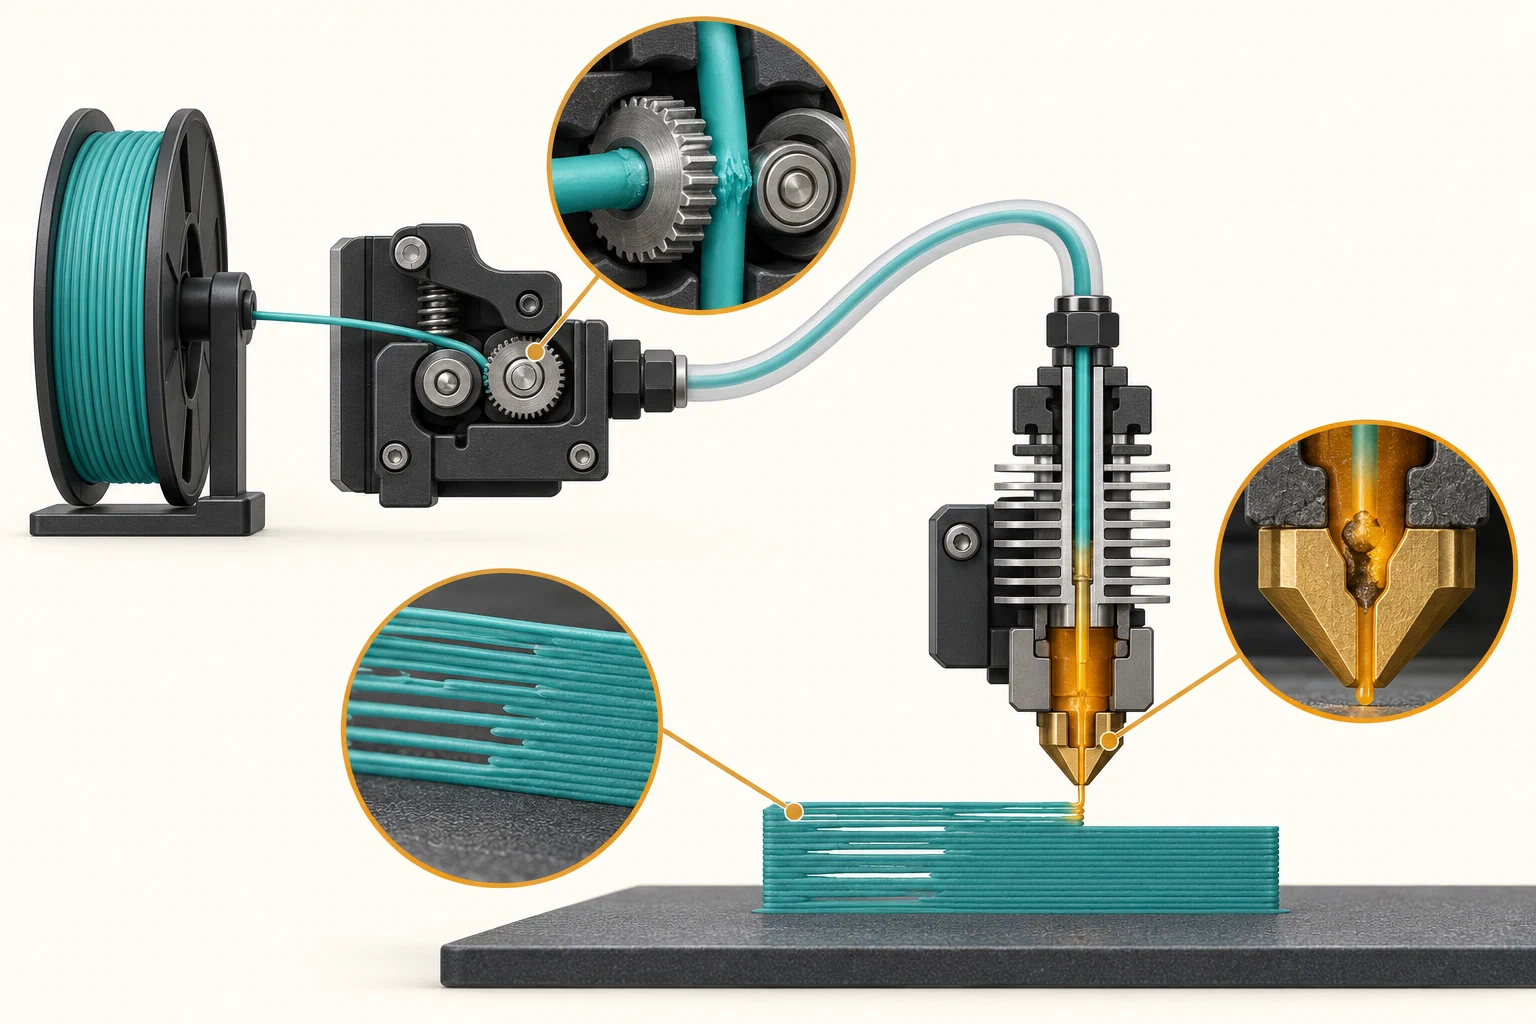
| Extruder clicking or ground filament | Look for spool drag, feed-path resistance, drive engagement, a partial clog, or demand beyond the setup’s capability. |
| Extrusion stops while motion continues, especially after a long print | Heat creep is one candidate, particularly when filament softens above the melt zone, but contamination, nozzle installation, cooling, or the drive path can produce the same result. |
| No flow after a material or nozzle change | Check loading, nozzle compatibility, installation, profile selection, and a model-specific loading procedure. |
Work from low-risk checks to service
- Stop the print if extrusion has failed. Do not resume over a missing section and call the job recovered. Preserve the failed part and the last known state.
- Confirm that the selected filament profile matches the actual material and nozzle. Compare the profile’s speed, temperature, flow, and volumetric-demand assumptions with the material maker’s guidance. Do not “fix” an unverified mismatch by raising temperature blindly.
- Check that the spool turns freely and that the filament path is not kinked, compressed, or rubbing. Inspect for a worn or ground section at the drive gear. A model-specific guide such as Creality’s SPARKX i7 procedure treats spool resistance, feed routing, ground filament, and hotend residue as separate candidate checks.
- Check the nozzle exterior and the printer’s loading or extrusion result using the manufacturer’s procedure. A controlled manual extrusion can show that material moves, but it does not prove that the print profile or sustained cooling is correct.
- If the failure appears after a long run, compare the room or enclosure condition, hotend fan state, heat-sink airflow, layer height, and material throughput with the exact printer guidance. Heat creep is more plausible when filament softens above the normal melt zone, but there is no universal room threshold or cross-printer heat-creep repair.
Separate settings from hardware work
The Bambu Lab H2C manual distinguishes full-plate under-extrusion from partial and corner-local patterns, with separate candidate checks. Keep those observations tied to that model. Its corner discussion mentions pressure advance and flow calibration together without establishing a general relationship between them; verify any named calibration in the current H2C workflow instead of transferring an inferred setting change.
Only after the feed path and printer state are plausible should you test one process variable. Reduce demand through an appropriate, documented profile or compare a small object at a known-good setting; record whether the symptom moves with speed, material, or geometry. If a nozzle, drive gear, heat break, fan, or hotend needs cleaning or replacement, follow the exact model service instructions. Do not copy a hot cleaning temperature, tool, disassembly order, or electrical step from another printer. Manufacturer maintenance pages often include burn, cable, fan, and unplugging boundaries that are part of the procedure.
Stop immediately for smoke, uncontrolled heating, exposed wiring, a damaged fan, a collision, or a hotend step you cannot perform safely. Route recurring wear or component faults to maintenance rather than compensating indefinitely in the slicer.
Check whether extrusion stopped at a filament-change pause
If the gap starts immediately after a filament-change pause, record the command, printer model, and exact point at which the job resumed before treating it as a clog. Sovol documents one SV08-specific M600 failure: that command retracts filament, and a gap can follow if the job resumes without the source-described load-and-extrude sequence. If the printer and command match, follow the current SV08 instructions. Do not transfer that sequence to another printer or treat it as a general resume rule; a resumed job still needs physical inspection.
A large blob wrapped around the hotend is also different from a blocked nozzle. Creality’s clumping guide is for the K2 Plus and includes service-sensitive cleanup instructions, so this article does not reproduce a generic hot-cleaning method. If the symptom matches, use the exact K2 Plus instructions or manufacturer support. If the printer displays a protection or fault code, record it and match its source in printer fault codes and safety stops before attempting additional extrusion.
Verify the result
After the model-specific intervention, verify extrusion with a controlled test and then print a small object using the recorded material, nozzle, plate, and profile. Inspect line continuity, wall strength, and the point where the original symptom appeared. The fix is not confirmed by one short purge or a cleared alarm alone. If material flows but the printed pattern remains wrong, inspect the generated toolpath, first-layer state, or geometry rather than reopening the hotend automatically.