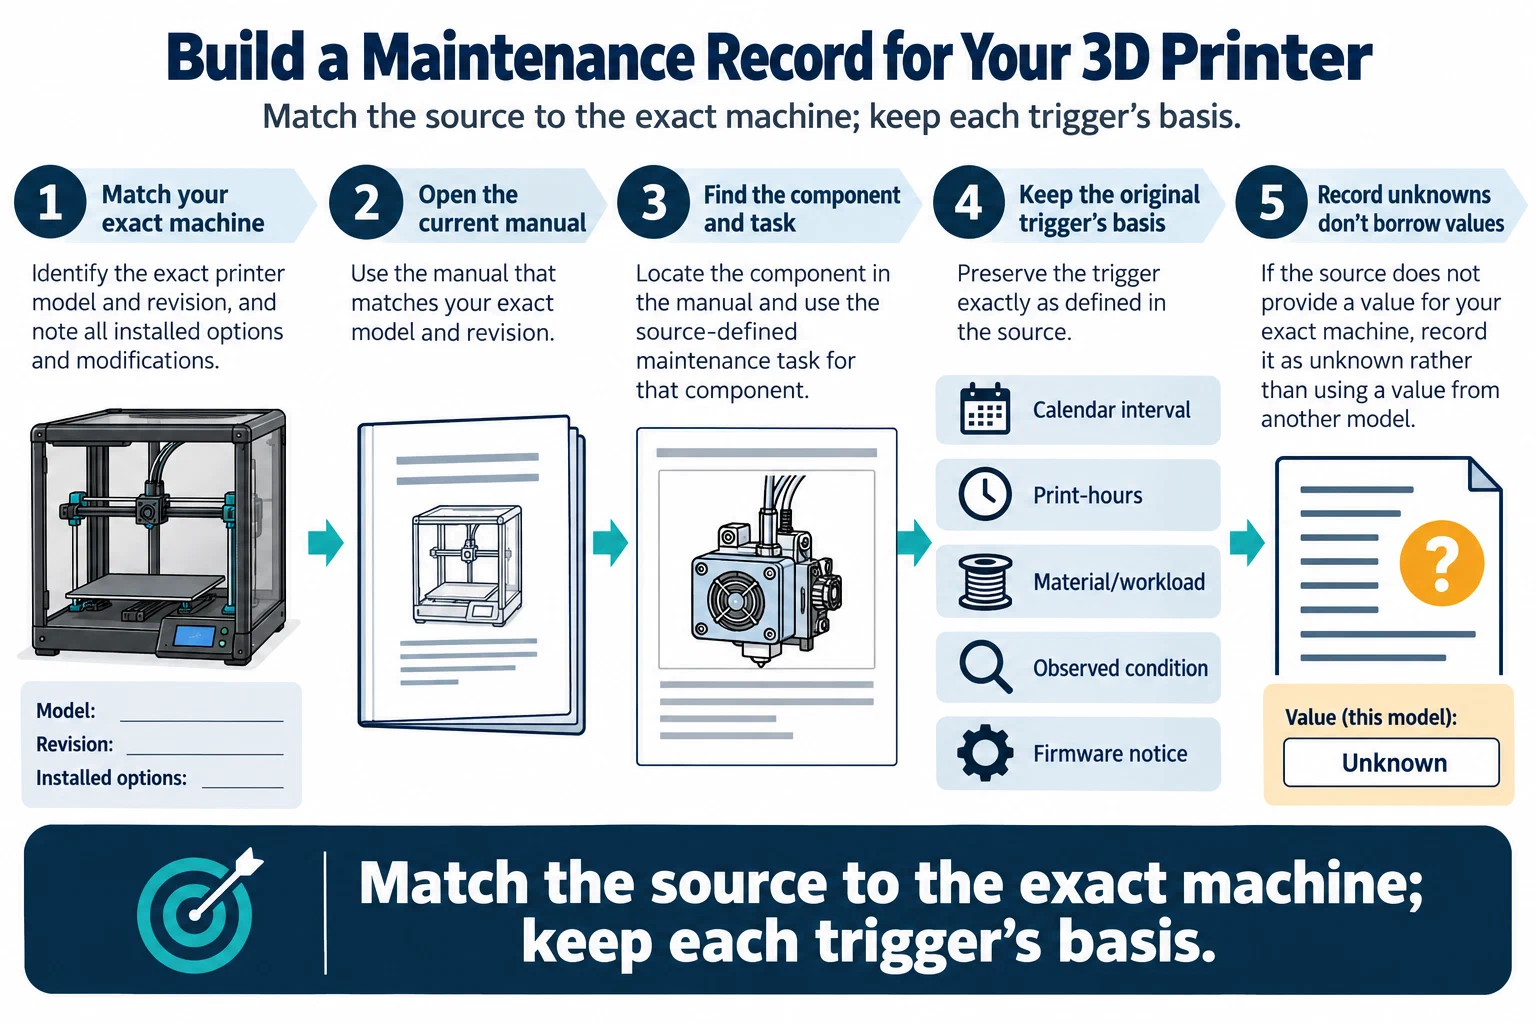
A useful maintenance schedule starts with the printer, not a generic calendar. Record the exact model and revision, firmware or hardware context, material use, environment, and current symptoms before copying any task from a manual. The result should tell you what to inspect, what the manufacturer permits an owner to do, what invalidates calibration, and what check will show whether the task helped.
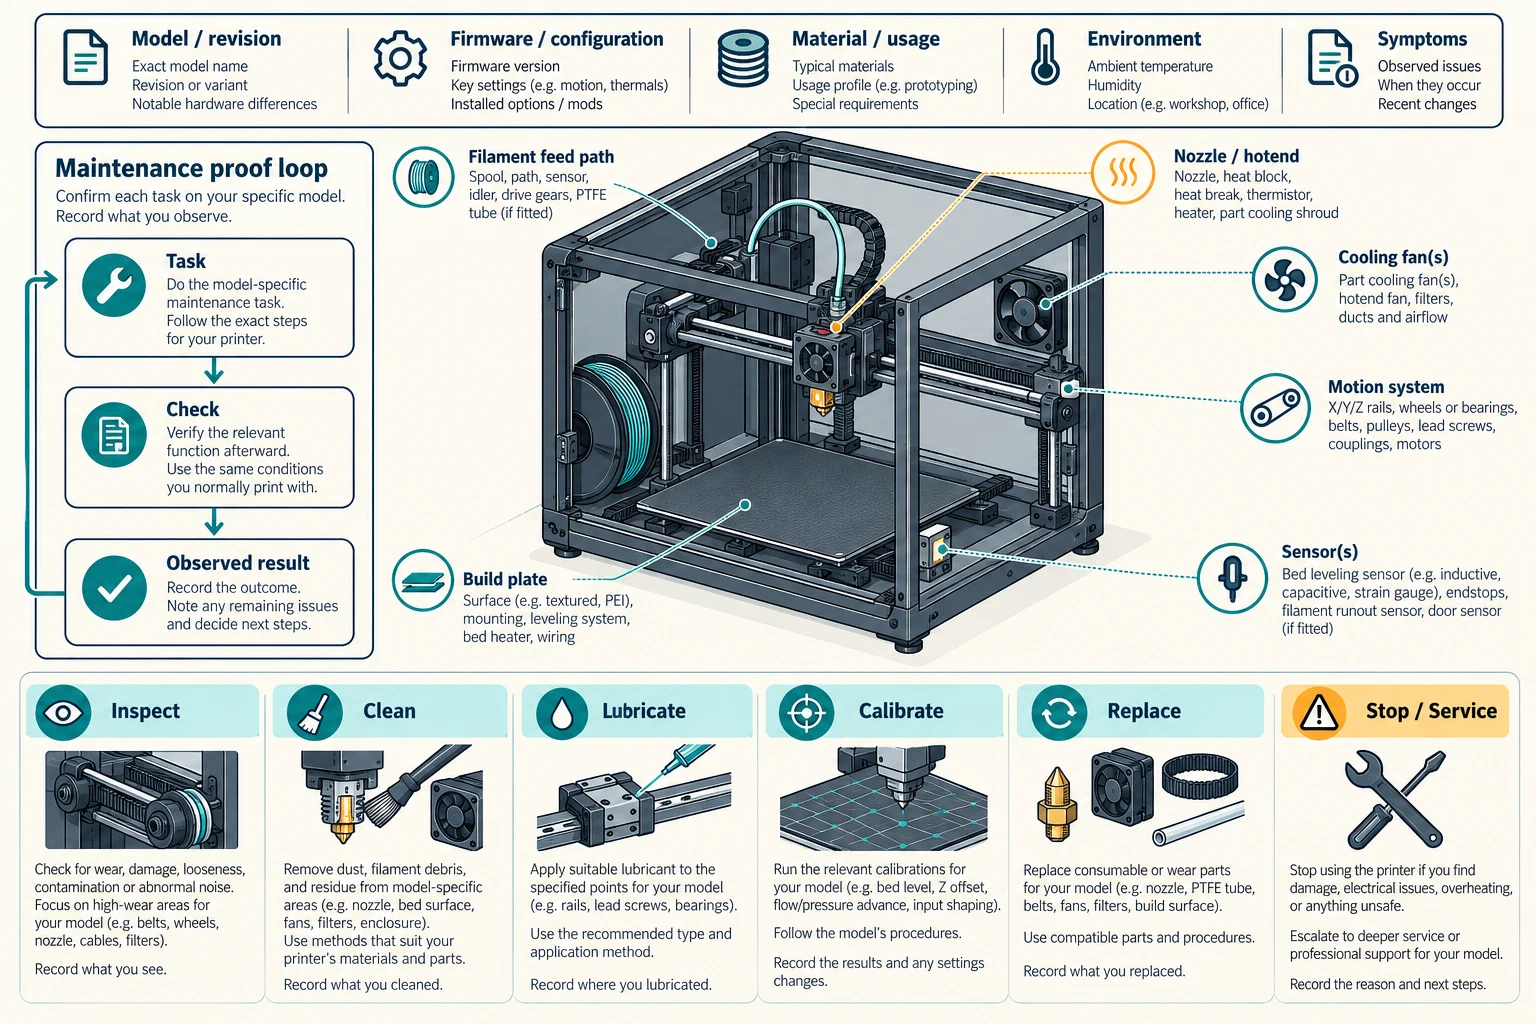
Start with an identity card
Create one record for each printer or materially different configuration. Include:
- model, revision, serial or asset label, and firmware;
- nozzle diameter and material, build plate surface, extruder or feeder configuration, and enclosure state;
- common filament families, abrasive or flexible use, dry-storage practice, and approximate print hours or job count;
- room, dust, humidity, temperature, and shared-workspace conditions;
- the current slicer and profile names when a maintenance change may affect first-layer, extrusion, motion, or cooling behavior.
Do not merge two printers because they share a brand name. A support page can identify a model and route you to a service tutorial without supplying a complete interval schedule. Creality’s Ender-3 V3 SE documentation is a useful example: it lists maintenance tips and model-specific routes for nozzle, extruder, belts, bearings, fans, axes, and temperature issues, but it does not establish a universal service interval or print-quality pass threshold.
Classify each task
Put every manual instruction in one of six columns:
| Class | Record before acting | Typical result |
|---|---|---|
| Inspect | symptom, usage state, and component condition | keep using, monitor, or isolate |
| Clean | material, residue, tool, and safe machine state | clean path or surface |
| Lubricate | exact component, product, and source-defined cadence | smoother permitted motion |
| Calibrate | changed part, invalidated setting, and firmware path | named machine check or stored value |
| Replace | part identity, compatibility, and reason | installed component and endpoint |
| Stop or service | hazard, failed check, or unclear procedure | support or qualified repair route |
A source-defined cadence belongs beside the model that supplied it. For example, Prusa’s MK4/S and MK3.9/S guide separates before-print checks, 200-printing-hour work, and annual electrical inspection. It also says not to lubricate trapezoid nuts or Z lead screws. Those are useful records for the named family, not permission to apply the same schedule or lubricant boundary to another printer.
Make the checklist verifiable
For each row, store the source link, date checked, person or operator, observed condition, action, and next test. A task is not complete merely because a box was ticked. Link bed or plate work to a first-layer check; link nozzle or extruder work to controlled extrusion and a suitable print; link motion work to homing, probing, alignment, or a representative geometry; and link fan or sensor work to the machine’s own diagnostic result.
Use the exact manual after relocation, a firmware change, a nozzle or plate change, a long period of abrasive or flexible material use, a collision, or a recurring symptom. If the manual does not state a cadence, record a condition-based trigger instead of inventing one. Usage hours are a useful context field, not proof that a component has reached a universal wear limit.
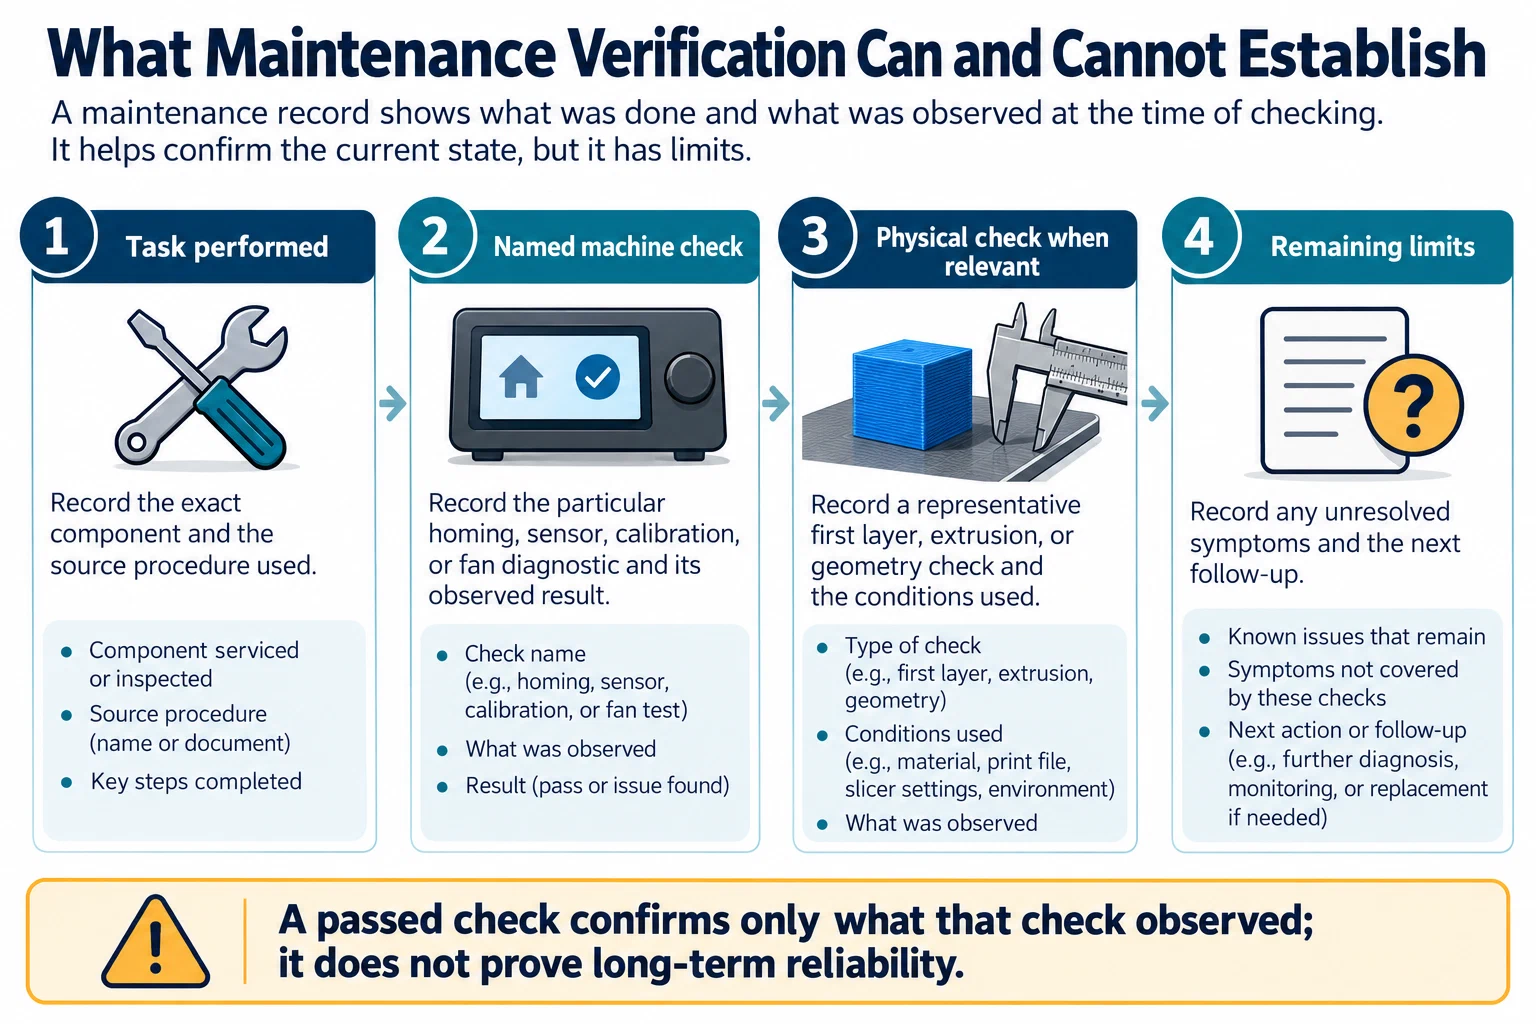
Keep safety in the record
Write the required state transition next to the task: cool-down, power-off, unplugging, guarded motion, ventilation, or a prohibition on opening a covered assembly. NIOSH recommends a context-aware hierarchy of controls for makerspaces, schools, libraries, and small businesses; it does not provide a universal exposure limit or make every maintenance action safe for every model. Stop for smoke, uncontrolled heat, exposed wiring, damaged connectors, unexpected motion, or a failed safety check.
When a symptom appears, preserve the state before changing several variables. Use cleaning the nozzle and extruder path for feed-path work, belts, rails, fans, and sensors for component checks, and verify a repair or replacement after service. For thin lines or stopped extrusion, also compare the maintenance record with under-extrusion, clogs, and heat creep .
Preserve the trigger and the exact model
Manuals show why a checklist cannot be reduced to one interval column. The Bambu Lab H2D manual makes some reminders depend on firmware and task duration, while separating tasks for 3D printing from checks that apply only to configured laser equipment. Its 3D-printing maintenance table gives different cadences to different parts and calls for more frequent care under sustained high-temperature or engineering-material use. The P2S manual has its own weekly, monthly, and quarterly tasks, and changes some intervals when high-temperature materials are used continuously or for a high daily average. Record the firmware reminder, usage trigger, and installed configuration that actually apply; do not combine these schedules or generalize them to another printer.
The QIDI Q2 manual likewise ties lubrication to named axes, lubricant types, and condition as well as a stated range. The QIDI Plus5 manual gives separate Z lead-screw and X/Y shaft schedules, while its fan checks are condition-led; keep both QIDI models’ values attached to their own manuals. For the Prusa CORE One INDX, some work is linked to printing hours, while the rail lubrication cadence, conditional bearing work, and belt inspection have their own rules. A record should preserve whether a task is triggered by calendar time, print hours, material workload, observed condition, or a firmware notice. Where the source gives no number or pass threshold, leave that field unspecified and record the observed result instead of inventing one.
Creality’s SPARKX i8 FAQ separates calibration from cleaning: it describes pre-print calibration for each job, but gives no numeric plate-cleaning interval. Record those as different tasks rather than treating a calibration check as a maintenance schedule.