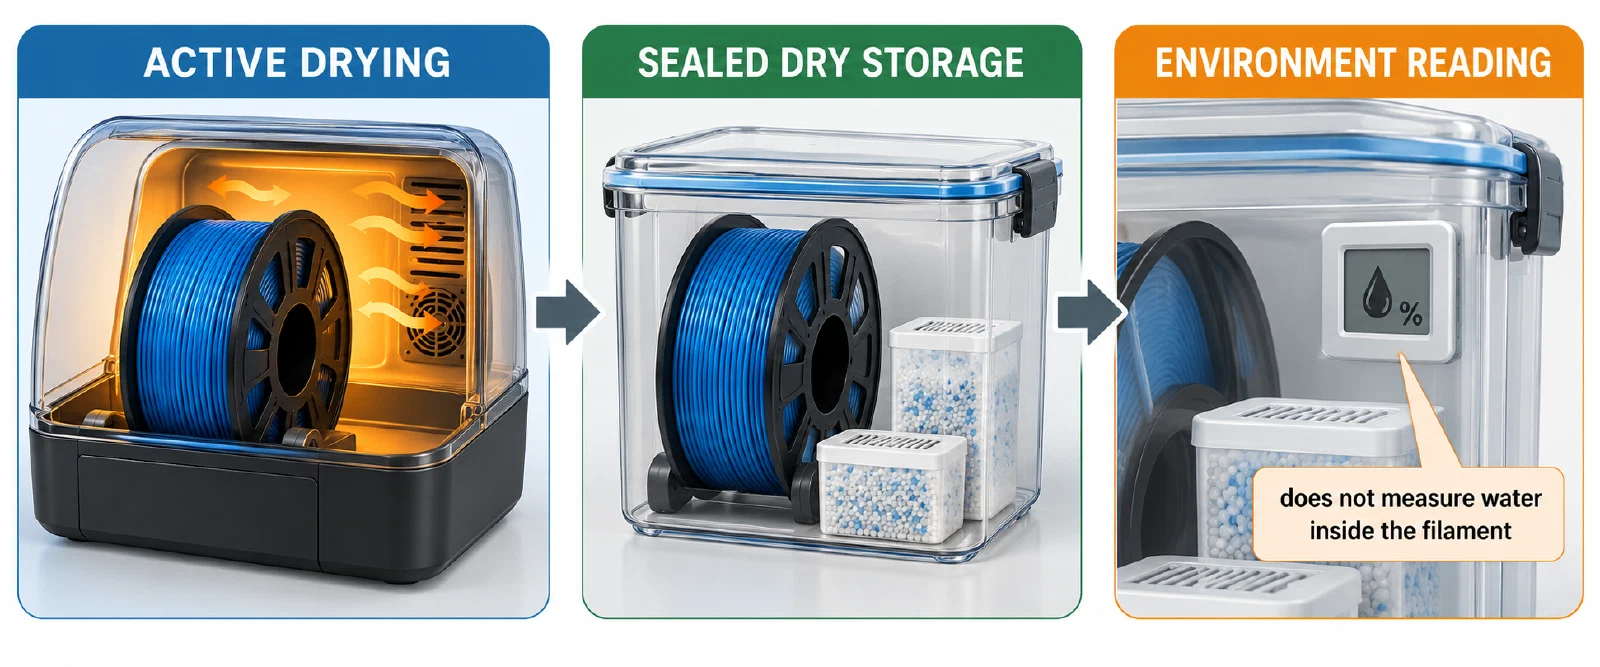
Moisture can change how filament feeds, melts, and bonds, but a wet-spool diagnosis should not be made from one symptom. Rough surfaces, bubbling, hissing or crackling, strings, blobs, smoke, and weak layers can also come from temperature, contamination, cooling, geometry, or a mechanical problem. Treat drying as a controlled material check, not as a universal cure.
Start with the exact product
Record the manufacturer, product or grade, color or additive, filament diameter, spool construction, and whether the package has been opened or exposed. Hygroscopicity varies: Prusa identifies polyamide, polypropylene, PVA, and BVOH as particularly moisture-sensitive, while its guidance describes PLA as less affected by ordinary humidity exposure. “PLA,” “PETG,” or “nylon” is not enough information to select a safe drying temperature.
For a recycled-content product, also record whether the claim concerns the polymer, a reinforcement, or both, along with any stated source and batch details. The recycled-filament guide explains how to keep those claims separate from the drying record.
Manufacturer tables are examples, not a cross-brand recipe. For example, one Prusament table lists PLA/rPLA at 45 °C for 6 hours, PETG at 55 °C for 6 hours, TPU at 60 °C for 4–6 hours, ASA at 80 °C for 4 hours, and PA11 carbon fiber at 90 °C for 6 hours. Those values remain tied to the named product table and its spool limits. Check the current product instructions before using any number, especially for cardboard or temperature-sensitive spools.
When product instructions disagree
Before heating, match the exact product or formula and spool generation to the supplier’s current product page or data sheet. Check that the dryer can control the stated conditions and that its limits fit the spool; include the package and exposure history in the care record. If product instructions disagree, keep their contexts separate and ask the manufacturer which applies. For example, the current Prusa drying table lists PC Space Grade at 90 °C for 4–6 hours, while the Prusament PC Space Grade Black product page recommends 60 °C for 6 hours. Neither source says which instruction controls. Do not choose or average the schedules; confirm the current instruction for the exact product and spool with Prusa before drying.
Product sheets can also differ within one family: Polymaker PLA Pro v6.0 lists 55 °C for 6 hours for that named product. Treat this as another product reference, not evidence that all PLA needs that schedule. If you use a powered dryer, follow its handling instructions as well as the filament sheet. The Polydryer manual warns that a loose filament end can obstruct a heating vent; keep the strand wound or secure its tip at the outlet while drying.
A product-first drying workflow
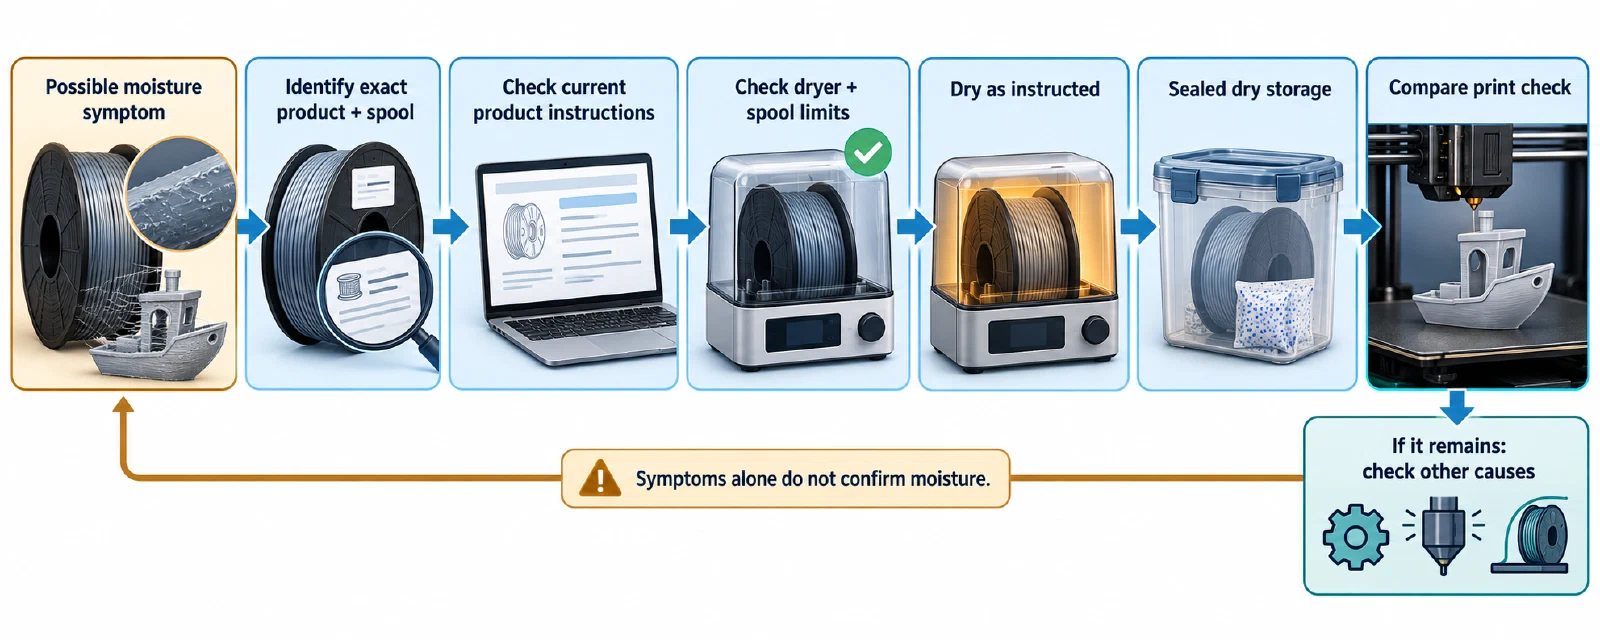
- Check the product data. Find the manufacturer’s drying temperature, time, spool limit, storage condition, and any equipment warnings. Do not substitute printing temperature for drying temperature.
- Separate drying from diagnosis. Note the current symptom and keep other changes stable. A dry spool that still shows the problem points you toward temperature, extrusion, cooling, surface, geometry, or machine checks.
- Use compatible equipment. Confirm that the dryer or oven can control the required temperature and that the spool will not deform or touch a heating surface. Never exceed the spool or filament manufacturer’s limit. Do not treat smoke or severe bubbling as evidence that more heat is safe.
- Follow the equipment procedure. The Prusa/Memmert workflow is specific to that oven and its compatible unwrapped spools. It warns against drying different materials together because their settings differ, and it directs users to start with the material-specific table.
- Protect the handoff. Move the spool promptly from active drying into a sealed container or drybox. A drybox with desiccant slows moisture uptake and can feed filament, but the Prusa USS Drybox guidance explicitly says it does not dry already-moist filament.
Storage while printing
Use a sealed bag, box, or drybox with fresh desiccant suited to the container. Check seals and avoid leaving the lid open while preparing a print. A drybox hygrometer reading describes that box and its stabilization time; it does not prove a particular spool has reached a universal moisture endpoint. As one product-specific example, Prusa lists below 30% relative humidity for PLA and below 20% for PETG, TPU, PVA, and BVOH in its USS Drybox guidance. Do not transfer those numbers to every drybox or filament.
Container relative humidity and an indicator-card color describe the environment or that indicator’s response; neither directly measures water inside the polymer. Laboratory water-content methods use a defined method and sample, and the ISO preview does not validate a consumer test on spooled filament. Record what each device measures and any stated calibration limits separately from the before/after print response.
Record the dry-state check
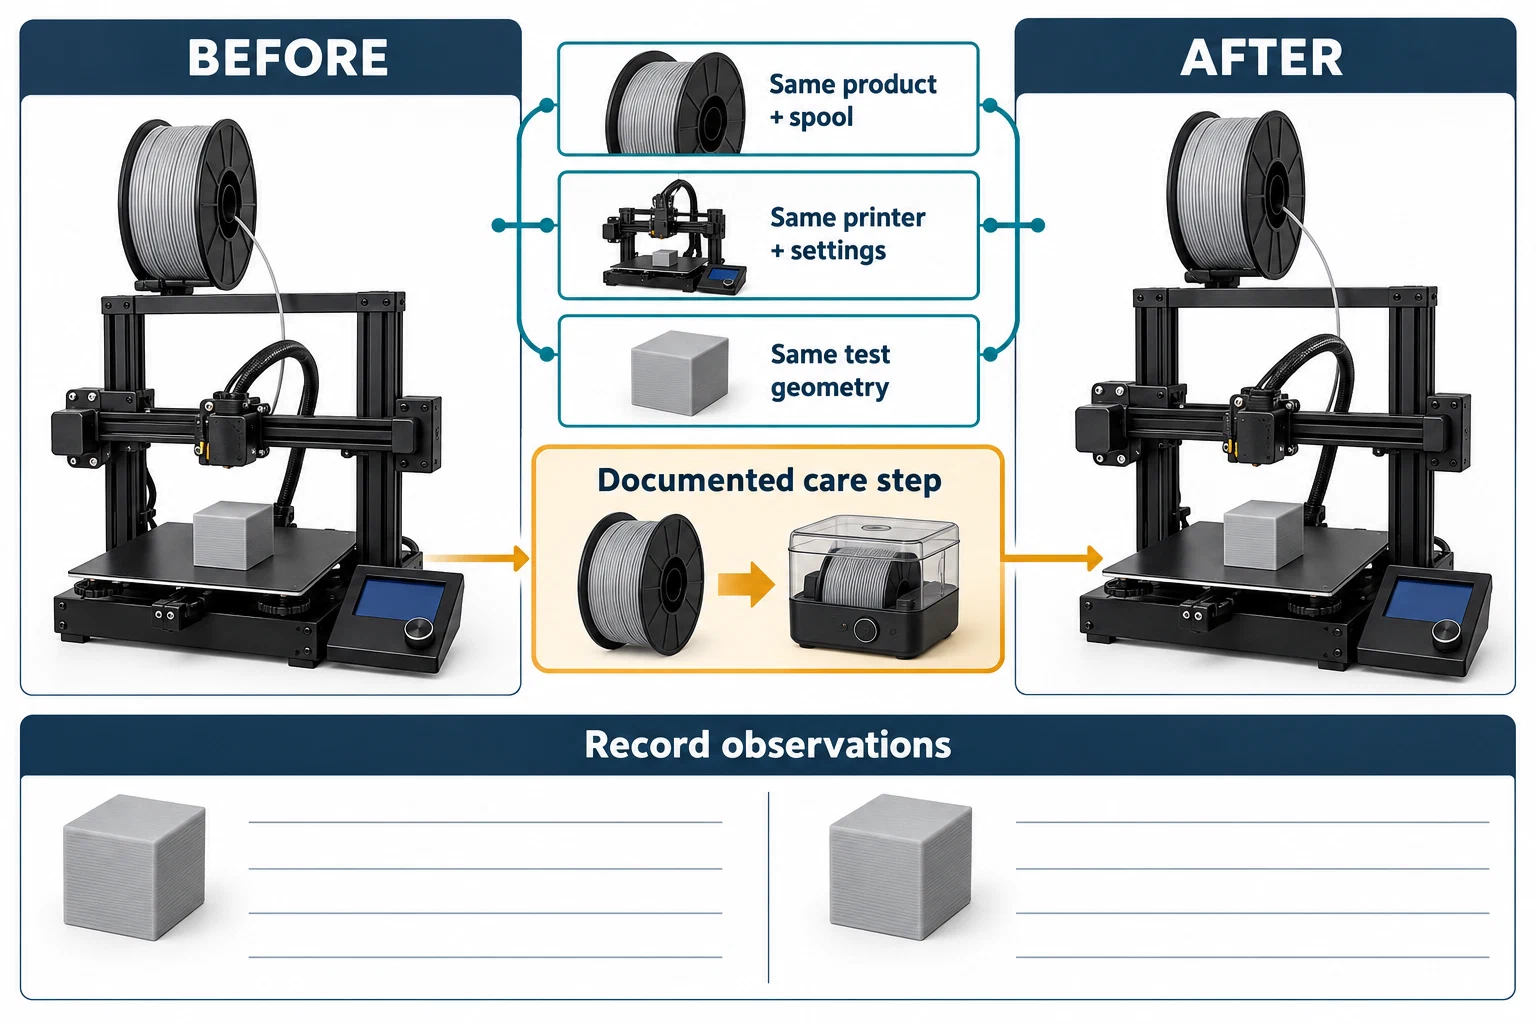
For a repeatable result, write down:
- exact product, grade, color, diameter, and spool construction;
- exact spool generation, the product instruction source and version/date used;
- package state and approximate exposure history;
- dryer or oven model and calibration or displayed temperature; for a drybox hygrometer or indicator, record its type, stated calibration limits, and reading/state as environmental/device information;
- drying temperature, duration, and the manufacturer instruction used;
- storage container, desiccant state, and handoff/feed path after drying;
- the test object and geometry, unchanged settings, symptom before drying, and result after drying.
If the result is still poor, keep the record and test one other cause at a time. If the manufacturer does not provide a safe drying method for the exact spool, do not invent one from a family label or from a different brand’s table.
Back to top ↑