Purge is not one setting with one correct value. A color transition, an incompatible-material transition, and a support interface have different cleanliness, bonding, removal, and waste requirements. The right choice depends on the automated system, slicer release, nozzle and tool arrangement, material pair, dry state, model geometry, and the result you need.
Identify what the change must accomplish
First label the transition:
- Same material, different color: the main risk is residual color in the melt path and visible contamination. A transparent wall can expose material that was flushed into infill.
- Different materials: check the manufacturer’s pairing and temperature boundaries before attempting a change. Adhesion, viscosity, thermal window, and moisture can matter more than color.
- Support base or interface: decide which material should touch the model and which should form the bulk support. The interface material can improve removal or surface quality, but it adds a tool assignment and usually another change sequence.
For one system-specific example, Snapmaker’s U1 FAQ labels polymer-family pairs “Strong Bonding” or “Bondable.” It does not define whether matrix rows and columns represent the base and interface materials, and it gives no product-specific test conditions. Treat the labels as manufacturer classifications for that U1 context; verify the exact filament products and run a small interface print, since the labels do not establish the result for your materials or geometry.
Intentional optical blending is a separate goal from clean color separation. For a documented color-mixing workflow and a local swatch process, use mixed colors and printed swatches ; do not label a planned blend as contamination or use purge settings to correct a recipe that simply looks different from its preview.
Record the exact base material, interface material, product, nozzle, feeder or tool, slicer release, profile, dry state, and model surface. OrcaSlicer exposes separate support-base and interface choices, but a slicer assignment does not prove that the hardware can feed, purge, bond, or remove the pair.
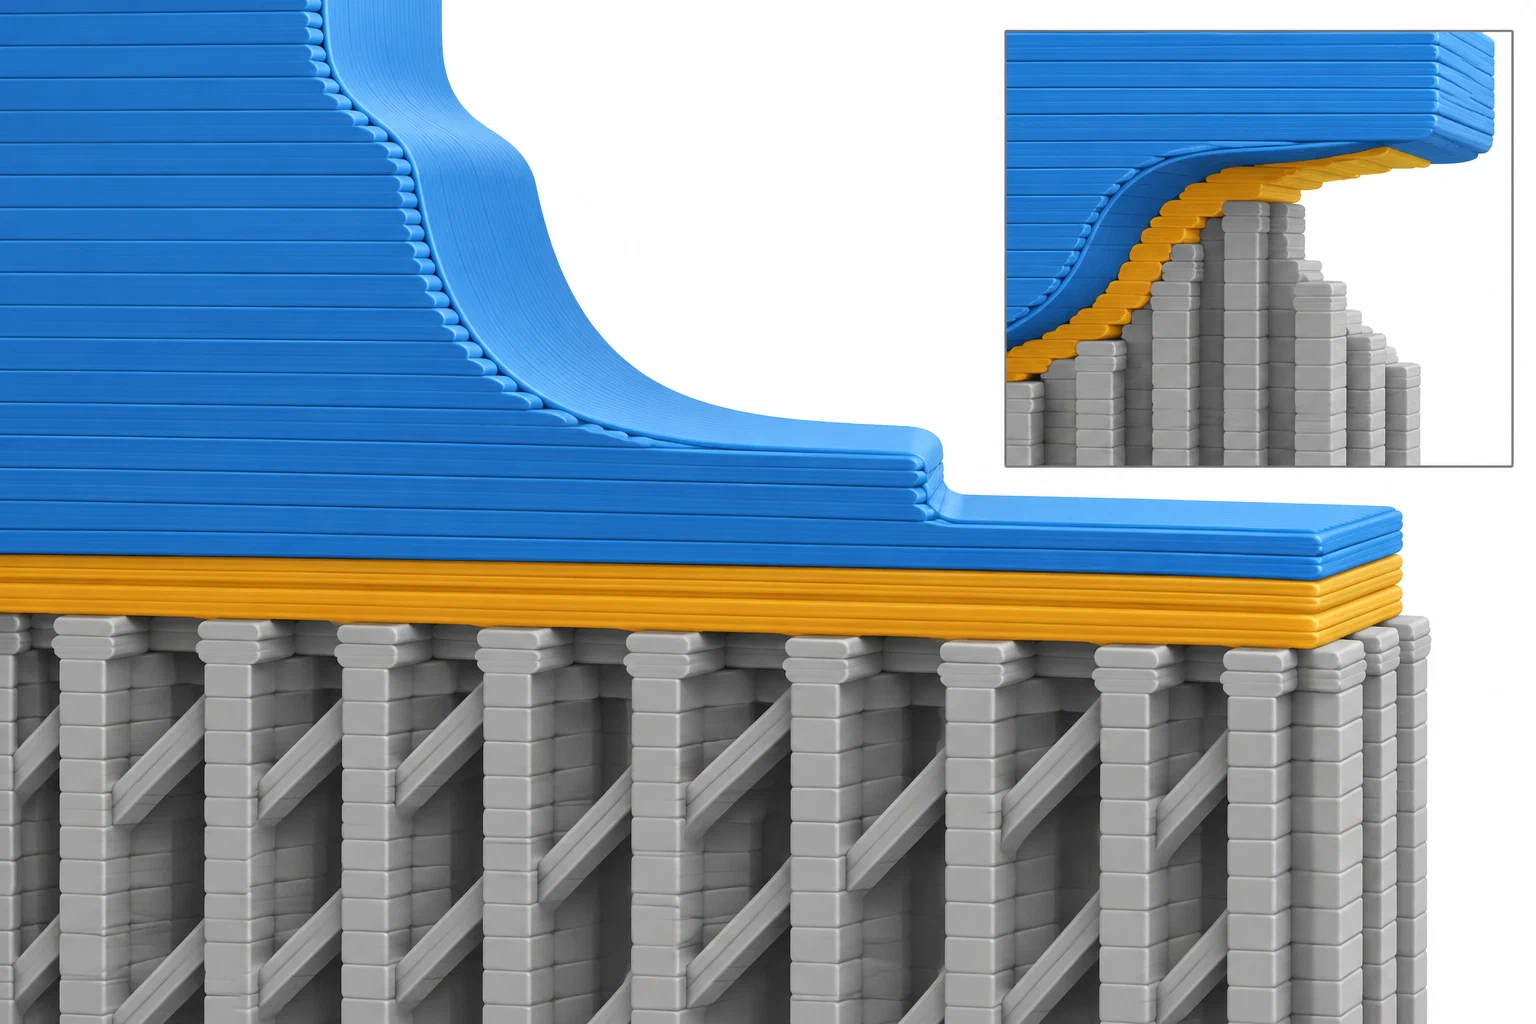
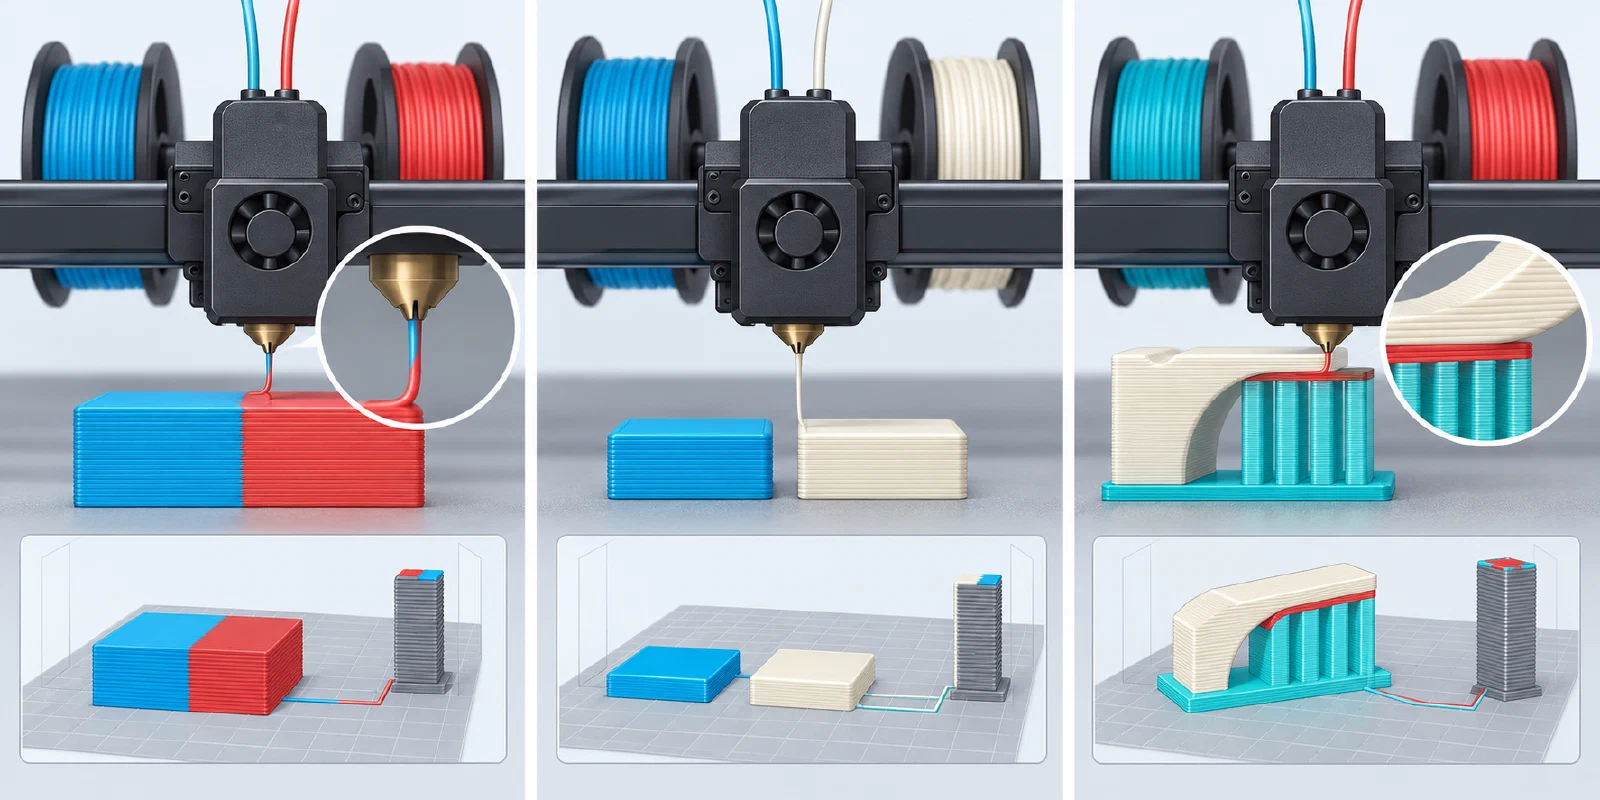
Inspect the sliced tool-change plan
Preview the job before printing. Check which tool supplies the outer wall, inner wall, infill, support, interface, prime tower, wipe object, and any flush destination. Count the transitions in a representative layer and look for a material being assigned to a tool that is not physically mapped.
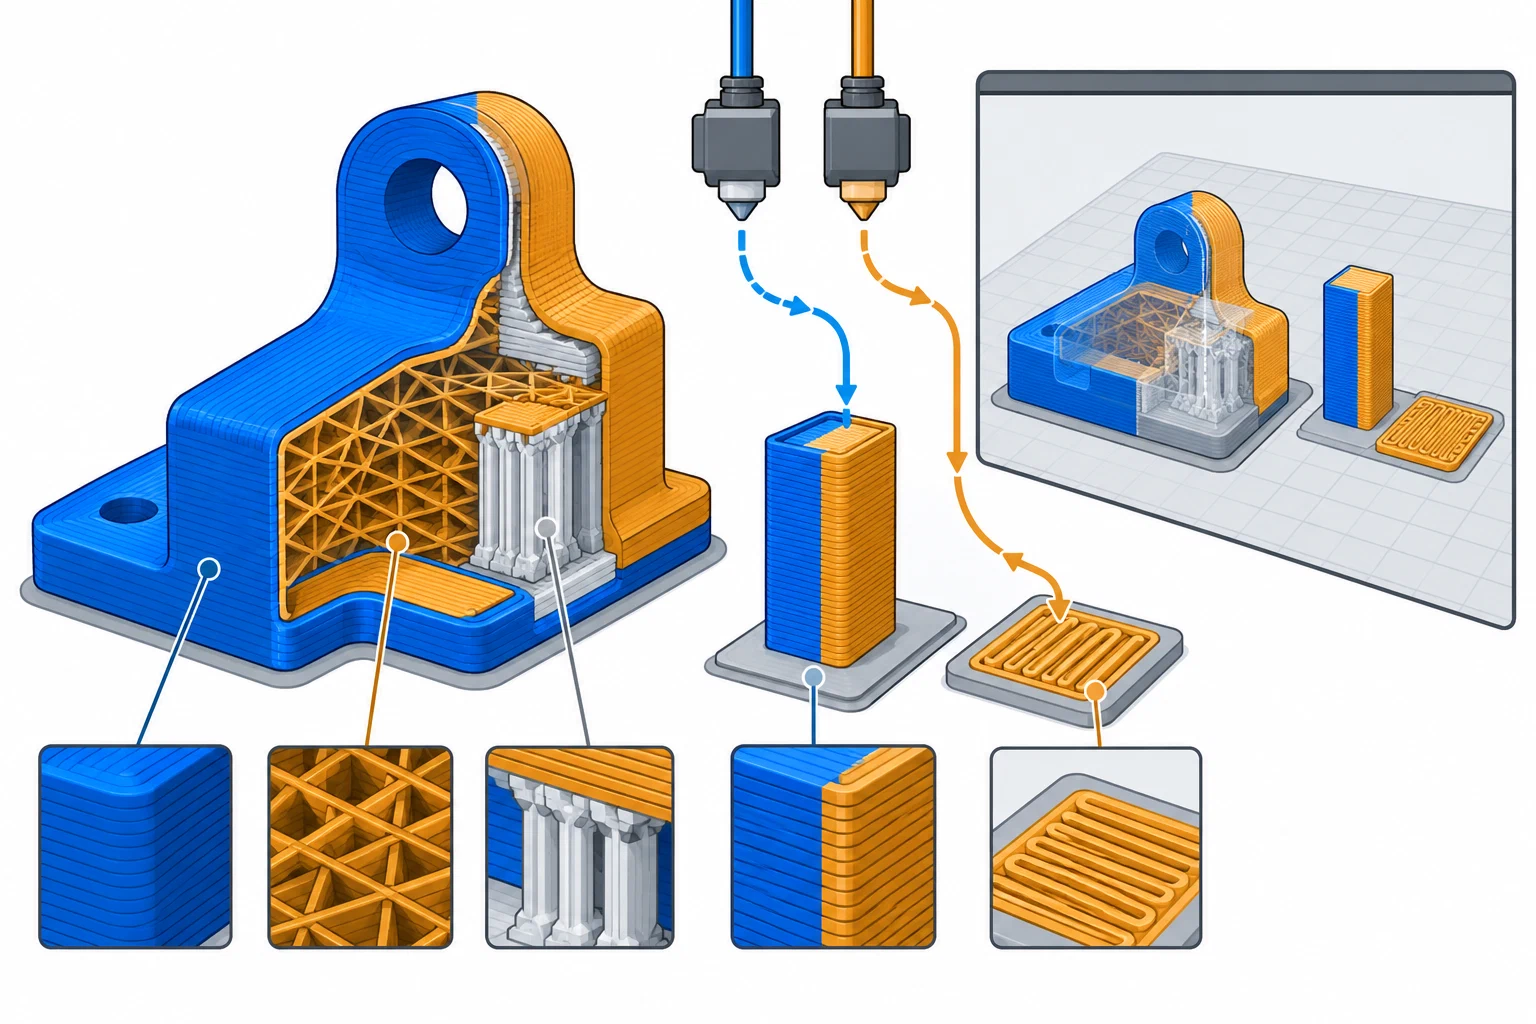
Slicer controls are coupled. OrcaSlicer documents flushing into object infill or support as destinations that require a prime tower. Infill can reduce waste and time, but mixed material can remain visible through a transparent wall. Its prime-tower controls also include volume, geometry, purge speed, and sparse-layer behavior; higher speed can affect stability and collision force. These are control semantics, not a validated setting for your printer.
Creality Print 7.3 describes reusing purge in hidden object infill while protecting outer walls and top/bottom surfaces; material that cannot be placed in the internal structure remains assigned to the wipe tower. Its release notes caution about solid or thin-wall models, color-bleed risk, and parts with strict weight, strength, or internal-structure needs. This is a version-specific slicer feature, not a universal purge destination or a tested quality result.
If you use a different slicer or system, use its own documentation and inspect the generated preview or tool-change commands. Do not copy a Prusa, OrcaSlicer, Bambu, or open-source feeder value into another ecosystem because the field has a similar name.
Treat purge values as starting points, not proof
Prusa documents a default filament-change purge and a larger suggested starting range for its MMU2S/MMU3 soluble-support workflow. That guidance is explicitly tied to Prusa systems, PVA/BVOH, and the named slicer workflow. Prusa also describes a Prusa XL default wipe tower for broad material coverage and reliability, with disabling it allowed only under conditions such as dry filament and regular monitoring. Neither source establishes a universal purge volume or a safe no-tower rule for AMS, IDEX, or another tool changer.
Use the material manufacturer’s limits and the exact automated-system profile. If the first test shows a color tail, residue, weak interface, a blocked tip, or an unstable tower, record the observation before changing the relevant purge, handoff, temperature, or speed control. Change one variable and repeat a small test. Do not hide contamination by increasing every purge-related value at once.
Keep exchange claims within their scope. The Bambu H2C manual’s Vortek hotend-change sequence describes docking and exchanging a hotend; its no-purge wording does not mean the initial filament-entry path requires no purge. In OrcaSlicer’s multi-extruder Type 2 wipe-tower workflow, the documented wait-for-temperature option is gated to nightly builds or releases later than 2.4.2. A firmware or tool-change macro that already waits can create a second wait, so check the installed build and target macro before changing it. Neither note establishes a purge volume or print outcome.
Compare support-interface choices on a small model
For each candidate pair, print a small geometry that includes the intended interface and a representative color or material transition. Check:
- whether the selected tools load and unload without a feed error;
- whether the interface bonds where it should and releases where it should;
- whether residue or the previous material remains on visible surfaces;
- whether the tower, wipe object, or flush destination stays stable and clear of the nozzle path;
- how much material is discarded and whether the result justifies the extra changes.
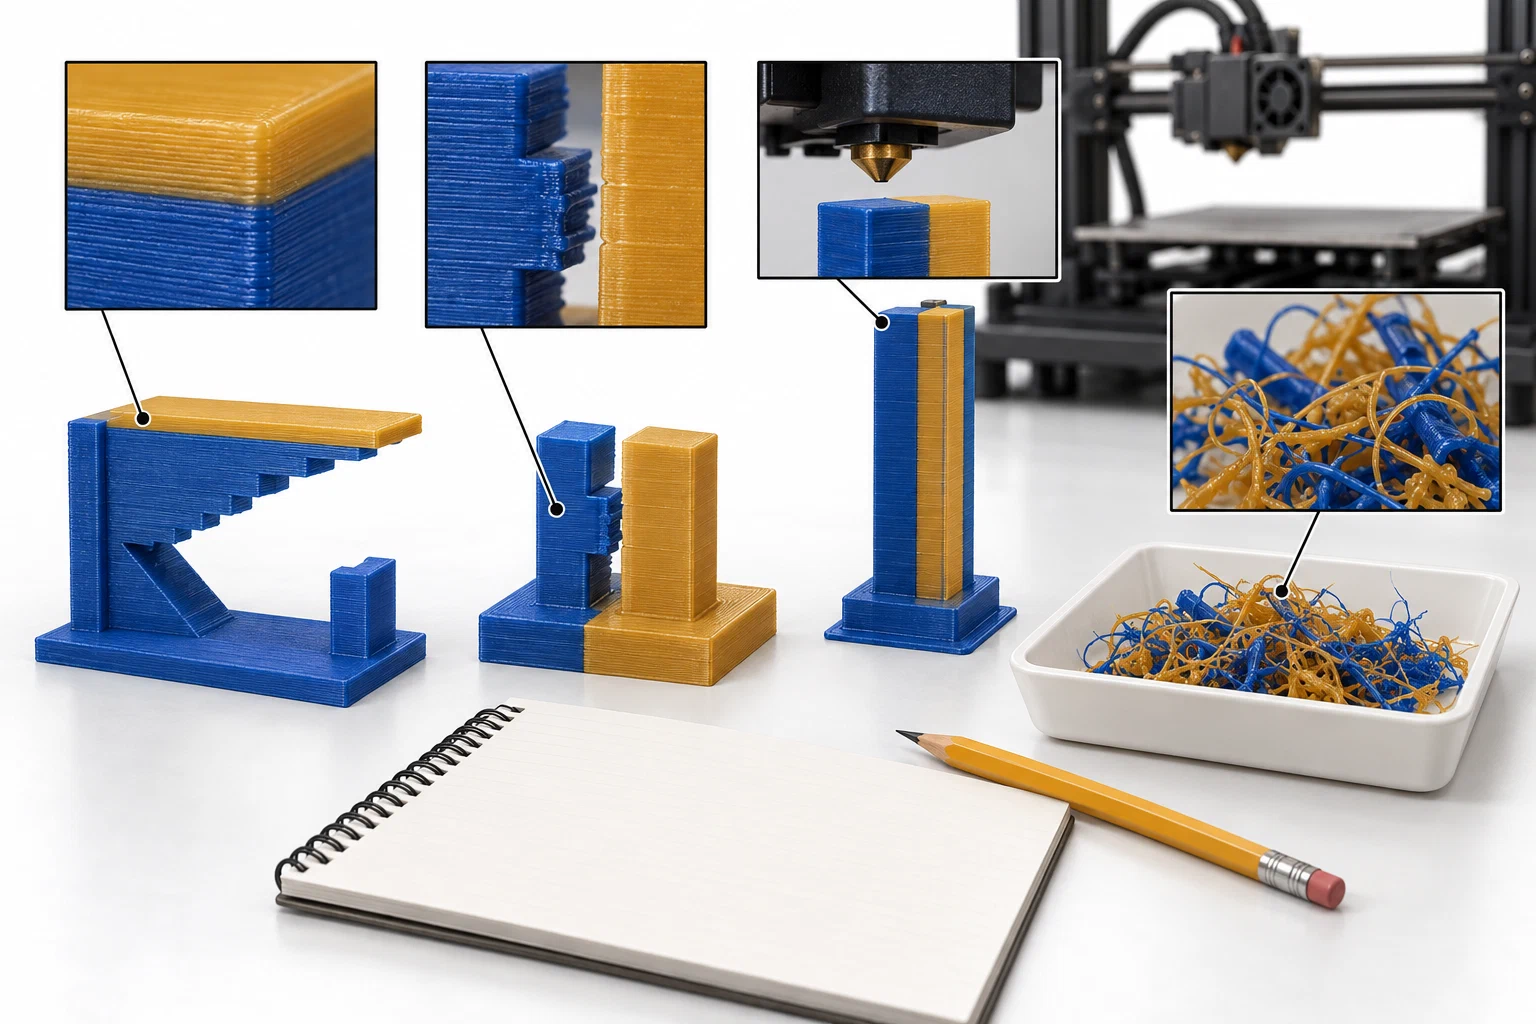
This board is illustrative: use it as a guide to what to inspect, not as a result for a particular printer or material pair.
Record the model, layer height, nozzle, temperatures, material products, dry state, tower or flush controls, observed result, and next change. A support interface that looks clean on one geometry may fail on a different overhang or contact area. Use the portal’s calibration guidance when the geometry or material change requires a repeatable comparison.
Keep material and support limits visible. For example, Prusa’s soluble-support mapping and purge guidance is not automatic detection of the loaded material, and the AMS HT material list is specific to that feeder and product labeling. If compatibility is unclear, defer the combination until the exact manufacturer guidance or a controlled test resolves it. Never claim that a purge setting guarantees clean transitions, strong bonding, or unattended success.
Back to top ↑