A temperature tower compares a controlled set of nozzle temperatures for one filament product. It can reveal changes in surface finish, bridging, stringing, overhangs, and apparent layer bonding, but it does not identify one universal best temperature. The best-looking section may be weak, may behave differently on a functional geometry, or may only look better because another variable changed. Treat the selected value as a provisional material-and-process result.
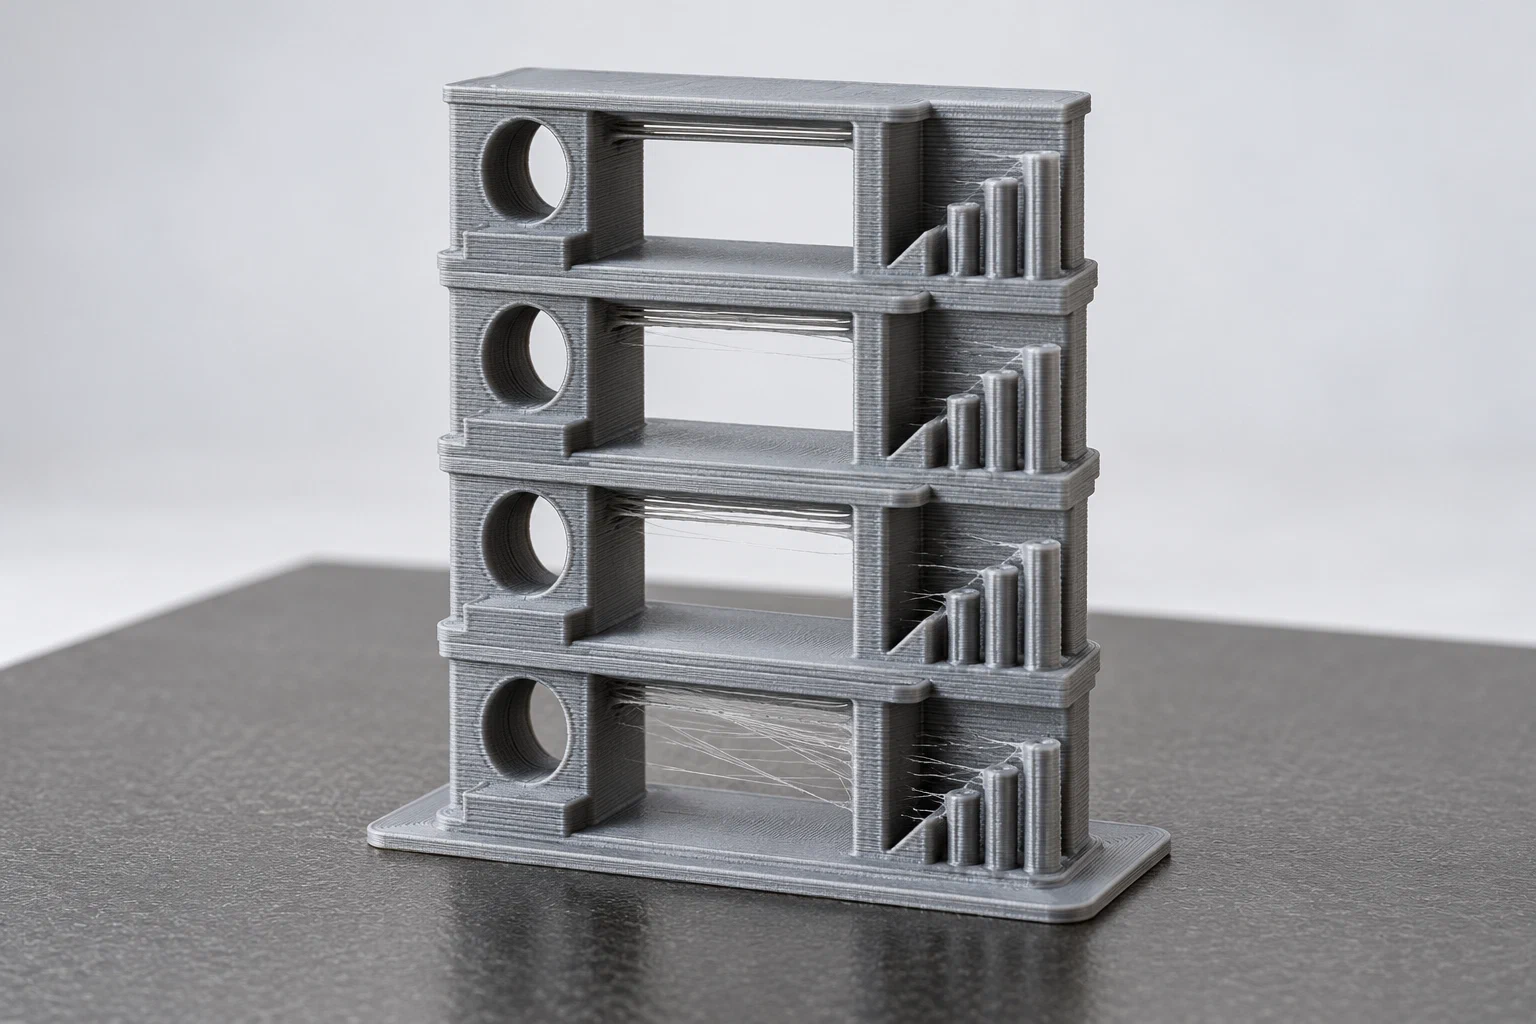
Illustrative comparison only; the image is not a measured tower result.
Choose a safe, bounded range
Start from the temperature range and handling instructions for the exact filament brand, product, grade, and printer. Record whether the product is standard, filled, recycled, high-flow, or otherwise modified; color and additives can change behavior. Confirm the nozzle material and diameter, plate, first layer, layer height, line widths, speed, cooling limits, enclosure or ambient conditions, and dry state. Do not begin outside the product or printer’s documented limits merely to make a tower more dramatic. If the filament is wet, dry or replace it according to the material guidance before attributing stringing or surface defects to temperature.
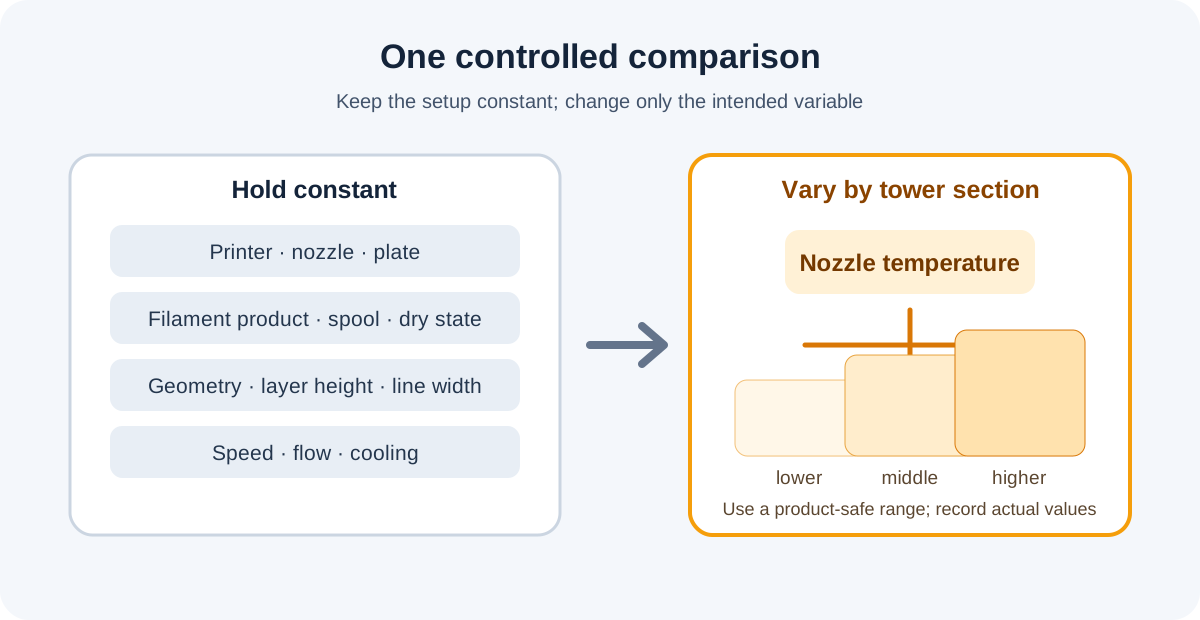
The tower is informative only if its process is known. Keep the same printer, nozzle, plate, filament spool, layer height, line widths, speeds, flow, cooling schedule, and geometry throughout the comparison. Use the slicer’s current temperature-tower workflow for the installed release, because generated test patterns and temperature-change mechanisms can be version-sensitive. OrcaSlicer v2.4.0 Alpha release notes say its generator scales tower geometry by nozzle size and adjusts the temperature range and layer height for the resized model; they provide no formulas or physical validation. For that release, inspect the generated tower and temperature mapping in preview instead of assuming each printed height corresponds to the same schedule across nozzle sizes. Check the preview and machine-start code before printing so the temperature changes are actually represented and do not conflict with printer-specific startup behavior.
Run and inspect the comparison
- Record the product label, spool or batch if available, dry-state treatment, nozzle, plate, slicer release, and intended use of the printed part.
- Choose a product-safe temperature interval and an increment that gives enough sections to compare without pretending the optimum is more precise than the test can resolve.
- Generate or configure the tower using the current slicer instructions. Confirm that only the intended nozzle-temperature variable changes and that bed temperature, cooling, speed, flow, and layer height remain as planned.
- Inspect each section under the same lighting and, where useful, gently test strings, bridges, overhangs, and layer separation. Record surface artifacts, seam or corner behavior, bridge sag, stringing, visible gaps, brittleness, and any dimension or fit change.
- Choose a provisional window rather than a single magic number. A temperature that improves bridging may not maximize surface appearance or strength, and a clean tower does not prove the value on a large, enclosed, thin-walled, or heavily retracted model.
The outcome matters as much as the temperature. Tensile studies compare named materials, printers, and specimen designs; their results do not turn a tower segment into a strength rating for another product or machine.
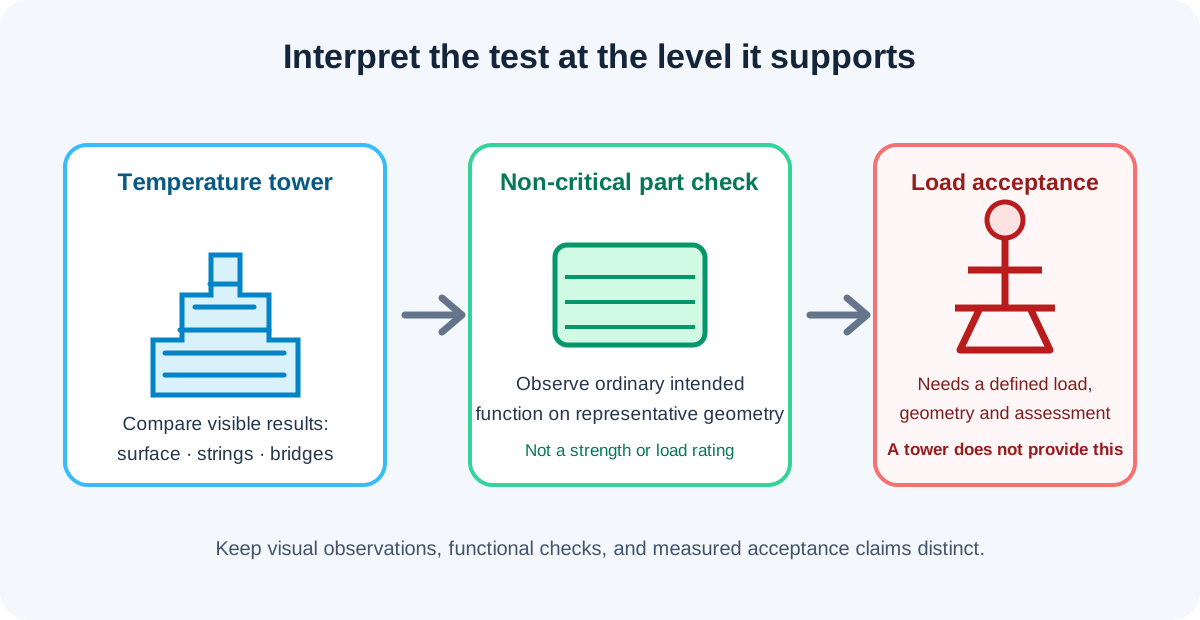
Use the tower to compare the properties you actually inspect, and assess any important finished-part property with a method suited to that part. For bridge, overhang, or short-layer cooling questions, use feature-specific calibration while keeping temperature fixed.
Verify before storing the value
Print a small representative part with the intended layer height, cooling, speed, and geometry. Prefer a part that exposes the property that matters: a functional fit for dimensions, a non-critical functional part used under its intended conditions to observe layer bonding (not a structural load test), or a travel-heavy model for oozing. If the result differs, investigate wet material, nozzle condition, flow, cooling, travel, and geometry before widening the temperature range again. Keep the provisional temperature in the exact material/nozzle/printer profile with its product, slicer version, plate, dry state, test object, date, and observations.
A temperature tower is not a substitute for material choice and care or stringing diagnosis . It is one controlled comparison; repeat it after a nozzle, material product, slicer process, major speed, cooling, enclosure, or firmware change when that change affects the test assumptions.
Back to top ↑