A first layer with gaps, ridges, drag marks, or curled corners does not identify one bad setting. Nozzle height, plate condition, mesh or leveling state, material, flow, temperature, speed, and the model’s footprint can produce similar pictures. Diagnose the pattern before changing a value.
Record the setup and symptom
Write down the printer and exact variant, firmware, nozzle diameter and wear, plate surface and profile, filament product and dry history, slicer and version, printer and filament profiles, first-layer height, temperatures, speed, cooling, and flow. Photograph the whole first layer and a close view of the defect. Note whether it is everywhere, limited to one side, repeated at the same coordinates, or confined to sharp corners.
| What you see | What it suggests, not what it proves |
|---|---|
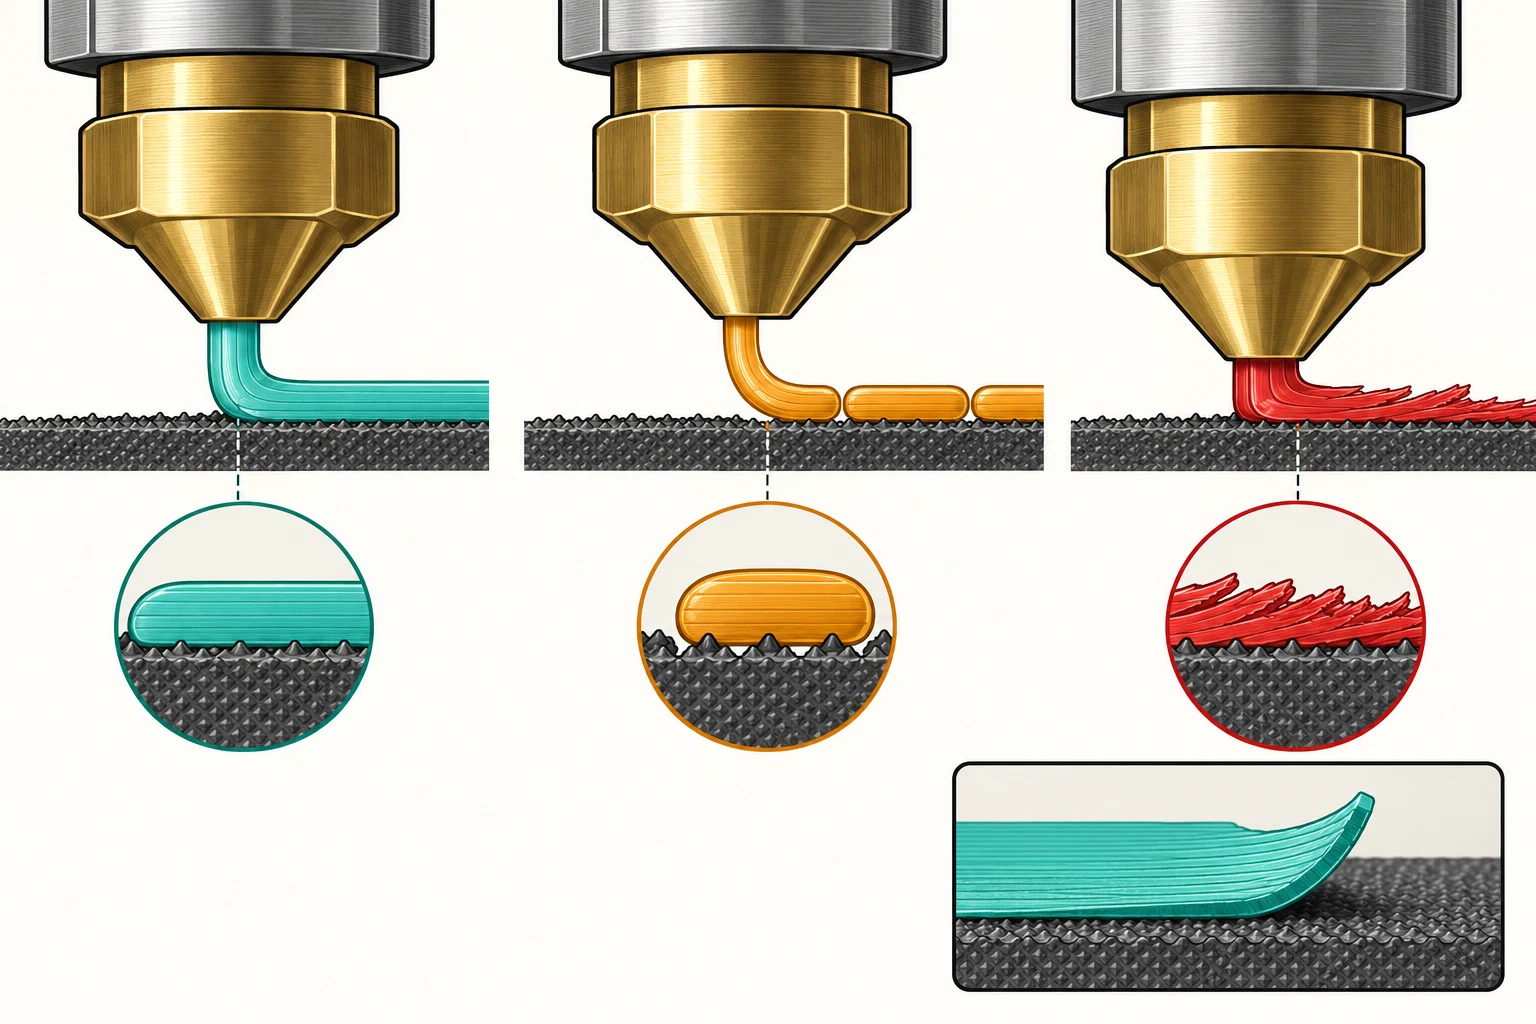
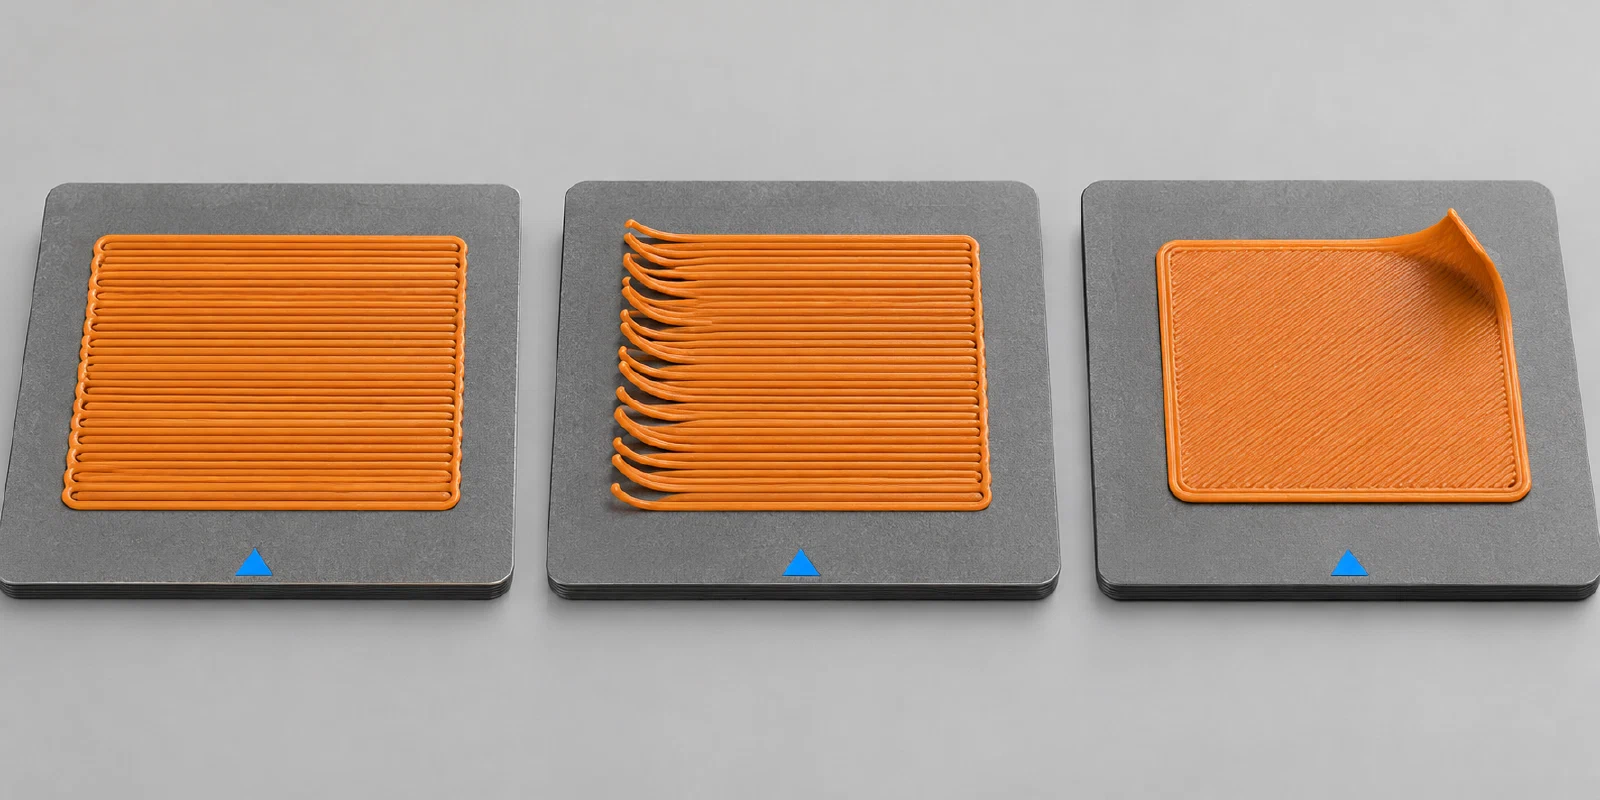
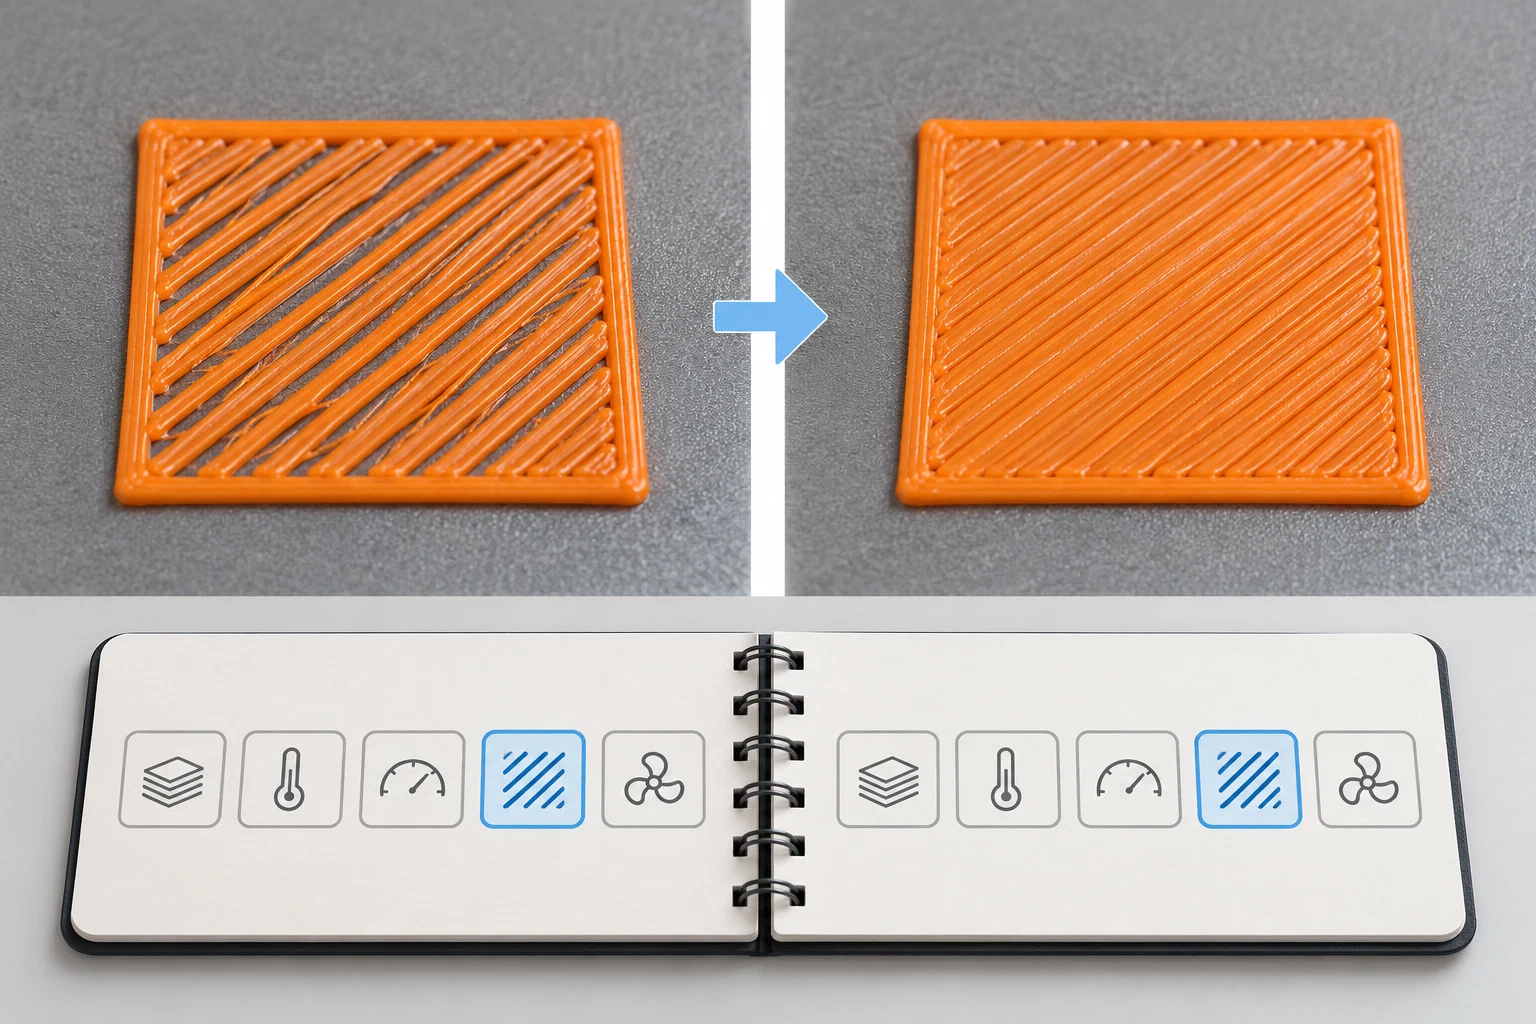
| Gaps between adjacent lines or isolated underfill | Nozzle may be too far from the surface, flow may be low, the surface may be uneven, or the material path may be inconsistent. |
| Broad ridges, translucent over-compression, or a nozzle dragging through lines | The nozzle may be too close, the mesh or plate may be wrong, or the first-layer flow may be excessive. |
| Defect concentrated on one side | Plate seating, leveling, gantry, probing, or a local surface problem deserves priority over a global slicer change. |
| Corners lifting while the center looks acceptable | Adhesion, footprint, material state, cooling, drafts, or geometry may be involved. |
| One edge or feature failing repeatedly | Check the model edge, support or brim choice, start-of-print path, and generated toolpath before assuming a bed-wide fault. |
Check physical causes first
- Confirm that the selected plate is installed in the orientation and position required by the printer. Remove fingerprints, loose debris, and excess residue using the plate maker’s procedure. Do not substitute a cleaning chemical or abrasive method without checking the plate instructions.
- With the printer in its safe inspection state, check for a loose plate, obstruction, damaged surface, nozzle contamination, or a carriage condition that prevents consistent motion. Do not touch hot or moving parts.
- Rerun the exact printer’s leveling, mesh, or first-layer calibration when its manufacturer calls for it. A Prusa MINI calibration sequence, for example, is a printer-specific procedure for judging the deposited line; it is not a Z-offset number to copy to another machine. Creality’s K2 Pro guidance likewise ties calibration choices to that model’s workflow and machine state.
- Check the material. Wet or degraded filament can worsen surface quality and adhesion, but a first-layer defect alone does not prove moisture. Use the filament maker’s drying limits and spool instructions rather than borrowing a recipe from another product.
Run controlled tests
After the physical checks, change one relevant variable and record the result. If the pattern is uniform and the printer’s calibration procedure permits it, use that procedure to test nozzle-to-surface distance. If the line is consistently underfilled, compare a small first-layer test with the same material and a known-good profile before adjusting flow. If the line is over-compressed, do not compensate by adding more flow or forcing the nozzle against the plate.
For corner curl, keep nozzle and bed conditions fixed while comparing a small footprint with the actual geometry. Then investigate plate preparation, material temperature range, cooling, airflow, and brim or orientation choices. A warped plate, damaged coating, wet material, or model edge can require a different route from a global height correction.
Separate a detached hotend blob from adhesion failure
A large blob of filament around a hotend is a different observation from a first layer lifting off the plate. Record where material first detached and whether the nozzle became wrapped before later layers failed. Creality’s K2 Plus guidance treats clumping as a model-specific condition with several possible contributors; it also includes hotend cleanup steps that are not portable. Do not improvise scraping or hot cleaning. Use current instructions for the exact printer or ask its manufacturer for service guidance. If the printer reports a probe, sheet, sensor, or other fault, capture the exact text and code and use printer fault codes and safety stops to match the reported state before rerunning calibration.
Bambu Lab’s H2C manual also distinguishes nozzle height that is too low, which can damage the plate, from height that is too high, which can reduce adhesion. That is an H2C-specific calibration warning, not an offset to copy. Follow the procedure for the exact machine and stop if the nozzle threatens the surface.
Verify before accepting the change
Repeat the same first-layer test with the same plate, material, and profile. Look for even line contact without open gaps, excessive ridges, scraping, or corner lift. Then print a small representative object and inspect adhesion and release after cooling. A single improved first layer does not prove that every geometry or material will behave the same way. If the nozzle threatens the plate, the bed heats abnormally, a collision occurs, or the required service step is unclear, stop and use the exact manufacturer procedure or route the issue to maintenance.
Back to top ↑