Nozzle diameter is a choice about the part, the material, the hotend, and the profile—not a simple speed selector. A smaller nozzle can represent finer XY features, while a larger nozzle can support wider lines and fewer passes. The result still depends on layer height, line width, volumetric flow, temperature, extrusion force, geometry, and the printer’s actual interface.
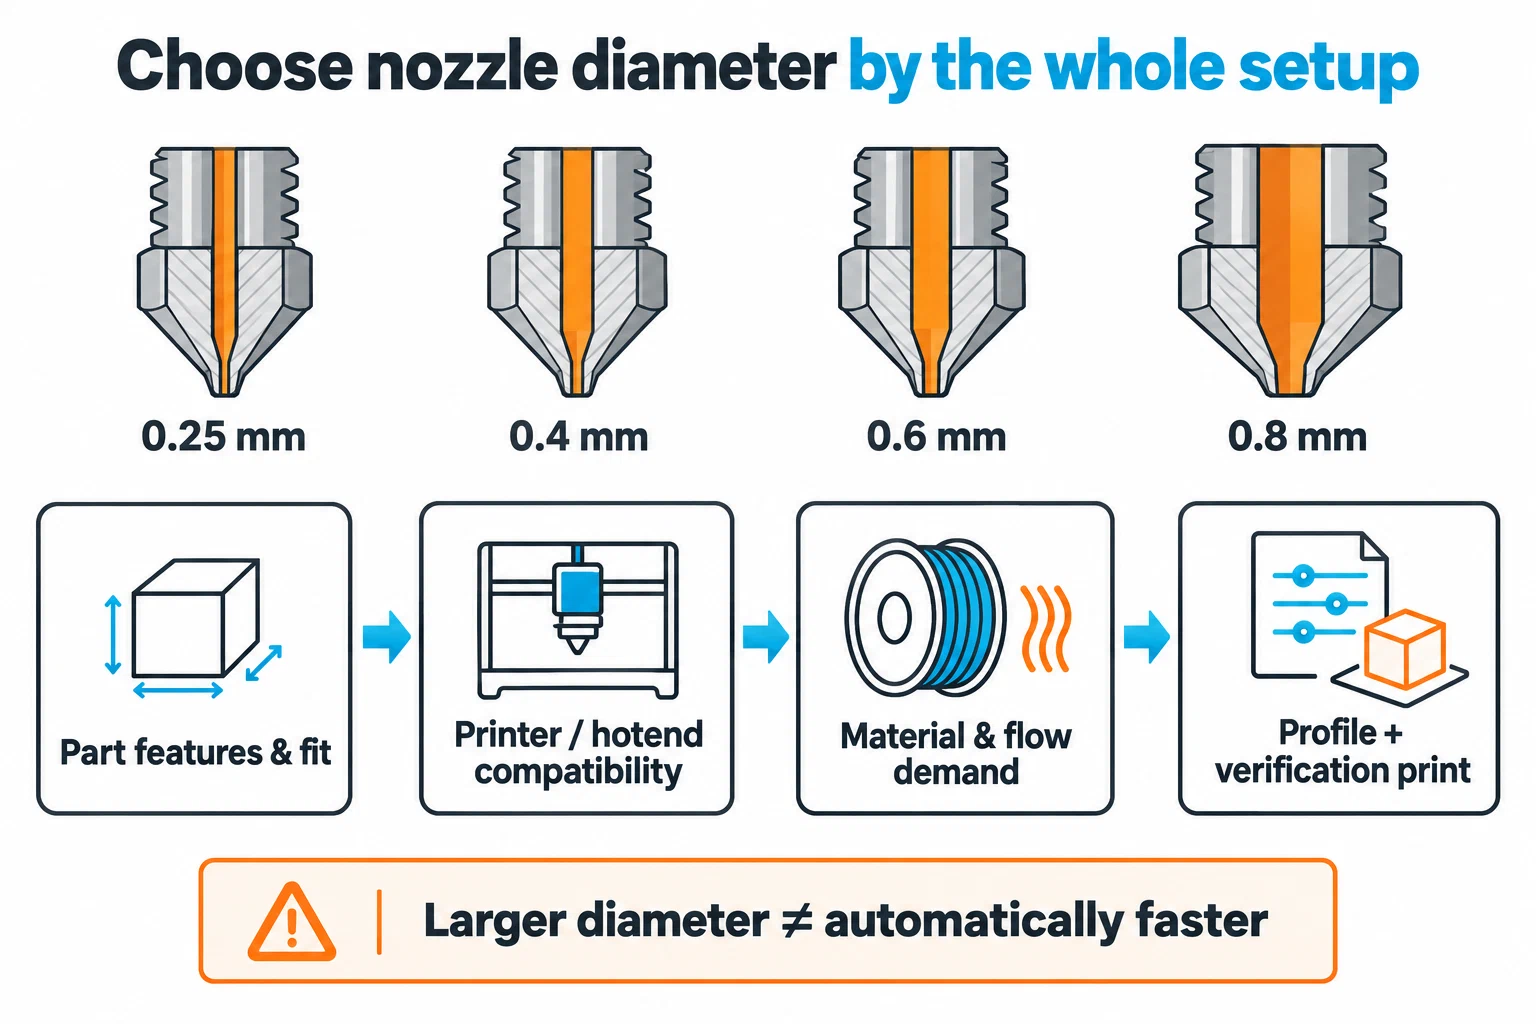
Start with the part and the material
Record these before comparing diameters:
- the exact printer and hotend or print-core family;
- the nozzle interface, material, geometry, and current wear state;
- the filament family, brand or product, filler, dry state, and feed path;
- the smallest important feature, wall thickness, text, hole, or clearance;
- the required surface finish, strength, throughput, and dimensional fit; and
- the slicer, version, printer preset, nozzle preset, and material/process preset.
Prusa’s Nextruder guidance lists roughly 0.25, 0.4, 0.6, and 0.8 mm choices for several common materials, but warns that a very small nozzle can be problematic with flexible filament and unsuitable for composites in that context. The listed options are not a cross-brand compatibility table. A Bambu Lab A1 product page likewise lists its own nozzle options and installed nozzle as a model-specific capability statement, not as evidence that an arbitrary replacement will fit another printer.
A practical comparison
| Diameter | Useful starting question | Main trade-off to verify |
|---|---|---|
| 0.25 mm | Do fine text, small openings, or thin visible features justify slower, more sensitive printing? | Higher pressure, possible flexible-filament difficulty, and greater clog sensitivity can outweigh the detail benefit. |
| 0.4 mm | Is this the documented, general-purpose setup for the printer and material? | It is a baseline, not proof that one profile works for every product or geometry. |
| 0.6 mm | Would wider lines reduce wall count or make a practical part easier to print? | Detail, bridge behavior, flow demand, and the printer’s hotend limit still need checking. |
| 0.8 mm | Is throughput or a robust large feature more important than fine surface detail? | Wider lines and larger extrusion demand may require a different profile, temperature, and test strategy. |
A larger nozzle is not automatically faster. E3D’s flow guidance describes achievable volumetric flow as dependent on line width, layer height, print temperature, extrusion force, hotend, printer, and filament. Treat any flow value as a setup-specific starting point, not a multiplier that can be transferred by diameter alone.
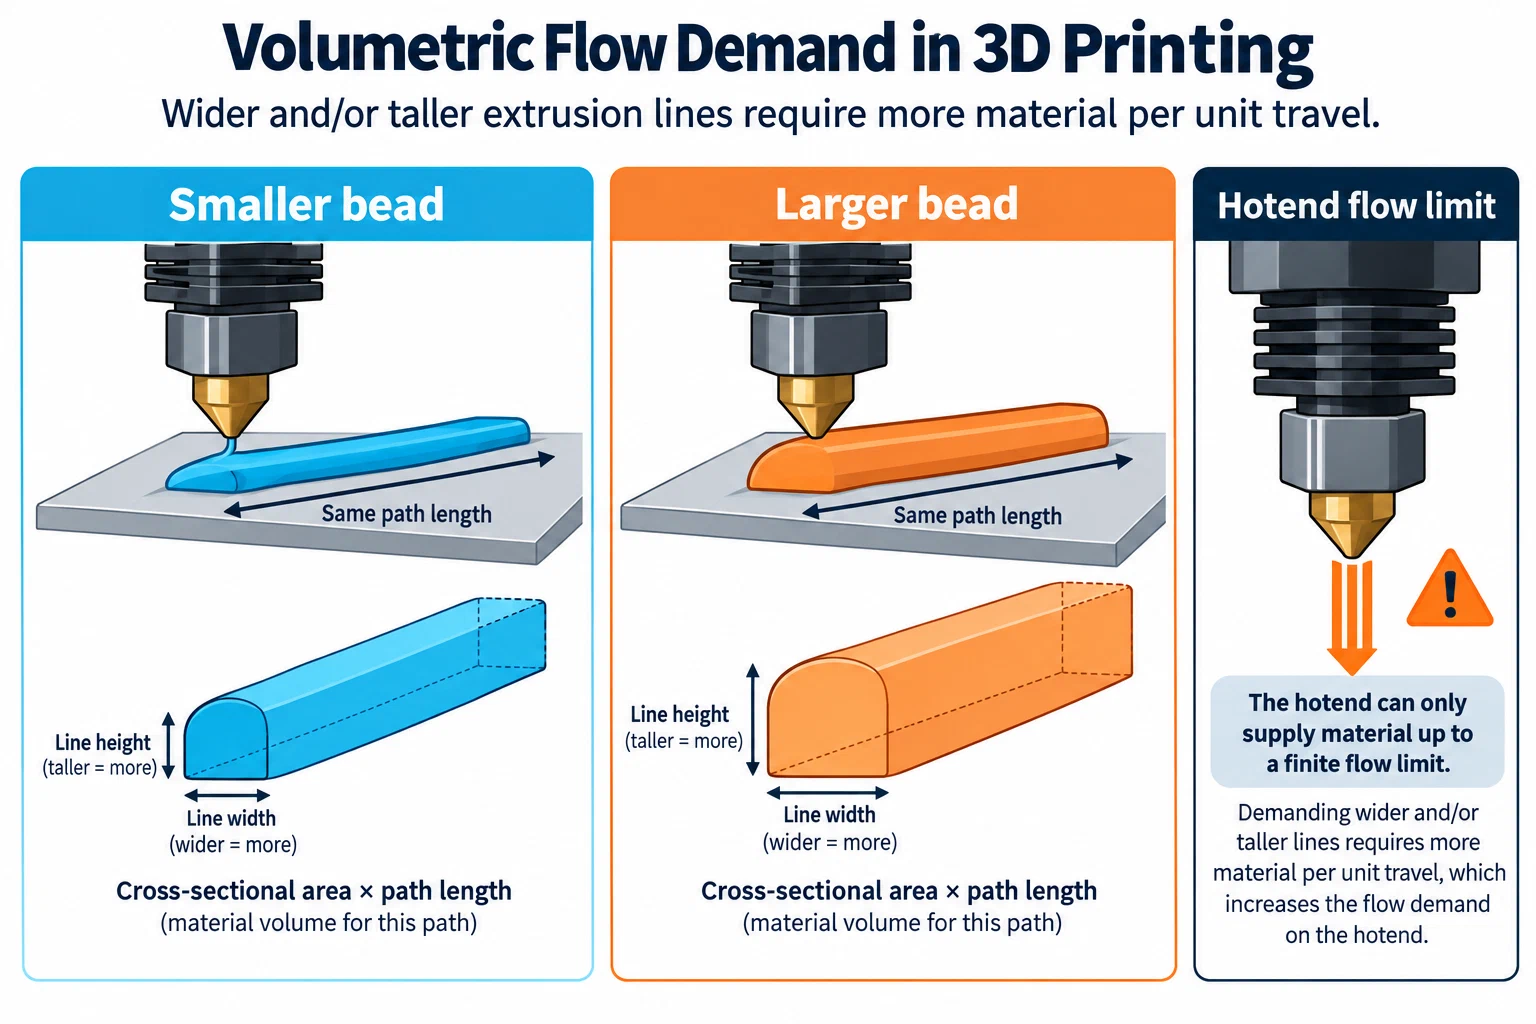
Use a model-specific compatibility card
Some ecosystems expose useful boundaries that should travel with the printer identity. Bambu’s H2D specification lists 0.2, 0.4, 0.6, and 0.8 mm nozzles, but its 40 mm³/s standard-hotend figure is tied to a named material, temperature, geometry, and test. The H2D hotend documentation also says its dual-nozzle setup uses the same nozzle type and size, warns that particulate filled filament can clog a 0.2 mm nozzle, and recommends a hardened 0.6 mm nozzle for carbon- or glass-fiber filament in that product context. Record those as H2D constraints, not portable rules.
After service, the check may be more than selecting a diameter. A Creality K2 Pro replacement procedure includes smooth extrusion followed by the printer’s Input Shaping and Auto Leveling checks. Other machines use a complete hotend or adapter-specific procedure. Confirm the exact replacement part and follow that model’s service documentation before treating a new diameter as ready for a profile.
The H2C manual separates its built-in left 0.4 mm hardened-steel hotend from the right induction hotend. Its material table routes PET-CF, PPA-CF, and PPS-CF to the left hotend; TPU 95A HF to the right; and TPU 85A to a right-side 0.6 mm hotend with direct feeding. The manual’s supported-size list is not the same as its included-accessory list, and the material rows narrow the choices. The cited manual identifies itself as Version 1.0 (2026.01) but does not specify a firmware revision. It directs readers to the H2C Firmware Release History for firmware details and says that history takes precedence if it conflicts with the manual. Check the release history for current guidance before ordering or loading a profile.
Nozzle architecture also changes what the diameter choice means. Snapmaker’s
U1 FAQ describes a proprietary integrated hotend whose nozzle is not replaced
separately. Its Liber high-flow guidance excludes CF-, GF-, and wood-filled
filament and TPU from high-flow use, and requires a common nozzle diameter
across hotends in one print job. On the X2D, the version 1.0 manual describes
separate main and auxiliary paths and applies to firmware 01.01.00.00; later
release notes take precedence if they conflict. These are model instructions,
not transferable size or feed rules.
Check layer height and profile coupling
Nozzle diameter controls much of the slicer’s XY feature resolution; layer height primarily affects vertical resolution and visible layer steps. PrusaSlicer guidance says layer height should generally remain below 80% of nozzle diameter and cannot exceed the nozzle diameter in that software. That is a PrusaSlicer constraint, not a universal quality law for every slicer, printer, material, or shape.
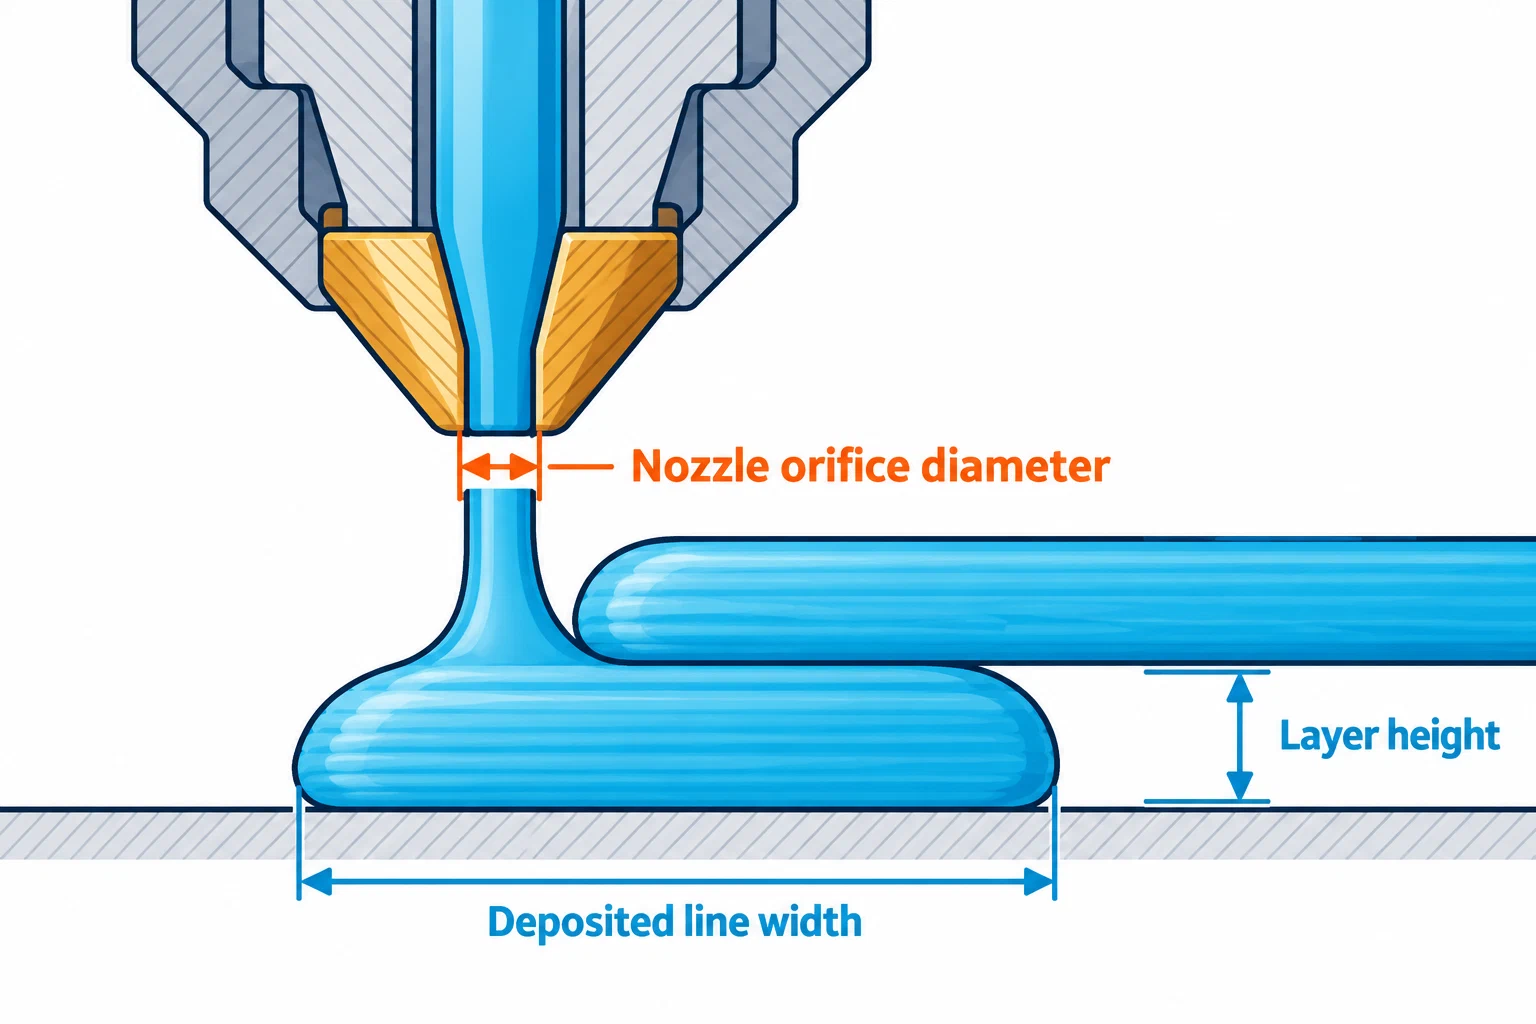
After a change, select or create the profile for the exact printer model and diameter. Check line widths, layer heights, first-layer settings, temperature, cooling, maximum volumetric speed, retraction, pressure control, and any printer-side nozzle selection. On a multi-tool or model-specific system, also check tool identity and offset state. Do not reuse stored G-code simply because the filename still names the same printer.
Verify the choice
- Confirm the nozzle and hotend interface from the printer or component documentation before installation.
- Load a profile bound to the exact diameter and record which values changed.
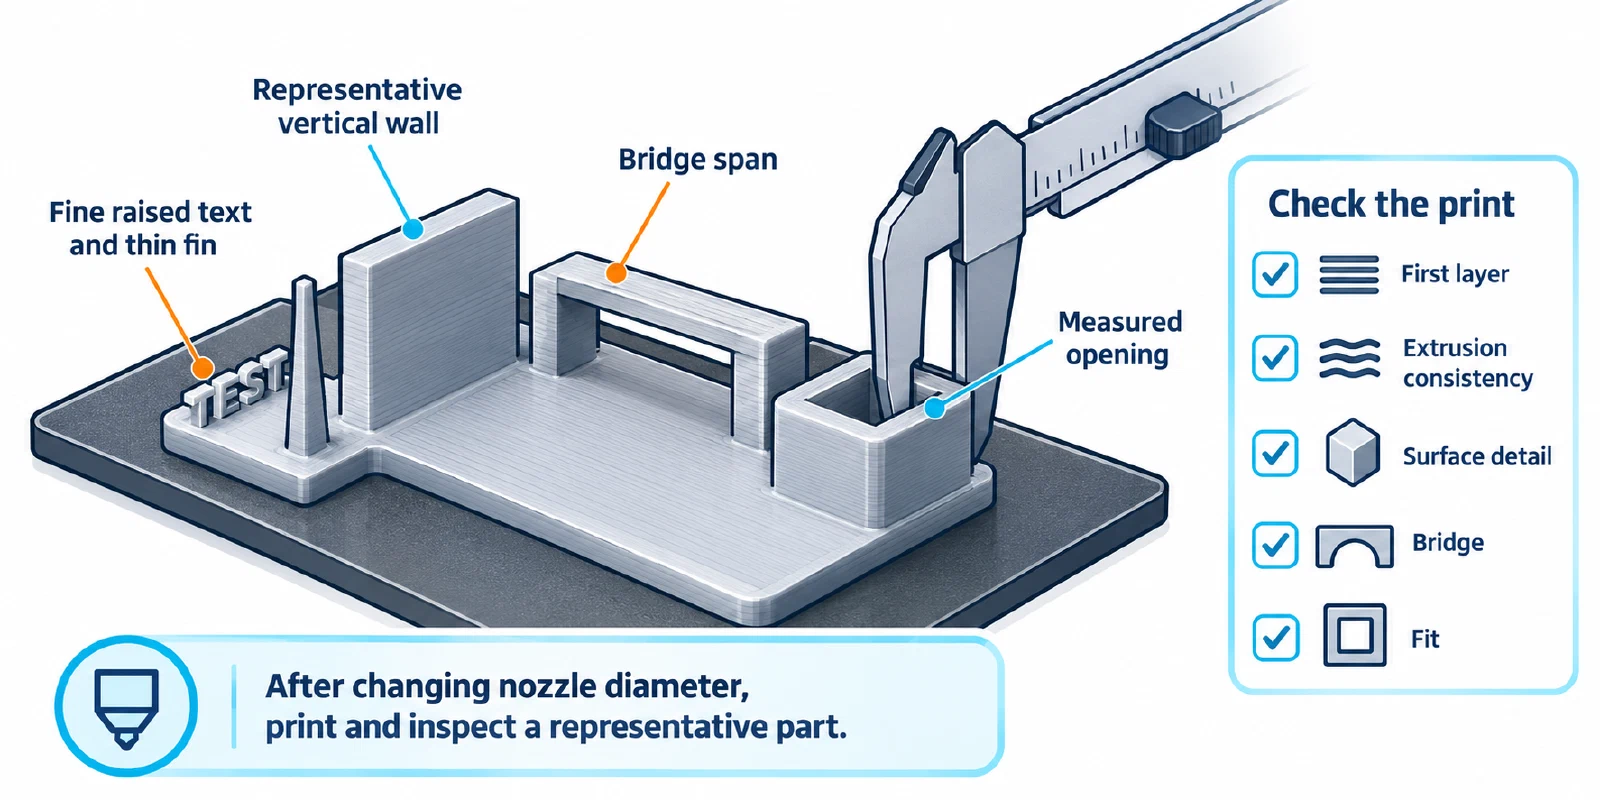
- Print a small model with fine features, a representative wall, and a measured opening or fit.
- Check first-layer coverage, extrusion consistency, surface detail, bridges, dimensional fit, and any signs of excessive pressure or clogging.
- Change one major process variable at a time and save the result with printer, material product, plate, slicer version, nozzle, and dry-state context.
For an abrasive composite, use the material-specific hardware guidance in Brass versus hardened nozzles for abrasive composites . If the swap changes the process enough to invalidate the old values, continue with Adapt a profile after a hardware or firmware change and a controlled calibration rather than guessing from diameter alone.
For adapter, integrated-hotend, or coordinated-upgrade fit before purchase, use Checking hotend and extruder compatibility .
Back to top ↑