A failed tool change is a stopped sequence, not a diagnosis. The same visible symptom can come from a wrong map, a damaged filament tip, moisture, a blocked PTFE route, a sensor-state mismatch, a profile command, or a hardware fault. Capture the state before clearing the error so the next test can distinguish causes instead of erasing the clue.
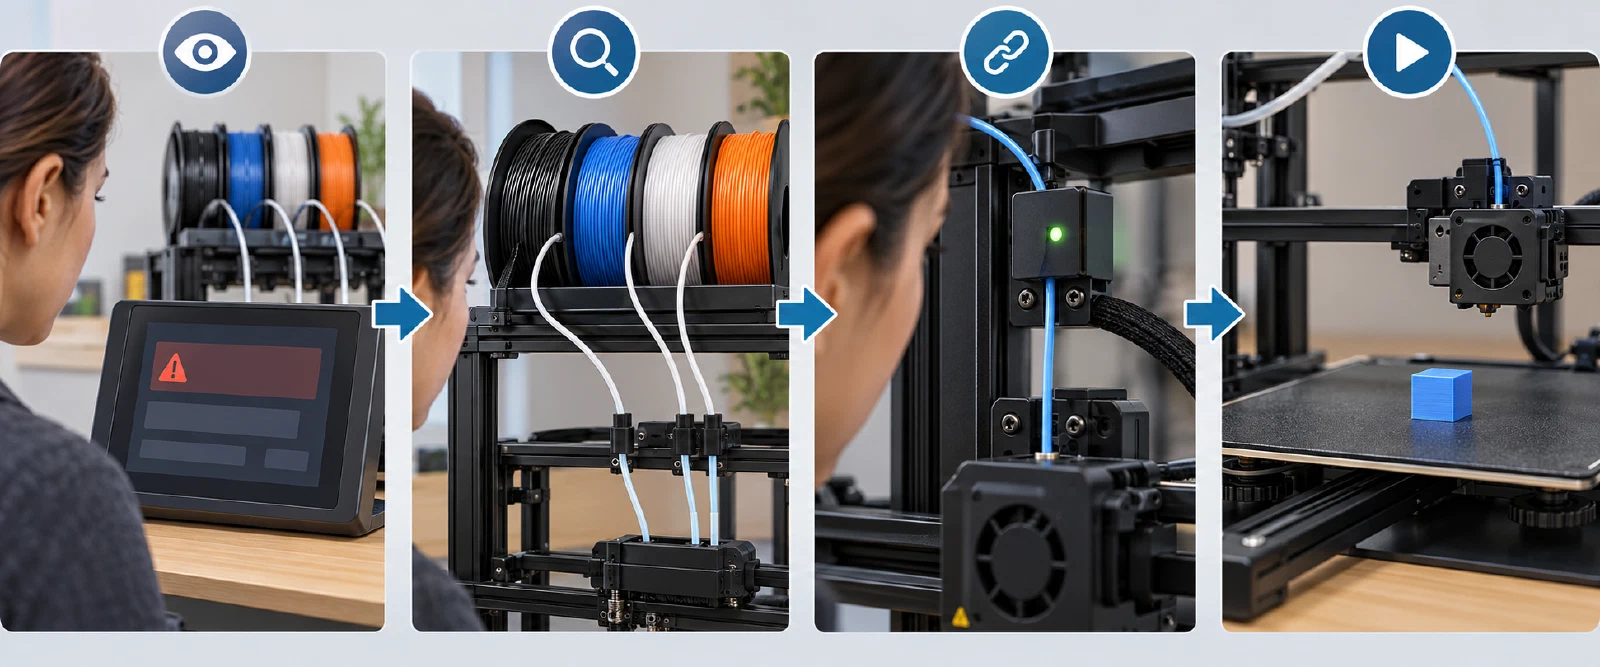
Freeze the evidence first
Record the printer and feeder or tool-changing system, exact variant and generation, firmware versions, slicer and profile release, material and product, slot or tool, nozzle, plate, dry state, displayed error or LED pattern, and the point where the sequence stopped:
- spool or inlet detection;
- loading through a buffer, hub, selector, or feeder;
- cutter or tip formation;
- sensor confirmation;
- extruder or nozzle arrival;
- unload, park, dock, purge, wipe, or resume.
Save the sliced file or profile name and note the last successful change. An LED or internal “loaded” record is a clue, not proof of the filament’s physical position. Prusa’s MMU3 status guidance, for example, directs readers to the printer error for diagnosis; its LED meanings are firmware-scoped and differ from older MMU behavior.
Work from least invasive to most specific
- Check the job map. Compare the requested tool or filament with the physical slot, printer-side map, and material actually loaded. Inspect the sliced preview. Do not assume a slot number or T-code means the same thing on another system.
- Check the obvious path. Look for an empty spool, tangled filament, a tight spool edge, a kinked or worn PTFE tube, a wrong buffer or hub route, a selector obstruction, a cutter issue, or a filament tip that cannot pass the next opening. Do not force filament through resistance.
- Check material state. Confirm product identity, diameter, dry state, brittleness or flexibility, and the feeder’s documented material boundary. A change failure can be a material or tip-formation problem rather than a motor failure.
- Check the state signals. Compare sensor readings, LEDs, printer messages, and the system’s internal loaded record. A state mismatch needs the named manufacturer branch; resetting a state without recording it can hide the cause.
- Check the profile and version boundary. Compare printer and feeder firmware, tool count, hardware revision, slicer mode, tool-change commands, purge or handoff controls, and profile provenance. Revert to a known compatible configuration only through the system’s documented process.
- Enter a hardware or service branch only when indicated. A motor, cutter, dock, board, cable, thermal, or overcurrent message needs the exact model’s service procedure. Stop, isolate power, cool hot parts, and escalate when the manual requires it.
Use error-specific branches, not a universal checklist
Prusa’s error #04108 is a useful example: the documented load-to-extruder check and its printer-family branches lead to sensor calibration, extruder, clog, spool/buffer, PTFE, and filament-tip checks. Errors #04104, #04106, and #04506 represent different sensor or state boundaries, so they should not be collapsed into one “recalibrate everything” step. The MMU3 setup guide also gives model-specific inspection and small adjustment guidance for the tip and path; its values do not transfer to an AMS, IDEX, or another feeder.
Other systems need their own branches. A Prusa XL tool-changer fault can require the manufacturer’s dock, coupler, belt, calibration, and board checks. Creality CFS-C documentation separates long-string and jam branches and treats cutter and PTFE service as CFS-C-specific. Flashforge AD5X installation ties holder, position, and configured channel numbers together. These examples show why the exact system and error remain part of the diagnosis.
For Creality K2 Plus runout, keep the source, sensor stage, and displayed continuation separate: the guide describes different behavior depending on whether filament has passed the CFS outlet, and a Retry action is not evidence that filament reached the extruder or that the resumed print is sound. The K2-series jam guide separates extruder/heat-break, gear, and buffer branches; follow the current procedure for the exact model and stop when it enters hot-part or disassembly work. This page does not reproduce those service steps or claim a repair result.
Snapmaker U1: separate loading stage from error classification
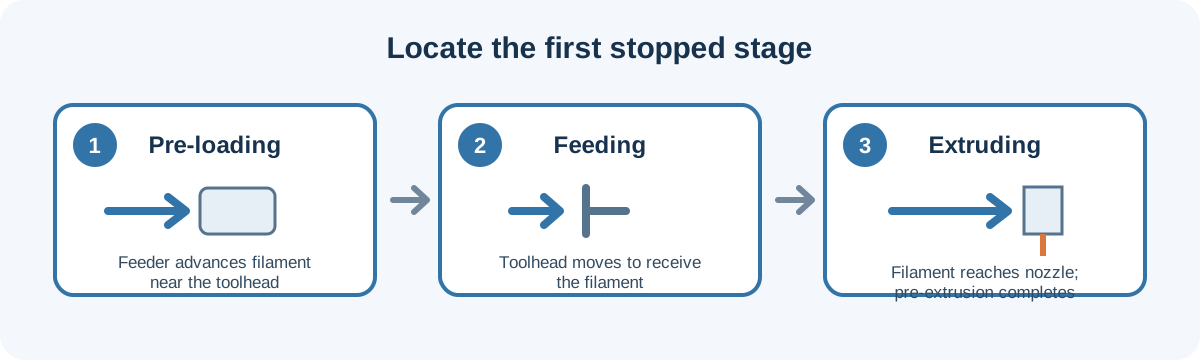
For a U1 automatic-load problem, first record whether it stopped during pre-loading (the feeder advances filament toward, but not into, the toolhead), feeding (the toolhead moves to receive it), or extruding (filament reaches the nozzle but pre-extrusion does not finish). The indicator and full displayed code help select the matching branch; neither confirms a root cause. Snapmaker’s automatic-loading guide lists separate residual-filament and feeder-speed checks during pre-loading, a tube and filament-tip check for a cited feeding-stage code, and a separate nozzle-clog path for one extrusion-stage code. Follow the current page for the exact head and state rather than transferring one code to all four heads.
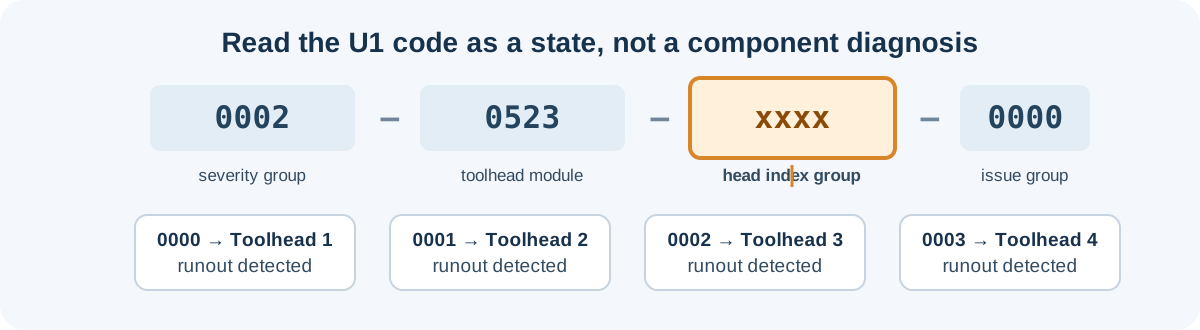
Snapmaker formats U1 codes as severity, main module, submodule, and issue
groups. In its table, 0523 is the toolhead module and 0525 is the filament
feeder module. The four 0002-0523-xxxx-0000 rows identify the corresponding
Toolhead 1–4 runout state. Treat the leading severity as the vendor’s
classification of notice, warning, or error; the documentation cautions that
a code may not identify the actual fault. Record the complete code, affected
head, indicator, and physical filament position before following the linked
branch.
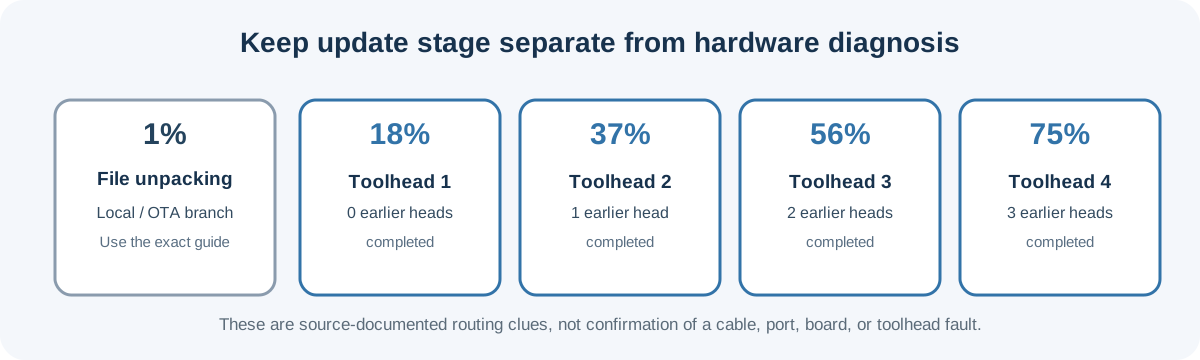
If the stopped operation is a firmware update, preserve its progress stage and whether it was an over-the-air (OTA) or local update. Snapmaker classifies 1% as a file-unpacking failure; handling then differs by route: its local USB branch covers file and USB preparation, while an OTA unpack failure routes to support. The 18%, 37%, 56%, and 75% checkpoints map to sequential toolhead-update states, and other stages route to support. Its table maps those four checkpoints to the head that failed; a percentage does not diagnose a bad cable or board. Cable, connector, and board checks belong to the complete current U1 update-failure procedure , which includes physical service work. Use Snapmaker support if its exact branch does not resolve the issue. The separate V1.1.1 release note lists minimum companion software versions and runout-resume changes; verify the installed versions before applying that release-specific behavior.
Change one variable, then verify
After the manufacturer’s immediate recovery step, test the smallest useful operation: one load, one unload, one tool change, or a short test object. Keep the same material, map, profile, and hardware while testing one correction. Record whether the failure moved to another slot, occurred at the same stage, changed with the material, or disappeared only after a reset. A successful retry is not proof that the underlying cause is gone; repeat enough controlled changes to establish the result for the named setup.
Stop rather than improvise when filament is trapped in a hotend, a tool is not parked, a motor or power fault is displayed, a cutter or blade is exposed, or the next step requires disassembly not covered by the current manual. Do not bypass sensors, continue through an unresolved collision warning, or apply another system’s recovery order. Once the failure is understood, update the mapping record , purge and support choices , or compatibility record with the observed firmware, profile, material, and verification result.
Back to top ↑