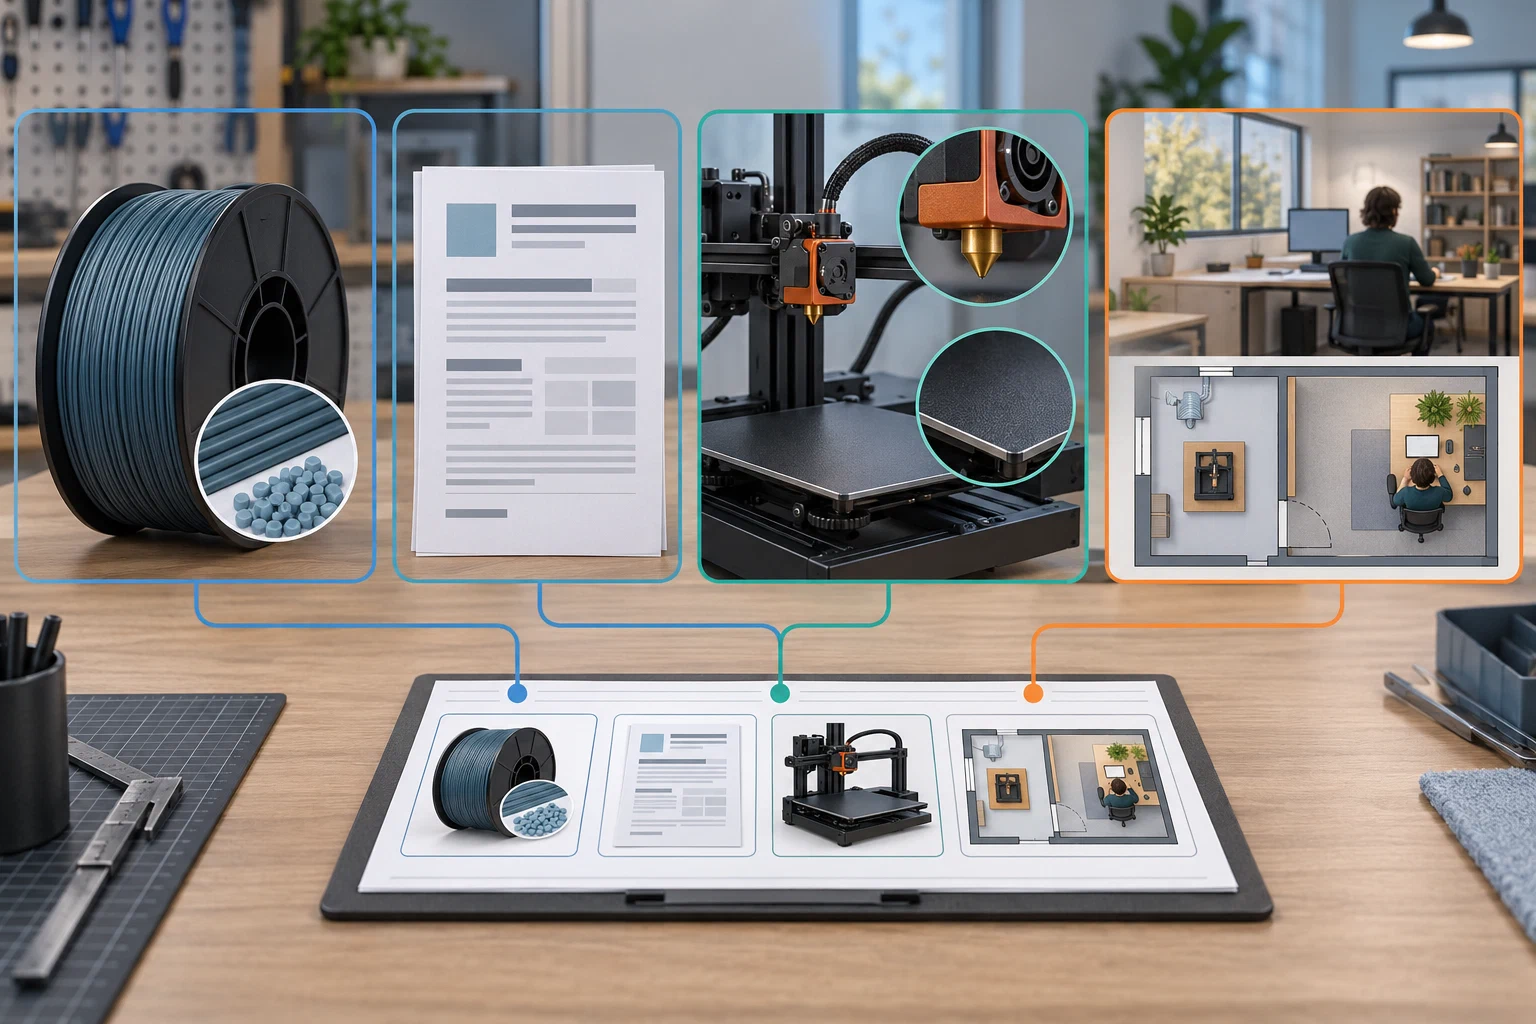
“PLA,” “PETG,” “ABS,” and “nylon” are material families, not complete safety identities. Record the manufacturer, product name, color, additives or filler, diameter, lot if available, SDS revision and region, printer and exact variant, firmware, nozzle material and diameter, plate, slicer release and selected material profile, process temperature, enclosure state, room occupancy, and dry or wet history. Those details determine which evidence can be transferred and which must remain unknown.
Separate three different kinds of evidence
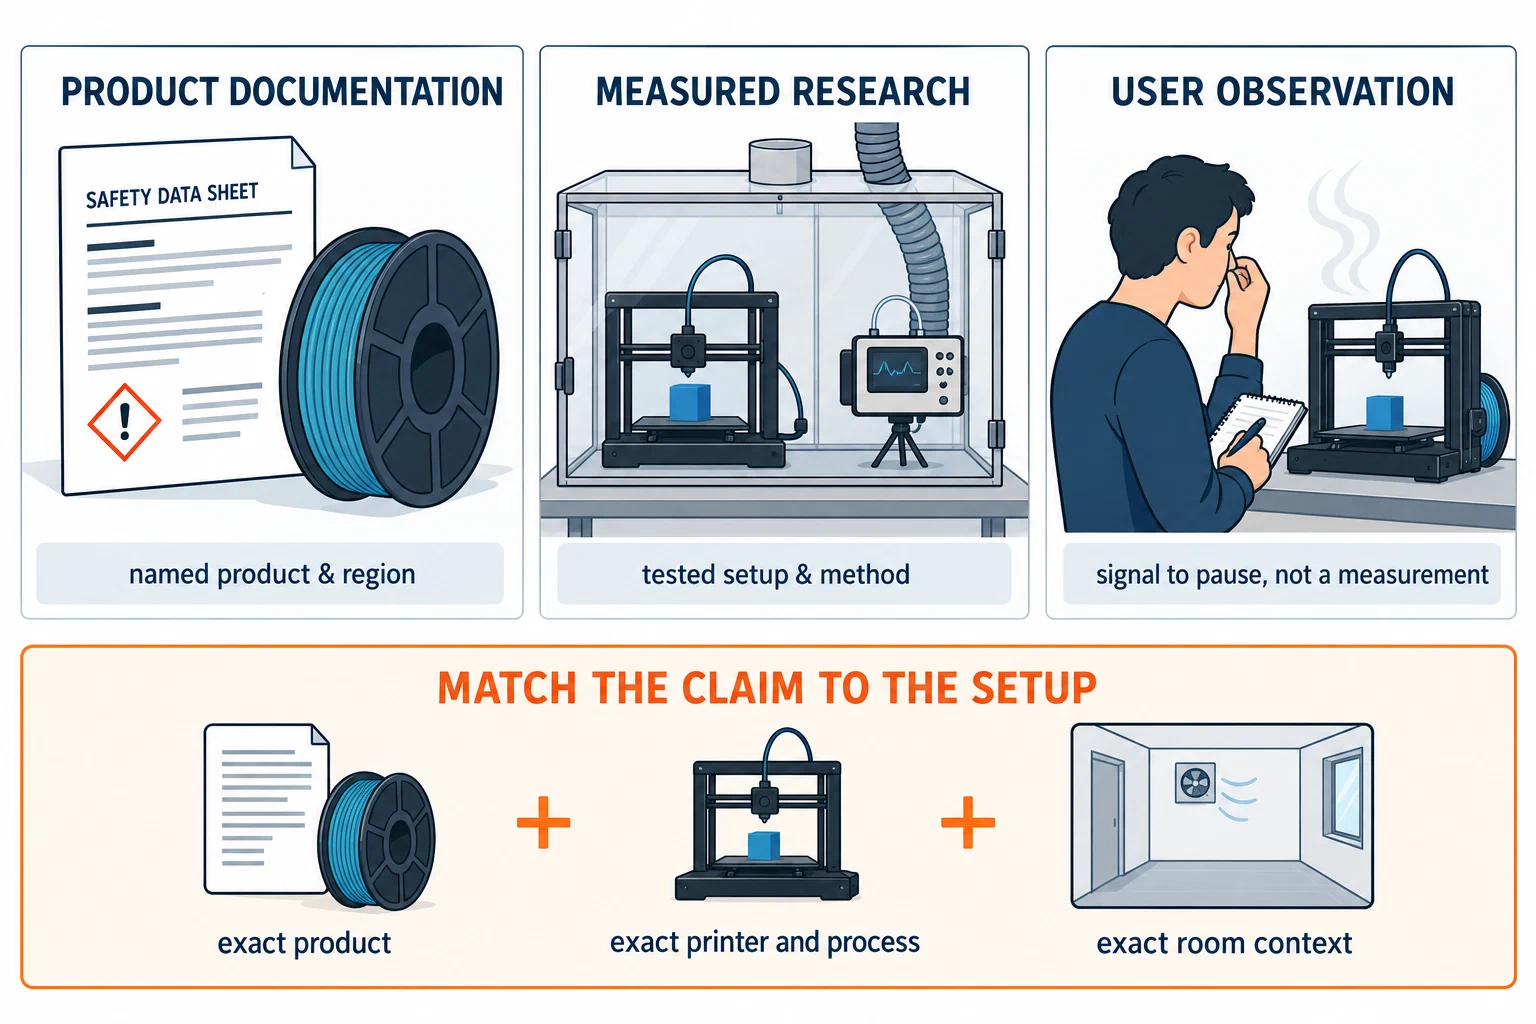
A material decision becomes clearer when these statements are kept apart:
- Product documentation: An SDS may describe storage, spill, ignition, combustion products, and occupational-hygiene practices for one named product. For example, the Polymaker PLA Pro Australia SDS says to keep the product dry, cool, closed, and ventilated, avoid dust or vapors during a release, remove ignition sources during a spill, and recognize carbon oxides as hazardous combustion products. It does not measure printer emissions or certify every PLA product.
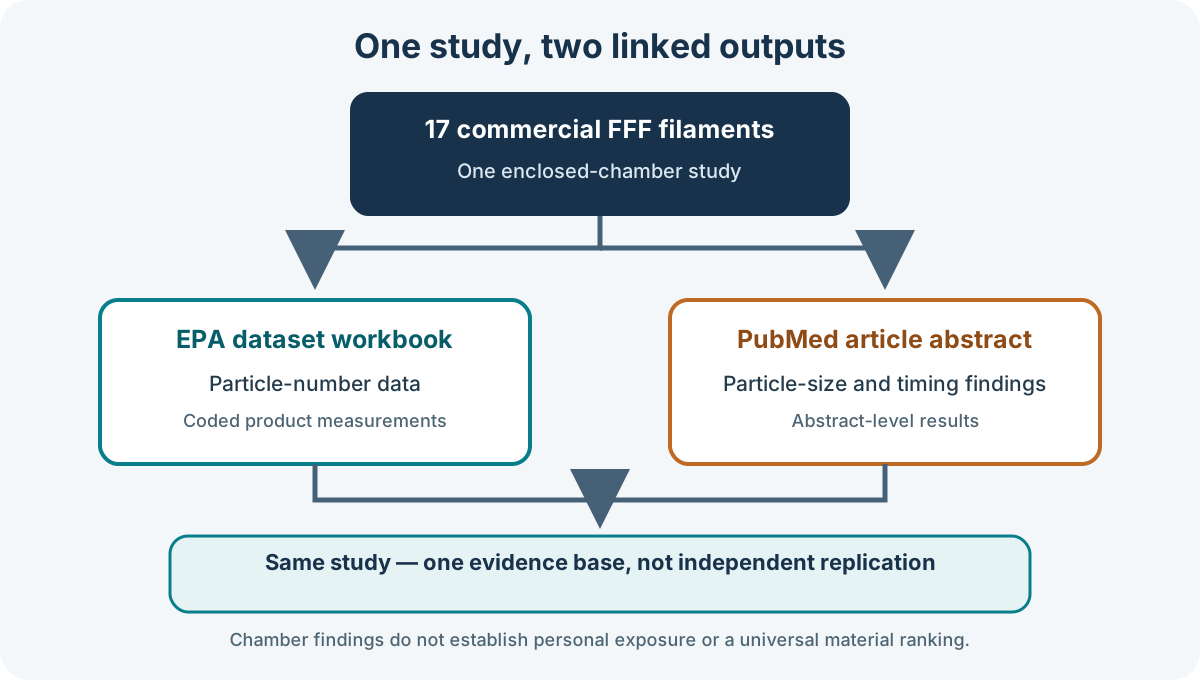
- Measured research: NIOSH reports that emissions vary with material, coloration, extruder temperature, printer, room, and control. Its office study found lower particle emissions for one evaluated orange PLA than two evaluated materials, but explicitly did not establish a general PLA-versus-ABS ranking. A newer indexed study of 17 commercial filaments reported the highest average particle-number concentrations among its tested ABS group, followed by metal-containing PLA, PLA, and PC groups in an enclosed chamber. That abstract is a comparison of tested products and methods, not an exposure limit or a universal material order.
- User observation: Odor, visible smoke, haze, irritation, or a change after adding an enclosure are observations that should change what you do next. They do not identify the substance concentration, prove that no emission exists when odor is absent, or create a universal hazard ranking. Treat persistent or unexpected symptoms as a reason to leave the area and seek appropriate local or medical advice; this article is not medical guidance.
The associated EPA dataset and PubMed abstract report different outputs from the same study; they are not independent replications.
An SDS that says a product is not classified under a named system is not the same as “no emissions,” and a product that has a flammability or material certificate is not a certification of a printed geometry, assembly, or room.
Check the scope of a fire or safety claim
A material rating, a test on a printed specimen, printer safeguards, and approval for an end use answer different questions. Read the actual listing or report and match it to the claim being made.
| Record | Check in the source | It does not establish |
|---|---|---|
| A molded-material rating | Whether the rating covers the molded material or an additive-manufacturing designation, and which test method and grade it names | The same rating for a printed filament, part, assembly, printer, or workspace |
| An additive-manufacturing material listing | Exact material grade, printer and processing designation, and which properties were evaluated and published | Approval of an arbitrary printed part or its intended application |
| A printed-part fire test | Material, specimen geometry and thickness, print parameters, test method, and the product scope the test addresses | A fire rating for other designs or materials, printer fire protection, or household workshop approval |
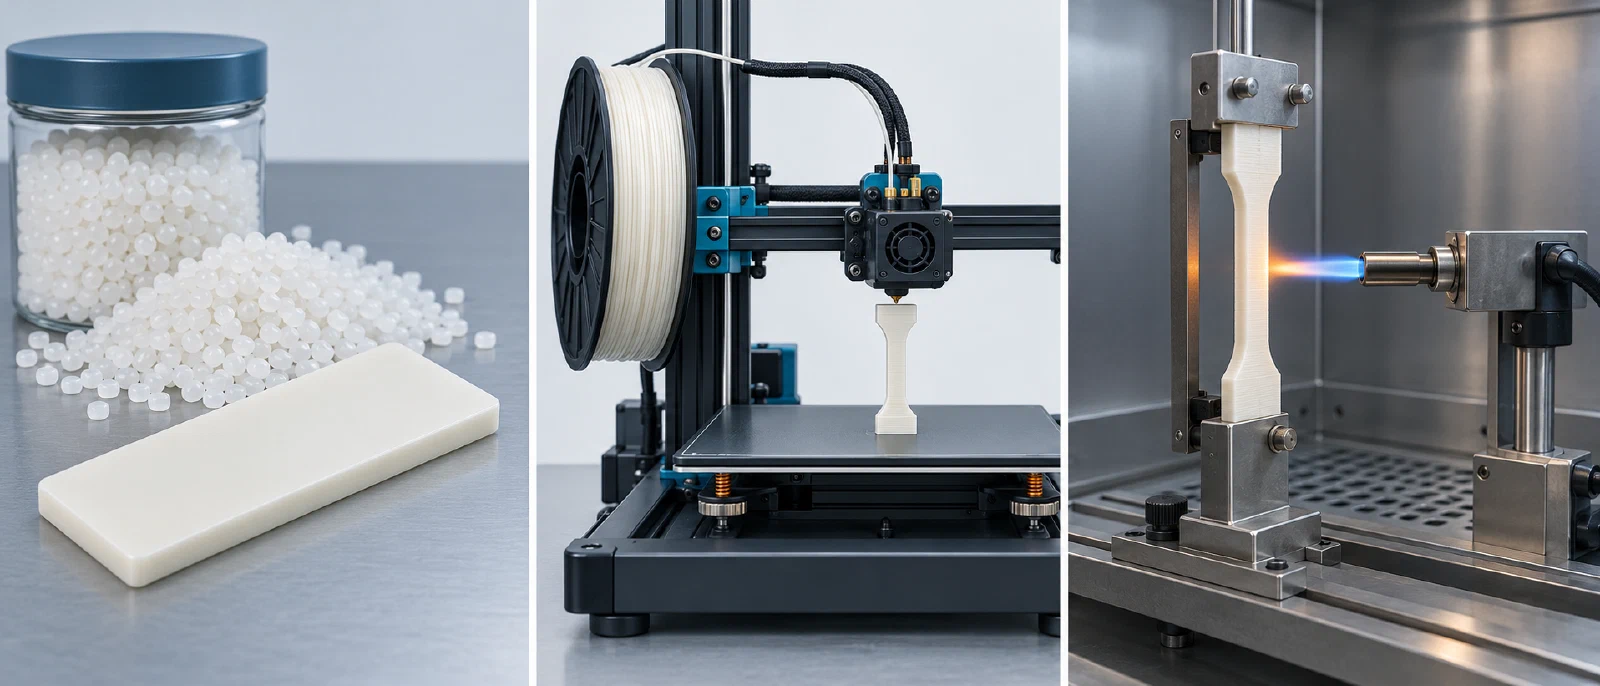
UL Solutions says an additive-manufacturing material designation can depend on the printer and processing parameters. It also explains that a property missing from a listing may not have been evaluated or may not have been published. A molded-material rating does not transfer automatically to additive-manufactured material. Check the UL additive-manufacturing FAQ and the actual record rather than relying on a shorthand product claim.
The CPSC staff lifecycle report concerns selected printed children’s-product designs and states that it was not reviewed or approved by the Commission. The FAA technical report examines selected FFF samples using an aircraft-cabin test method and says it does not constitute FAA policy. Neither report is a general household fire assessment. For printer operation, return to the exact printer manual and local requirements; for a particular finishing task, use workshop controls for finishing FFF parts .
Use a material-to-workspace record
Complete this record before moving a new product into a shared or occupied workspace:
| Field | Record | Why it changes the decision |
|---|---|---|
| Product identity | Maker, product, color, additives/filler, SDS revision and region | Similar family names can hide different formulations and instructions |
| Process | Printer/variant, firmware, nozzle material and diameter, plate, slicer/version, material profile, temperature, duration | Emissions and hot-work controls depend on the actual process |
| Material state | Drying method, temperature and time from the product instructions, storage container, wet-history | Moisture can change quality, purging, odor, and failure behavior |
| Workspace | Home, school, library, or makerspace; room occupancy; adjacent spaces; enclosure and exhaust state | A control tested in one room does not certify another |
| Handling | Spool storage, scrap, spill or dust response, waste route, and who is trained | Storage and waste decisions belong to the exact product and local rules |
| Verification | First test, abnormal observations, filter or exhaust check, and stop decision | “Loaded successfully” is not evidence of a suitable workspace |
Read the exact product SDS and manufacturer instructions. Keep spools closed and dry as directed, separate material from food and incompatible products, control scraps and dust, and do not use compressed air or dry sweeping to redistribute contamination where agency guidance calls for wet wiping or HEPA-filtered vacuuming. If a product has a filler, follow the abrasive composite filament guidance for nozzle, feeder, plate, and dry-state checks as a separate hardware decision.
Connect material to controls
Higher process temperature, a filled or colored formulation, a long print, a failed print, an enclosure, and a crowded room can change the control question. Start with source reduction and the printer maker’s enclosure or ventilation instructions. Then evaluate local capture, filter targets, room ventilation, occupancy, and maintenance together; a particle filter does not automatically capture gases or vapors, and a fan does not prove capture. Use ventilation and local controls for that room decision.
Stop the job and move people away from the printer if you see smoke, flame, uncontrolled heating, a jam with abnormal buildup, damaged wiring, a leaking or unidentified liquid, or a failed ventilation or enclosure component. Do not remove a cover or open a printer while it is hot or emitting material unless the exact manual and local emergency plan make that action appropriate. For a failed extrusion, route to under-extrusion, clogs, and heat creep rather than raising temperature blindly. For hot, electrical, or fire boundaries, use workshop housekeeping controls .
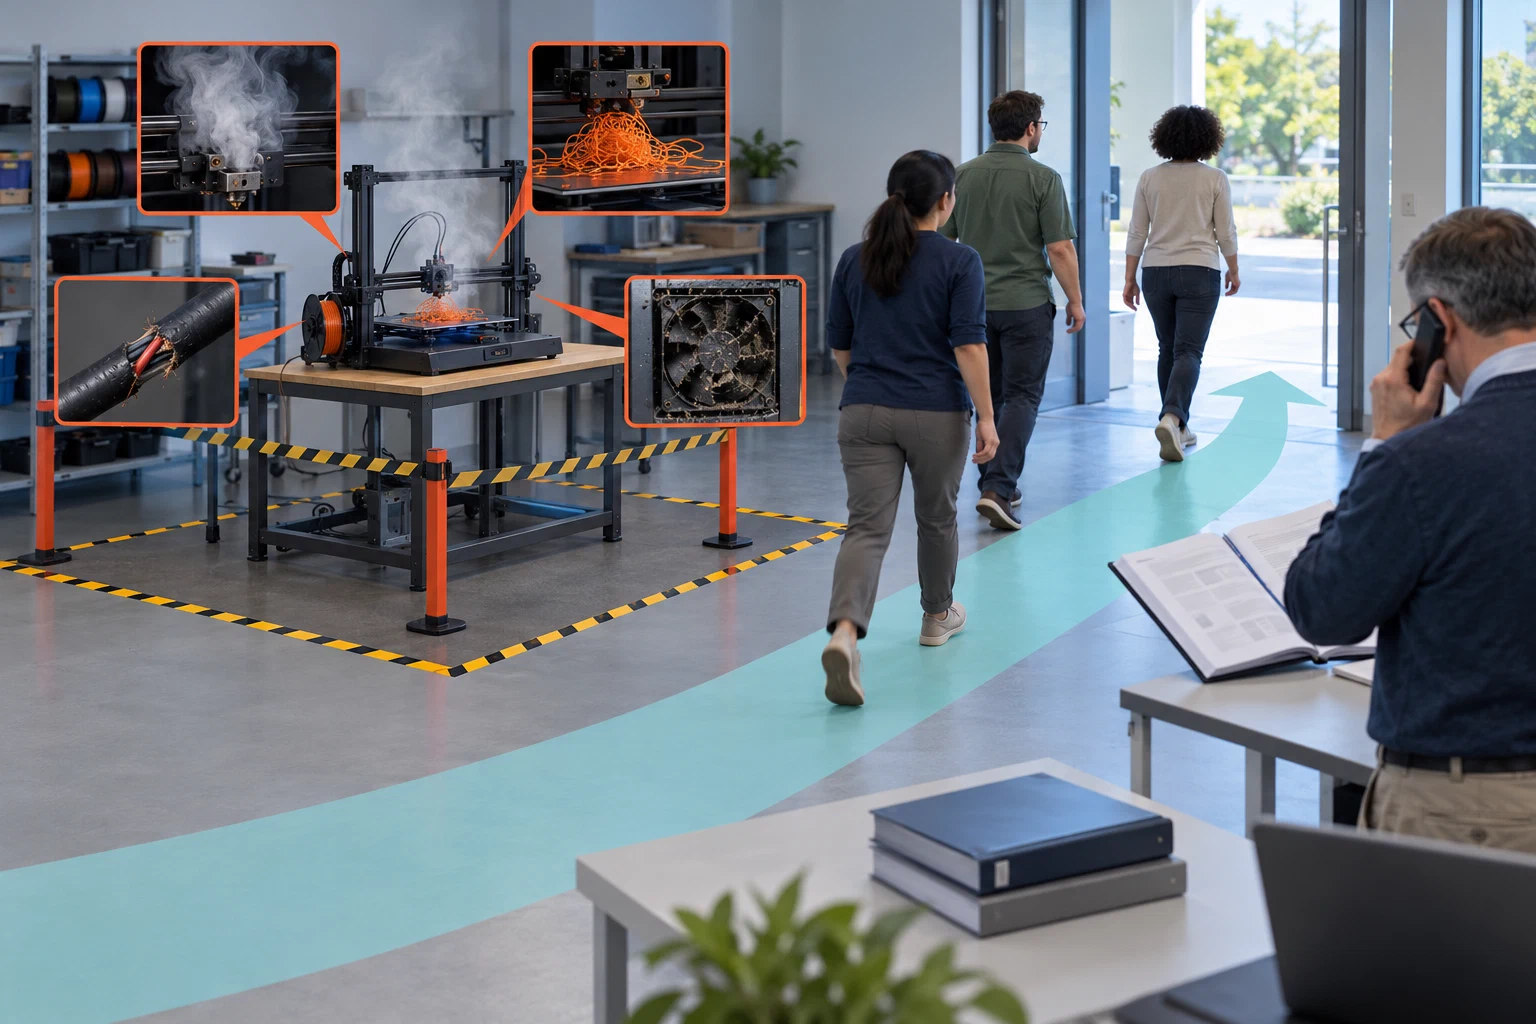
Exact print settings belong in materials and filament care and the printer/material/process preset workflow. If a product, printer, nozzle, plate, or workspace combination is undocumented, treat that as an unresolved setup question, not as permission to test. Confirm the exact manufacturer instructions and address local requirements and suitable controls for the actual material, process, and room before operating it. If those conditions remain unknown, defer that setup and seek guidance from the manufacturer or a qualified local assessor. An empty room and a stop path alone do not establish safe conditions.
Filament instructions do not automatically cover a separate sanding, cutting, coating, adhesive, or heat-treatment task. Review the actual tool and finishing product with workshop controls for finishing FFF parts .
Back to top ↑