A layer shift is a visible change in the object’s intended position, often as a staircase or offset on one axis. Ringing or ghosting is a repeated surface echo near a sharp feature. VFA-like patterns, poor geometry, a collision, a homing fault, and an extrusion problem can be mistaken for one another. Identify the artifact and where it begins before changing acceleration, belt tension, or a slicer value.
Record the event
Capture the printer and exact variant, firmware or controller, motion mode, model and orientation, material and nozzle, plate, slicer and version, selected printer and process profiles, layer height, speed, acceleration or motion limits, cooling, and any recent belt, gantry, fan, nozzle, firmware, or calibration change. Photograph the whole object and mark the first layer where the position or surface pattern changes. Record whether the defect repeats at the same model feature, follows an axis, appears after a collision, or occurs only with one generated file.
| Pattern | First distinction to make |
|---|---|
| One axis suddenly offsets and stays offset | Treat it as a possible layer shift. Identify X or Y, then check the exact model’s obstruction, belt, pulley, carriage, and collision guidance. |
| Repeating echoes beside sharp edges | Treat it as a ringing or motion-response symptom. It does not prove that one acceleration, resonance, or belt value is wrong. |
| Fine repeating bands that follow direction or speed | Consider VFA-like behavior, toolpath direction, mechanical state, and machine-specific motion behavior before applying a generic tuning value. |
| Failed homing, grinding, or unexpected travel | Stop and treat it as a motion or safety condition, not as a surface-finish adjustment. |
| A defect that follows the same model edge or starts in the preview | Compare geometry and generated toolpath before attributing it to hardware. |
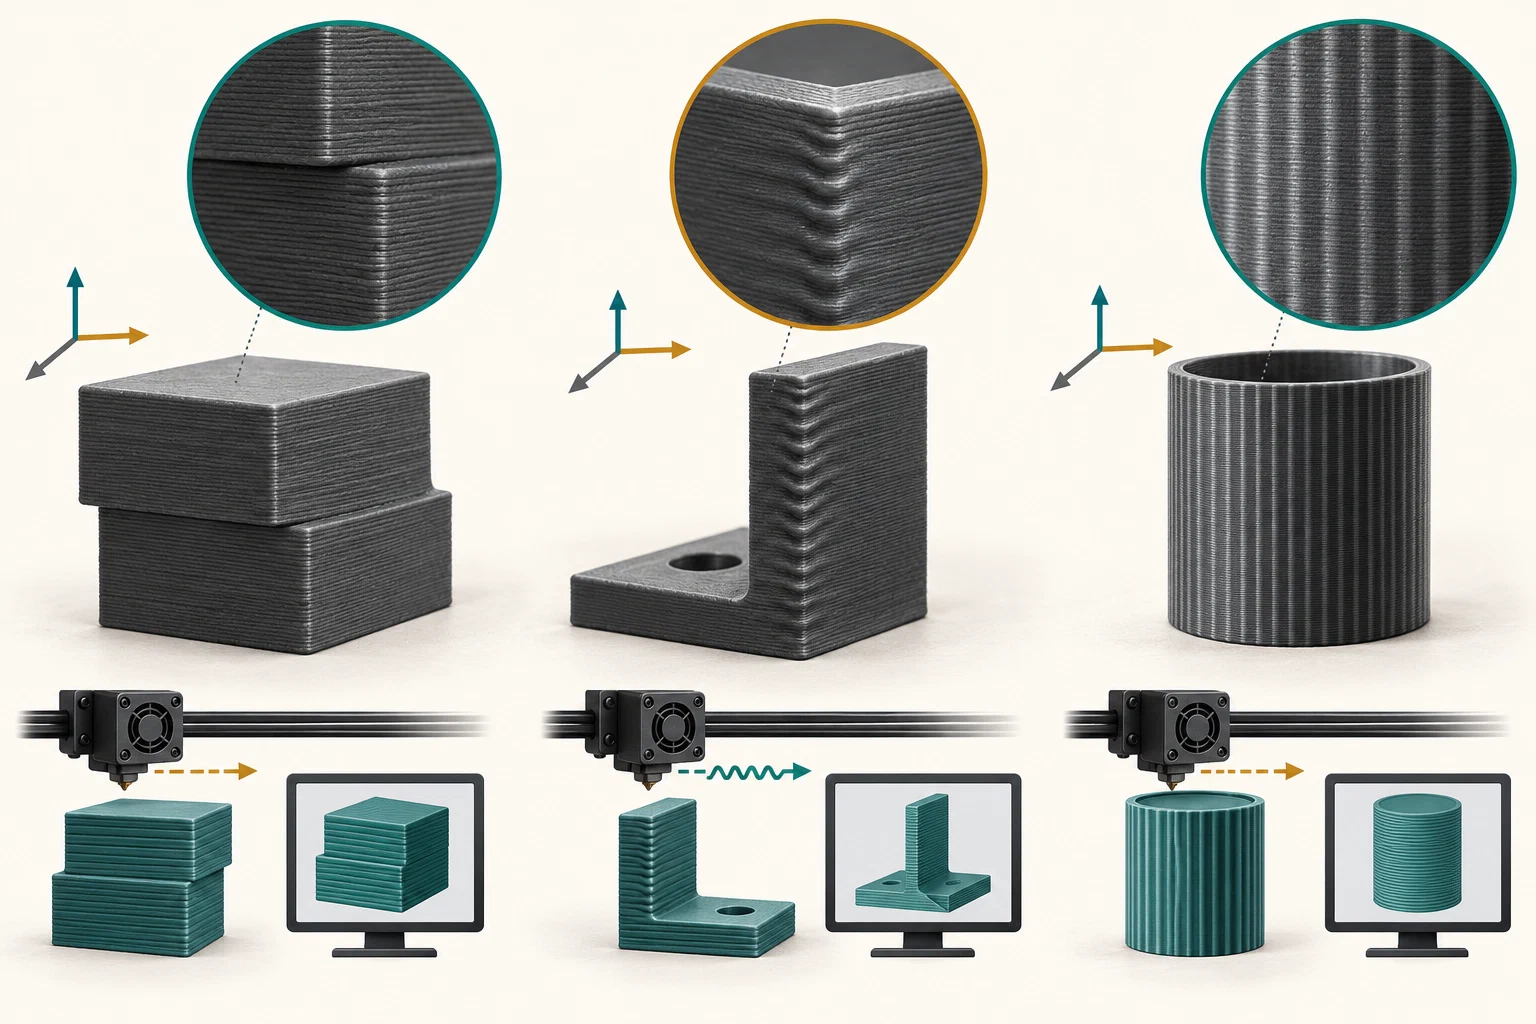
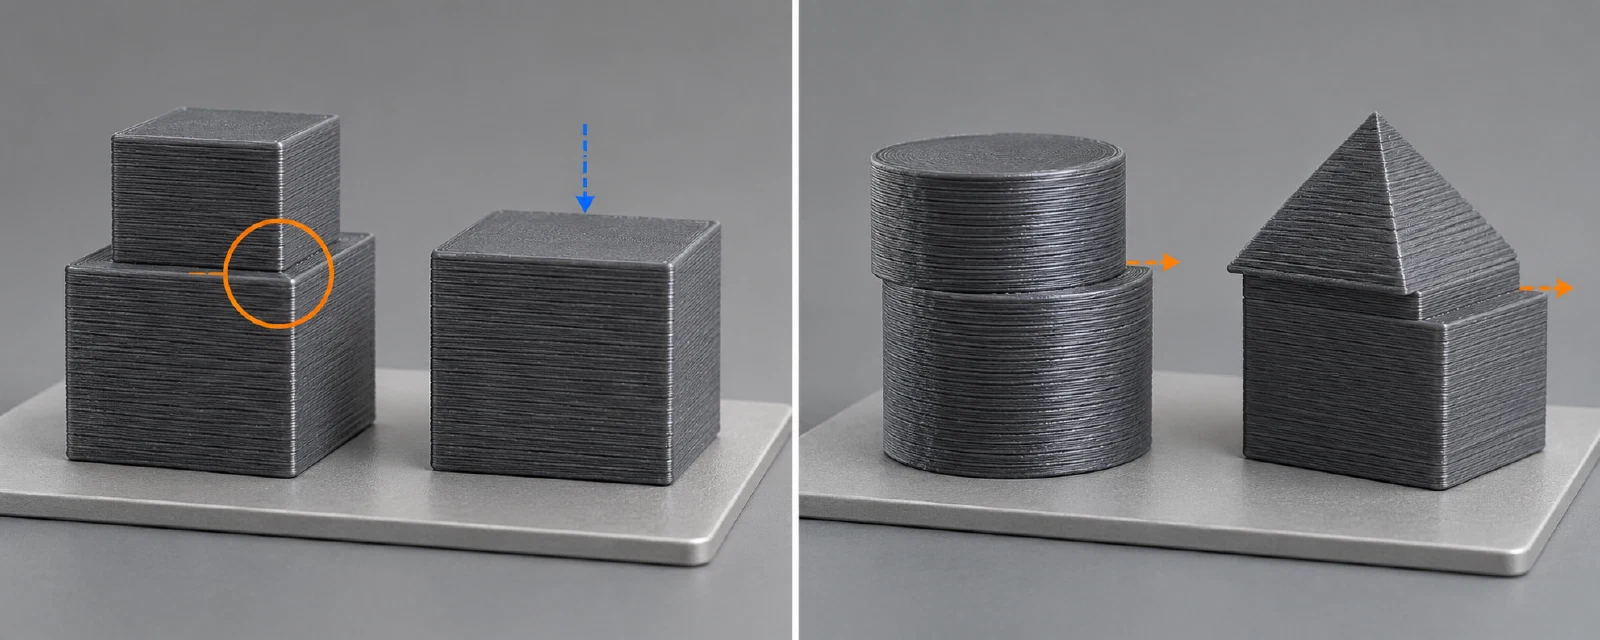
Check the job before touching hardware
Open the sliced file in the slicer’s preview and inspect the affected layers, walls, travel moves, supports, and any custom start or layer code. Confirm the selected printer, nozzle, material, process profile, firmware assumptions, and model orientation. If only one file fails, generate a controlled variant or a small diagnostic model rather than changing the machine first. A preview check can expose an intentional or accidental toolpath behavior, but a clean preview does not certify the physical printer.
For Klipper or another configurable controller, use the current documentation and the actual machine configuration to understand the relevant motion settings. Do not copy commands, acceleration limits, input-shaping results, or motor parameters between printer families. A configured value explains what the controller was asked to do; it does not prove that the mechanics can do it reliably.
Separate feature-local lines from motion-wide symptoms
One or two lines around the deck of a Benchy can match Prusa’s documented hull-line transition, where the toolpath changes from sparse infill to solid top layers; that isolated pattern does not by itself confirm a mechanical defect. Broad unevenness or a shifted layer is a different observation. Anycubic’s regular Z-axis line guide describes candidate causes for the Kobra X only, so record line spacing and the exact machine before using that branch. Also keep visible ringing separate from calibration faults: Prusa’s precise-homing refinement error and accelerometer-communication error are reported machine states with their own model-specific guidance, not proof that either caused a surface pattern. Match exact codes in printer fault codes and safety stops ; route a failed bridge or support to unsupported-feature diagnosis .
Inspect in the model’s service boundary
If the printer is safe and cool enough for the exact procedure, check for a loose object, cable or fan interference, debris, a carriage obstruction, belt damage, pulley security, gantry alignment, and other conditions named by the manufacturer. Prusa’s layer-shifting guidance starts by identifying the shifted axis and treats belt and pulley checks as family-specific diagnostics. Other printers may use different tensioning, rails, sensors, drive geometry, or service limits. Do not measure or tighten by a universal frequency, torque, or feel.
Stop for a crash, uncontrolled motion, grinding, damaged wiring, a hot or obstructed motor, repeated homing failure, or any adjustment not covered by the exact service documentation. A printer-reported error, a successful homing cycle, or a passed self-test is a diagnostic checkpoint, not proof that the underlying cause is repaired.
Change one variable and verify
After correcting a confirmed setup or mechanical issue, repeat the same small test with the same material, nozzle, plate, and profile. If no physical fault is found, change one warranted process variable within the printer and controller documentation, record the before-and-after result, and avoid changing speed, acceleration, input shaping, belts, and slicer settings simultaneously. Compare the defect’s location, severity, and repeatability, not just whether the latest object looks better.
Accept the result only after a controlled repeat and, for a meaningful production part, a second geometry that exercises the suspected motion. 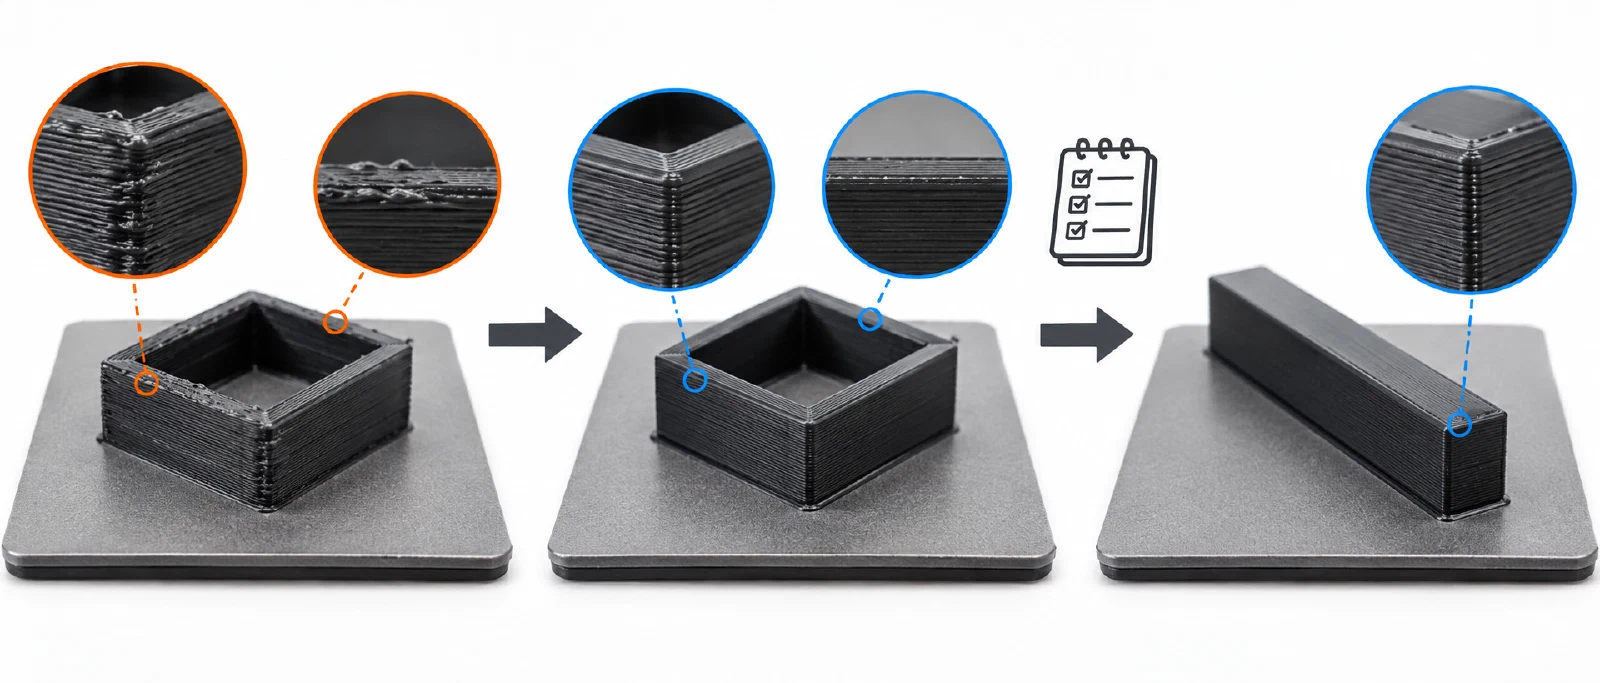
If layer shifts persist, preserve the failed object, generated file, machine configuration, and event timing for maintenance or manufacturer support. Route a true first-layer or extrusion symptom to first-layer diagnosis or under-extrusion diagnosis instead of forcing every motion artifact into one repair path.
Back to top ↑